Choosing the right object space telecentric len begins with the measurement problem, not the catalog page. In factory vision systems, a small metal washer may appear under a ring light, while a glass component sits beneath coaxial illumination. The lens must preserve scale, edge sharpness, and working distance across that real scene. Otherwise, a precise camera can still produce unreliable dimensions.
Optical designer and educator Dr. John E. Greivenkamp has described telecentric imaging as a method for reducing magnification changes caused by object movement. That principle guides this review. It also exposes a common mistake: treating every telecentric lens as interchangeable. They are not. A bi-telecentric design may stabilize both object and image space, while a fixed-magnification lens may prioritize repeatable inspection at one working distance. A liquid-lens telecentric system may offer adjustment, but it can introduce compromises in speed, resolution, and calibration.
The ten types below are organized around practical use, optical behavior, and integration demands. Expect examples involving machine vision, dimensional inspection, semiconductor alignment, and laboratory imaging. Some categories overlap. That is useful, but also confusing.
The overlooked detail is illumination. A telecentric lens cannot rescue poor lighting, reflective surfaces, or unstable fixturing. In practice, experienced engineers test the complete system: lens, sensor, light source, target, and software. Even then, the “best” design may be only the least problematic option. That is worth remembering before purchasing based on magnification alone.
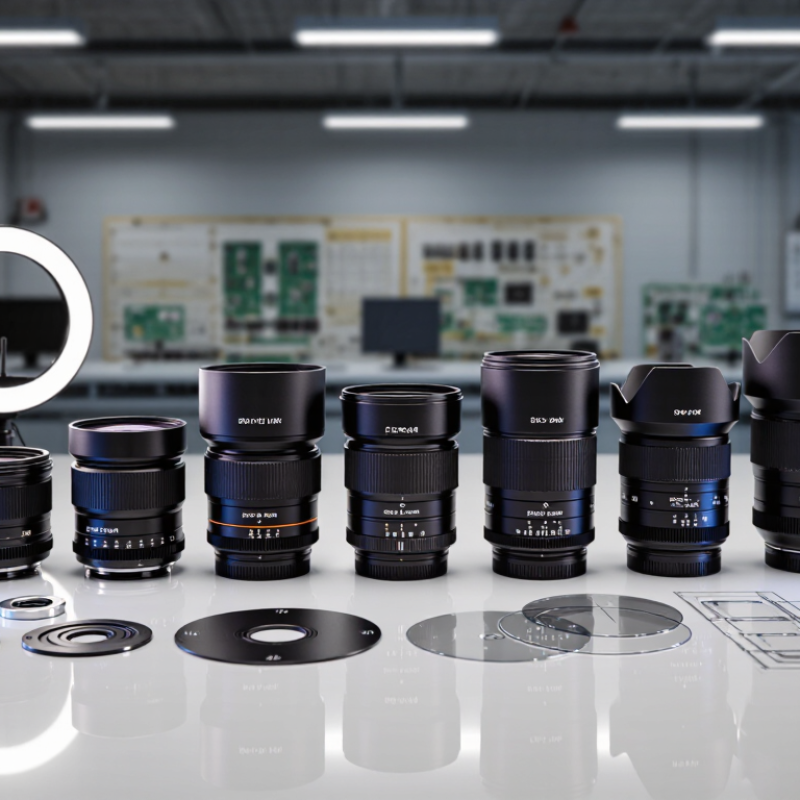
Object-space telecentric lenses are optical systems that keep chief rays nearly parallel in object space. In practical terms, a part can move slightly toward the lens without changing its measured width dramatically. This helps inspect holes, edges, shafts, and molded components with stable dimensions. Standard lenses often make nearby features appear larger. Telecentric designs reduce that perspective error.
Their structure usually includes an aperture stop near the front focal point, multiple lens groups, and a controlled imaging path. The stop limits chief-ray angles before light reaches the sensor. Parallel object-side rays then create consistent magnification across the inspection field. A real setup still depends on focus, sensor size, working distance, and illumination.
Poor lighting can hide the advantage. I have seen clean optics produce unreliable measurements when a metal edge reflects unevenly.
The design is precise, but not magical.
Tips: Match the lens to the required field of view and working distance, not only sensor resolution. Use diffuse lighting for shiny surfaces, and check calibration with a certified reference target. Keep the part centered when possible. Small alignment errors can become visible at high magnification. Test several sample heights before approving the system. This step is easy to skip, and regrettable.
object space telecentric lenses help preserve measurement accuracy when object distance changes slightly. Fixed-magnification designs keep the image scale stable across a defined working range. They suit gauging parts, checking connector pins, and inspecting molded edges. In production testing, a stable 0.5× view can reduce calibration drift. However, the working distance remains limited. Small setup errors may still affect sharpness.
Bi-telecentric lenses keep chief rays nearly parallel on both object and image sides. This reduces perspective errors and supports precise dimensional inspection. They are useful for flat components, machined profiles, and transparent samples. Large-aperture designs collect more light, which helps reveal dark surfaces or fine scratches. Yet, a wider aperture can reduce depth of field. I have seen an apparently brighter image hide focus variation across a thick part. No lens is perfect. Mechanical alignment still matters.
Tips: Match magnification to the smallest feature, not the entire part. Check working distance with the real fixture installed. Test depth of field using samples with different heights. For large apertures, control lighting carefully to avoid glare. Record calibration results at several object positions. This step often exposes assumptions that looked reasonable on paper.
| Lens Type | Operating Principle | Typical Magnification Behavior | Object-Side Telecentricity | Key Optical Characteristics | Typical Strengths | Main Limitations | Common Applications |
|---|---|---|---|---|---|---|---|
| 1. Fixed-Magnification Object-Space Telecentric Lens | The entrance pupil is positioned near infinity on the object side, making chief rays approximately parallel to the optical axis. The lens is optimized for one nominal magnification rather than continuous zooming. | Very stable around the specified working distance and nominal magnification. It is not intended to provide a broad zoom range. | High. Perspective distortion and magnification changes caused by moderate object-height variation are strongly reduced. | Usually designed for a fixed working distance, fixed image circle, and a defined sensor format. The usable depth range depends on numerical aperture and acceptable measurement error. | Repeatable dimensional inspection, low perspective error, and straightforward calibration in automated vision systems. | Limited flexibility if the working distance, sensor size, or required magnification changes. Telecentric optics can also be physically longer than ordinary imaging lenses. | Part gauging, edge measurement, semiconductor inspection, dimensional verification, and high-repeatability machine vision. |
| 2. Bi-Telecentric Lens | Telecentricity is provided in both object space and image space. Chief rays are approximately parallel to the optical axis on both sides of the optical system. | Extremely stable against small changes in object distance and image-side positioning when the system is used near its design conditions. | High. Object-side perspective effects are minimized, supporting accurate measurements of object dimensions and relative positions. | Designed to maintain nearly constant magnification while also reducing sensitivity to detector defocus or image-plane displacement. Often uses a comparatively complex multi-element optical layout. | High measurement consistency, low perspective error, and improved tolerance to small setup variations on both sides of the lens. | Typically larger, heavier, and more expensive than a comparable single-sided telecentric lens. Light transmission may be lower because of the additional optical elements and apertures. | Precision metrology, dimensional inspection, tolerance verification, flatness checks, connector inspection, and applications requiring stable scale reproduction. |
| 3. Large-Aperture Object-Space Telecentric Lens | Combines object-space telecentric geometry with a relatively large entrance pupil or clear aperture to collect more light and support higher optical throughput. | Magnification remains substantially less sensitive to object-depth changes than with a conventional non-telecentric lens, provided the object remains within the designed telecentric field. | High, subject to the specified telecentricity error and working range of the design. | Large aperture can provide higher numerical aperture, brighter images, and potentially higher resolving power. It may also reduce depth of field at a given magnification. | Useful for fast imaging, low-light inspection, high-speed line operation, and resolving fine features when illumination and sensor performance are sufficient. | Greater sensitivity to focus, alignment, aberrations, and illumination uniformity. The lens may be larger and more costly, and the reduced depth of field can complicate inspection of uneven parts. | High-speed production inspection, low-light measurement, fine-feature imaging, scientific imaging, and inspection of components with demanding resolution requirements. |
Coaxial telecentric lenses send illumination along the optical axis through a beam splitter. This design reduces shadows inside holes, grooves, and recessed features. It works well with polished metal parts and printed circuit surfaces. Broadband telecentric lenses maintain stable magnification across a wide wavelength range. They support color cameras and mixed lighting conditions. However, “broadband” does not guarantee perfect color correction. Testing remains essential.
Tips: Match the lens to the light source, sensor size, and target surface. Check the working distance before installation. A small mismatch can reduce measurement reliability.
Infrared telecentric lenses are useful when visible light creates glare or low contrast. They can reveal heat-related patterns, coated surfaces, and material differences. Confirm the lens transmission range before selecting an infrared camera.
Long-working-distance designs protect the lens from moving stages, heat, dust, and tall components. They also simplify access to narrow inspection areas. The trade-off may include a larger housing or reduced numerical aperture. In practice, I have seen teams choose distance first and image quality later. That decision often needs reconsideration. Test the complete optical setup with real parts, not only sample charts.
Compact object space telecentric lenses fit machines where space is limited. Their shorter mechanical length helps engineers place cameras near moving stages. They preserve nearly constant magnification across moderate depth changes. This reduces measurement errors on small parts. However, compact housing can limit aperture size and working distance. The result may be less light than expected. In practice, I would test illumination before approving the lens.
High-resolution designs reveal fine edges, surface scratches, and narrow gaps. They typically use carefully corrected optics and stable mechanical assemblies. A large sensor alone does not guarantee useful detail. Pixel size, numerical aperture, lighting, and vibration also matter.
Type Ten: application-specific lenses are built around a defined task. Examples include connector inspection, printed pattern measurement, or semiconductor component alignment. These lenses may include special working distances, spectral ranges, or distortion control. They can perform extremely well, but flexibility is often reduced.
Measure the part, not only the camera. Record working distance, field of view, object depth, and tolerance requirements. Use a calibrated target during acceptance testing. Check edge sharpness across the entire image. Do not trust a center-only result. A prototype may expose unexpected reflections, heat drift, or mounting weakness. That feedback is useful, even when the original design seemed correct.
Choosing an object-space telecentric lens starts with the measurement, not the lens catalog. Its chief advantage is stable magnification when object distance changes slightly. This matters when checking machined edges, molded parts, or small gaps. Common types include fixed-magnification lenses, bi-telecentric designs, and versions with coaxial illumination. Each suits a different inspection problem.
Compare the required field of view with the camera sensor size. A larger field may reduce detail. Check working distance carefully, especially around tall parts or moving fixtures. Low distortion is essential for dimensional measurement, while a smaller aperture can increase depth of field. However, stopping down too far may reduce brightness and expose sensor noise. That trade-off is often underestimated. Review the lens’s numerical aperture, telecentric angle, spectral range, and maximum usable sensor format. Then test a real sample, not only a flat calibration target. Edges, reflective surfaces, and curved features can reveal problems quickly.
Tips: Hold the part at several depths and measure the same feature each time. Record magnification drift, edge sharpness, and illumination uniformity. Use certified references when accuracy matters. Leave clearance for lighting and fixtures. A lens that looks perfect on paper may fail beside a metal bracket or deep cavity. Recheck alignment after installation; even a small tilt can create misleading dimensional results. In uncertain cases, a slightly lower magnification may provide more reliable coverage and fewer rejected images.
Comparative suitability scores for common inspection requirements. Higher scores indicate stronger suitability; actual performance depends on magnification, sensor size, working distance, illumination, and spectral range.
Bi-telecentric designs provide the highest dimensional stability because they are telecentric on both object and image sides. Coaxial and large-format designs are well suited to reflective surfaces and larger fields of view, while UV, SWIR, and liquid-tunable designs should be selected when wavelength or rapid focus adjustment is the primary requirement.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru