Choosing among China’s top 10 Rubber Deflashing Machine manufacturers is not just a price comparison. It is a process decision. A machine that works well for thick molded seals may struggle with thin, delicate components. Part geometry, rubber hardness, batch size, and acceptable surface finish all matter.
Rubber technologist John S. Dick’s published work offers a useful perspective. Editorial paraphrase, not a verified direct quotation: “Consistent results depend on controlling materials, process conditions, and inspection.” That distinction matters. No single machine suits every compound or part. Ask suppliers how they handle your actual components, not only standard samples. Request a trial using representative parts, then inspect edges under consistent lighting. Check cycle time, media or tooling requirements, operator workload, and maintenance access. Small details count. A hard-to-clean chamber can slow a busy shift. Unclear service arrangements can matter later.
This guide compares manufacturers through practical criteria: machine type, customization, production capacity, control features, quality documentation, and after-sales support. It also considers whether a supplier explains limitations plainly. That is not always easy to judge from a catalog. Treat rankings as a starting point, not a guarantee of fit. Before ordering, confirm specifications in writing and test the process against your own quality requirements. A careful comparison can reduce surprises, though it cannot replace a real production trial.
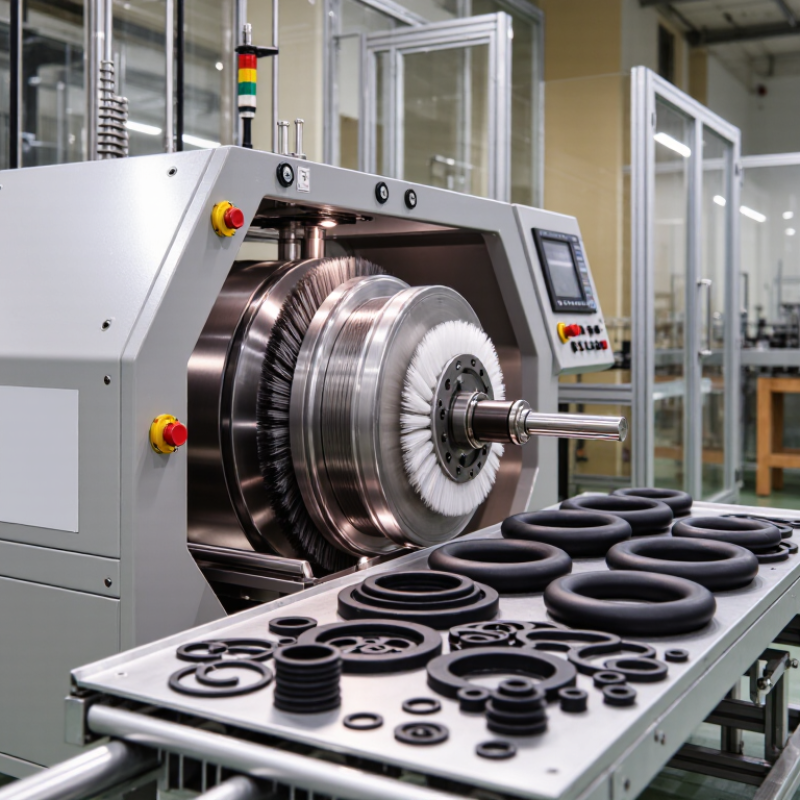
Rubber deflashing machines remove thin fins of excess material left along a molded part’s seam. These edges may look minor, but they can interfere with assembly, sealing, or a product’s fit. Depending on the rubber compound and part geometry, plants use methods such as mechanical trimming or cryogenic deflashing. The right choice depends on the part, not just the machine.
The industrial scale is substantial. The International Rubber Study Group’s World Rubber Industry Outlook 2024 estimated global rubber demand at roughly 30 million tonnes in 2023. Even small trimming inefficiencies can therefore matter across high-volume production. A well-set machine can reduce repetitive handwork and produce more consistent edges. Operators still need to check parts closely. Thin walls and tight corners can be damaged by excessive force or an unsuitable cycle.
A practical setup starts with a representative batch, not a catalogue promise. Technicians check flash thickness, part temperature, media, and cycle time, then inspect edges under good lighting. That detail matters. Deflashing is not magic; results vary with compound, mold condition, and part design. Some facilities also track rejected parts and rework, though the figures can be imperfect when teams record defects differently.
The entries below describe ten common equipment specializations relevant to rubber deflashing. They are capability categories, not a ranked list of named manufacturers; actual machine specifications vary by supplier and application.
| No. | Equipment Specialization | Deflashing Method | Typical Parts and Materials | Industrial Role | Key Selection Consideration |
|---|---|---|---|---|---|
| 1 | Cryogenic batch systems | Parts are cooled, commonly with liquid nitrogen, so thin flash becomes brittle; tumbling or blasting then removes it. | Small-to-medium molded rubber parts, including seals, gaskets, and grommets. | Processes multiple parts in a batch while limiting manual trimming. | Confirm material response to low temperature, batch size, and the required surface finish. |
| 2 | Cryogenic continuous systems | Conveyor-fed parts pass through a controlled cryogenic cooling and deflashing process. | Parts produced in regular, repeatable production runs. | Supports higher-throughput operations with reduced batch handling. | Check line speed, part orientation, loading method, and compatibility with upstream and downstream equipment. |
| 3 | Rotary tumbling machines | Parts move against one another or against approved media in a rotating chamber to wear away flash. | Durable parts with shapes that can tolerate controlled part-to-part contact. | Offers a relatively simple mechanical route for bulk processing. | Evaluate the risk of part-to-part damage, media contamination, and uneven treatment of complex shapes. |
| 4 | Centrifugal finishing systems | Rotating barrels or chambers generate higher-energy movement than conventional low-speed tumbling. | Small, robust components that need consistent finishing in a contained process. | Can shorten processing cycles for suitable parts compared with gentler tumbling methods. | Validate that the force and contact pattern will not deform or mark the parts. |
| 5 | Abrasive or media-blasting systems | A controlled stream of suitable media strikes exposed flash and removes it from the part. | Parts with accessible flash lines and surfaces that can withstand the selected media. | Provides targeted removal and can be configured for manual or automated operation. | Match media type, impact energy, nozzle access, and dust collection to the compound and part geometry. |
| 6 | Automated trimming and robotic cells | Robots, fixtures, or programmed tools guide cutting or trimming along defined parting lines. | Parts requiring repeatable treatment of specific gates, edges, or flash locations. | Reduces repetitive manual work and supports consistent processing when parts can be located reliably. | Assess fixture design, tool access, cycle time, and the ability to accommodate part variation. |
| 7 | Seal and gasket processing systems | Deflashing is selected according to seal geometry, compound, and allowable edge condition; cryogenic and mechanical approaches are both used. | O-rings, molded seals, gaskets, and related elastomer components. | Removes excess flash that may affect assembly, appearance, or sealing performance. | Define acceptable edge quality and inspect critical sealing surfaces after processing. |
| 8 | Injection-molded rubber part systems | Batch or automated processes remove flash formed around mold parting lines and other exposed edges. | Injection-molded elastomer components with repeatable geometry. | Complements molding operations by preparing parts for inspection, assembly, or packing. | Consider mold condition, flash thickness, part geometry, and the production rate required. |
| 9 | Precision small-part systems | Controlled low-impact processing or carefully fixtured trimming targets fine flash on small components. | Small molded parts where dimensional consistency and surface condition are important. | Helps process components that may be difficult or slow to finish manually. | Test samples for dimensional change, residual flash, cleanliness, and part loss during handling. |
| 10 | Integrated custom production lines | Deflashing equipment is combined with part feeding, separation, inspection, or material handling. | Applications with defined process requirements and a stable production workflow. | Links finishing with adjacent operations to reduce manual transfer and improve process traceability. | Review controls, safety systems, changeover needs, maintenance access, and integration requirements. |
Choosing among China’s rubber deflashing machine manufacturers starts with the part, not the catalog. Share details such as rubber type, part dimensions, flash thickness, and target output. A capable supplier should explain how its process suits those conditions, rather than promise one machine fits every job. Request a trial using representative parts. Check whether edges are clean without damage to the sealing surface. Run it twice. Small differences between batches can reveal inconsistent settings or loading. Details matter.
Review the machine’s working range, cycle time, tooling needs, and changeover steps. Ask how operators adjust temperature, pressure, or other process settings, where applicable. Inspect photos or videos of the actual work area, guarding, controls, and maintenance access.
A clear inspection record is more useful than a broad quality claim. Confirm what training, spare parts, and technical support are available after installation, and ask for realistic response times. Compare written specifications against the trial results, not just quoted output figures.
Even a successful sample test may not represent a full production shift. A longer pilot run can expose heat buildup, wear, or operator delays, so the evaluation should leave room for revision.
China’s rubber deflashing machine manufacturers vary in focus, from compact batch systems to automated cryogenic lines. A useful profile of ten leading suppliers should compare more than catalogue claims. It should examine machine capacity, part-size range, cycle time, tooling access, maintenance support, and documented test results. Small details matter: Can operators reach the loading area safely? Are spare blades and seals readily available? A polished brochure cannot answer every shop-floor question.
The International Rubber Study Group’s October 2023 outlook projected global rubber demand at about 30.9 million tonnes in 2024. That scale of demand makes consistent finishing and production uptime important across rubber goods manufacturing. Still, market growth alone does not prove a machine will suit a specific plant. Buyers should request sample runs using their own parts, then inspect edges, surface marks, and material loss. Results can differ by compound and geometry.
The ten profiles can group Chinese manufacturers by practical strengths: cryogenic deflashing, mechanical trimming, automation, custom tooling, or service coverage. Compare energy use per batch, noise, guarding, and changeover time where suppliers provide measured data. Ask how performance was tested. One limitation remains: public specifications may omit real operating conditions, so direct verification is sensible. Even a small burr can matter.
Comparing Technologies, Production Capabilities, and Services
When comparing Chinese suppliers, match the process to the part, not the brochure. Cryogenic systems use chilled media and tumbling; mechanical trimming suits accessible edges, while manual finishing remains useful for delicate, low-volume parts. Thermal methods can process complex pieces, but material limits and edge quality need testing. Small details matter. Check flash thickness, gate position, rubber hardness, and whether parts arrive warm.
Capacity claims need context. OICA’s 2023 production statistics recorded 93.5 million motor vehicles produced worldwide, reflecting the scale of rubber-component supply chains. This figure does not prove demand for any single machine. Ask manufacturers for cycle time, batch loading, yield, and changeover data using your own parts. A quoted throughput can still mislead. Request a sample run and inspect edges under consistent lighting.
Production capability also includes controls, spare-part availability, and commissioning support. Compare PLC recipes, temperature stability, media recovery, and dust collection where relevant. Ask how technicians diagnose uneven deflashing and how quickly wear parts can ship. Service promises should specify response times and training scope. A showroom demonstration may not represent mixed batches or worn tooling. Record acceptance criteria before purchase, then verify them across several production lots.
Choosing a rubber deflashing machine manufacturer starts with your parts, not a catalog ranking. Define the rubber compound, part dimensions, flash thickness, and daily output. A machine suited to small seals may struggle with larger molded components. Small details matter. Ask manufacturers to process your actual parts or representative samples. Check flash removal, surface condition, cycle time, and reject rate after testing. Request clear operating requirements, including temperature, media, tooling, and operator involvement.
Tips: Share photos and drawings, but include physical samples when possible. Ask for a written test report. Confirm what “acceptable finish” means before comparing quotations. A polished brochure is not proof.
Before committing, review machine specifications and available service support. Ask how spare parts are supplied, how quickly technical questions are answered, and what training is included. If possible, observe a machine running a similar job. Listen for inconsistent cycles, inspect finished parts under good lighting, and ask how settings change between product runs. Compare the full production cost, not only the purchase price. Energy use, consumables, labor, and maintenance can affect the real cost. Some requirements may change after testing; that is normal, but unclear answers deserve a second look.
Compare suppliers against the production factors that matter for your parts and process.
The 1–5 scores are a suggested screening guide, not measured market data or ratings of individual manufacturers. Prioritize material and part geometry first, then confirm throughput, flash thickness, automation, and consumable requirements with sample trials and production specifications.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru