China’s manufacturing base is turning inspection into a measurable production capability. According to the International Federation of Robotics’ World Robotics 2024 report, Chinese factories installed 276,288 industrial robots in 2023, representing about 51% of global installations. This scale creates strong demand for Automated Visual Inspection Systems that can check surfaces, dimensions, labels, solder joints, and assembly accuracy without slowing the line.
The opportunity is substantial, but supplier quality varies. MarketsandMarkets estimates that the global machine vision market will grow from approximately USD 15.7 billion in 2024 to USD 20.0 billion by 2029. Its forecast highlights the importance of cameras, optics, lighting, software, and artificial intelligence. A system may appear impressive in a demonstration, yet fail under dust, vibration, reflective metal, or changing product colors. That gap matters.
Jeff Burnstein, president of the Association for Advancing Automation, has described machine vision as “the eyes of automation.” The phrase is simple. The engineering is not. Reliable Chinese suppliers must prove repeatability through sample testing, false-rejection analysis, traceable data, and stable after-sales support. Buyers should also examine integration experience, not only hardware specifications or quoted prices.
This guide reviews leading China-based Automated Visual Inspection Systems suppliers through practical criteria, including detection accuracy, line compatibility, software flexibility, service coverage, and industry experience. Some evaluations remain imperfect because published performance figures are not always independently verified. That limitation deserves attention, especially before a factory commits to large-scale deployment.
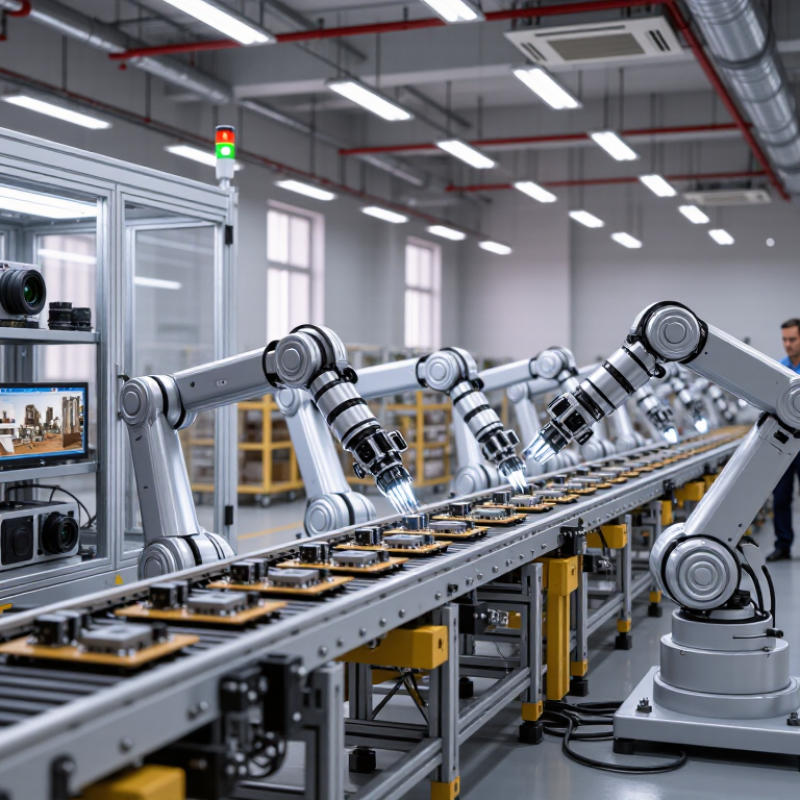
Automated visual inspection systems use cameras, lighting, software, and sensors to examine products during manufacturing. They identify defects that may escape tired human eyes, including scratches, missing parts, uneven edges, and incorrect labels. The system compares each image with defined quality standards and records inspection results.
In practice, a camera captures each product as it moves along a conveyor. Controlled lighting reveals surface marks, while software measures size, position, color, and shape. A reliable system can separate acceptable products from defective ones within milliseconds. It also creates traceable data for process analysis and quality audits. China’s experienced suppliers often customize these systems for electronics, packaging, automotive components, and precision hardware.
Accuracy depends on more than advanced software. Lens selection, lighting angles, product fixtures, and calibration all matter. Engineers should test real samples, including difficult defects and normal variations, before approving deployment. False alarms can slow production. Missed defects can damage customer trust. The system is not magic.
Some inspections remain difficult when surfaces reflect light or products change position. Regular calibration and human review are still necessary. A practical team should question poor results rather than hide them. In my experience, the strongest system is not always the most complex. It is the one that performs consistently under real factory conditions.

China’s automated visual inspection systems increasingly combine high-speed cameras, structured lighting, and edge computing. MarketsandMarkets estimated the global machine vision market at about USD 12.3 billion in 2023. It also projected growth to nearly USD 20.2 billion by 2028. This expansion supports stronger investment in Chinese inspection engineering.
Line-scan cameras inspect continuous materials, including film, glass, and metal surfaces. Area-scan cameras handle packaged products and assembled parts. Three-dimensional cameras measure height, depth, and surface deformation. Deep-learning models classify irregular defects that fixed rules often miss.
Industrial PCs process images locally, reducing network delays. Interfaces with PLC and MES platforms also improve traceability. China’s strength is practical integration. Components are often adapted to local production speeds and factory layouts.
The weak point is model reliability. Poor lighting or limited defect samples can produce false alarms. That problem remains easy to underestimate. The International Federation of Robotics reported 276,288 industrial robot installations in China during 2023, representing 51% of global installations. This automation base helps inspection deployment, but inspection accuracy still requires disciplined validation.
Tips: Test reflective and dark surfaces separately. Record false positives, not only missed defects. Use independent samples from different shifts. Review model results with experienced operators. A technically impressive system can still fail in changing factory conditions.
Leading suppliers of automated visual inspection systems in China serve electronics, automotive, packaging, medical devices, and precision manufacturing. Their systems commonly combine industrial cameras, controlled lighting, image-processing software, and robotic handling. A strong supplier should explain detection limits clearly. It should also provide sample testing with real production parts.
Experienced buyers often inspect the supplier’s engineering process, not only the machine’s appearance. Ask for repeatability data, false-rejection rates, cycle-time records, and maintenance procedures. A practical supplier can adjust lighting for reflective metal, transparent film, or uneven surfaces. It should also support integration with conveyors, programmable controllers, factory networks, and existing quality systems.
Local technical support matters. Response time can affect production more than the purchase price. Reliable suppliers usually offer installation guidance, operator training, spare parts planning, and software updates. Yet no inspection system is flawless. Dust, vibration, changing materials, and poor sample preparation may reduce accuracy. That assumption can fail. Buyers should request a trial run under real factory conditions and document every result. Clear acceptance criteria make supplier comparisons more credible and reduce costly misunderstandings.
| Supplier Profile | Primary Inspection Applications | Supported Inspection Technologies | Typical Camera Configuration | Typical Resolution Range | Production Line Compatibility | Common Defect Categories | Integration Features | Relevant Quality Standards |
|---|---|---|---|---|---|---|---|---|
| Supplier Profile A | Automotive components, metal parts, precision-machined products | 2D vision 3D measurement Pattern matching | Area-scan cameras with optional line-scan modules | 2–25 megapixels, depending on field of view and inspection tolerance | Inline inspection for conveyor, rotary-indexing, and robotic handling systems | Missing parts, dimensional variation, surface scratches, burrs, incorrect assembly | PLC communication, industrial Ethernet, digital I/O, recipe management, statistical data export | ISO 9001 quality-management framework; CE requirements where applicable |
| Supplier Profile B | Electronics, PCB assemblies, connectors, semiconductor-related components | AOI OCR/OCV Barcode reading | High-speed monochrome or color area-scan cameras | 5–25 megapixels for component presence, placement, marking, and solder-joint inspection | SMT, assembly, testing, and packaging lines | Wrong component, polarity error, insufficient solder, bridging, misplaced marking, contamination | MES connectivity, traceability records, barcode interfaces, remote diagnostics, configurable inspection recipes | ISO 9001; ESD-control practices are commonly required for electronics production |
| Supplier Profile C | Plastic injection-molded parts, household products, consumer goods | Color inspection Shape analysis Deep learning | Color area-scan cameras with diffuse, coaxial, or dome lighting | 2–12 megapixels for appearance and dimensional checks | Conveyor-based lines, pick-and-place cells, and automatic sorting equipment | Short shot, flash, deformation, color inconsistency, contamination, surface marks | Robot interfaces, reject actuators, batch statistics, user-access control, alarm management | ISO 9001; product-specific regulatory requirements may apply to food-contact or medical applications |
| Supplier Profile D | Pharmaceutical packaging, medical disposables, laboratory consumables | Print verification Seal inspection Presence/absence checks | High-resolution monochrome or color cameras with controlled illumination | 2–20 megapixels, selected according to package size and required defect sensitivity | Continuous web, blister, pouch, bottle, and carton packaging lines | Missing label, unreadable code, damaged seal, incorrect fill level, foreign material, packaging damage | Electronic records, audit trails, user permissions, batch reporting, reject confirmation | ISO 9001; regulated projects may require GMP, 21 CFR Part 11, or sector-specific validation |
| Supplier Profile E | Food and beverage packaging, bottles, caps, labels, cartons | Line-scan vision OCR/OCV Foreign-object detection | Line-scan cameras for continuous materials and high-speed web inspection | 4k–16k pixels per line for web, label, film, and surface inspection | High-speed conveyors, filling lines, labeling machines, and packaging equipment | Label defects, print errors, cap damage, seal defects, missing products, film contamination | Encoder synchronization, PLC and SCADA communication, automatic rejection, production reporting | ISO 9001; HACCP and food-safety requirements may apply to the production environment |
| Supplier Profile F | Glass, film, sheet materials, textiles, batteries, and continuous-process products | Surface inspection Line-scan imaging Defect classification | Multi-camera line-scan systems with encoder-based synchronization | 2k–16k pixels per line; final performance depends on material width and line speed | Web inspection, roll-to-roll processing, extrusion, coating, and continuous production lines | Pinholes, streaks, cracks, coating variation, wrinkles, inclusions, foreign particles | Industrial Ethernet, encoder input, defect mapping, roll reports, database connectivity, remote support | ISO 9001; electrical, machinery, and workplace-safety compliance depends on installation scope |
Automated visual inspection now supports electronics, automotive parts, batteries, food packaging, and pharmaceutical containers. According to the International Federation of Robotics’ World Robotics 2024 report, manufacturers installed 541,302 industrial robots worldwide in 2023. This expansion increases demand for vision systems that inspect products beside fast-moving production lines.
Small defects matter.
In electronics, high-resolution cameras detect missing components, solder bridges, bent pins, and surface scratches. In automotive production, 3D sensors measure gaps, weld beads, and assembly position.
Food and packaging lines commonly inspect seals, labels, fill levels, and foreign particles. The inspection method must match the product. A reflective metal surface can defeat a poorly selected lighting system.
The machine vision market is also becoming more data-driven. The Association for Advancing Automation reported continued growth in vision technology adoption across manufacturing applications in recent industry updates. Effective systems combine cameras, controlled lighting, image-processing software, and traceable results. They can reject defective products within milliseconds and store images for process analysis.
However, accuracy claims require careful testing. A 99.9% detection rate may change under dust, vibration, color variation, or new product designs. Suppliers with practical integration experience should provide sample testing, false-rejection data, calibration procedures, and maintenance guidance.
Human review remains useful for unusual defects and borderline decisions. This part is often underestimated.
Selecting automated visual inspection suppliers in China requires more than comparing machine prices. Start with inspection experience in your product category. Metal parts, electronic assemblies, packaging, and glass each need different optics and software logic. Ask for measured results from similar production lines. Request defect samples, false-rejection rates, and inspection speed under real factory conditions.
Technical capability matters, but practical integration matters more. Check camera resolution, lighting stability, algorithm training, data traceability, and communication with existing equipment. A reliable supplier should explain calibration procedures and maintenance intervals clearly. Site audits can reveal wiring quality, operator access, and spare-part readiness. Also examine service coverage, response times, training plans, and documentation in English. Small details matter. A fast machine is not useful if operators cannot adjust it safely.
Market conditions can change the purchasing decision. Local component availability may reduce downtime, while export projects may require stronger documentation and remote support. Compare total ownership costs, including installation, software updates, rejected products, and future model changes. Certifications should match the destination market and application. Avoid accepting impressive laboratory demonstrations as production evidence. I have seen inspection projects fail because product samples were too clean. Real factories contain dust, vibration, uneven surfaces, and changing materials. Suppliers should test those imperfections before contract approval. Even experienced buyers can underestimate integration time, so a staged acceptance plan is worth considering.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







