Global buyers are entering a demanding Cnc Parts market. Dimensional accuracy, material traceability, delivery stability, and engineering support now matter as much as unit price. Grand View Research valued the global CNC machine market at approximately USD 83.99 billion in 2023. Its report projects a 10.3% compound annual growth rate from 2024 to 2030. This expansion reflects wider automation, aerospace demand, medical-device production, and shorter product cycles.
However, larger market numbers do not guarantee better suppliers. A factory may show polished equipment, yet provide weak inspection records or unclear tolerances. Buyers should examine ISO 9001 certification, CMM capability, first-article inspection, surface-finish control, and realistic lead times. These details become visible on the shop floor: calibrated gauges beside a machining center, sealed material certificates, and labeled batches waiting for inspection. Dr. Thomas W. Kurfess, a manufacturing engineer and former SME president, has said, “Manufacturing is the backbone of our economy.” His point remains relevant because dependable components support entire products, not isolated purchase orders.
This guide compares leading CNC parts manufacturers for international buyers. It considers machining capacity, supported materials, quality systems, communication, logistics, and customization. Deloitte’s 2024 Global Manufacturing Industry Outlook also identifies supply-chain resilience and digital transformation as continuing priorities. Still, no ranking can fit every project. A small aerospace prototype needs different support from a high-volume automotive program. Some supplier information also changes quickly. Buyers should verify certificates, sample quality, and current capacity before committing. That extra step is less exciting. It is often the difference between a smooth production run and an expensive rework cycle.
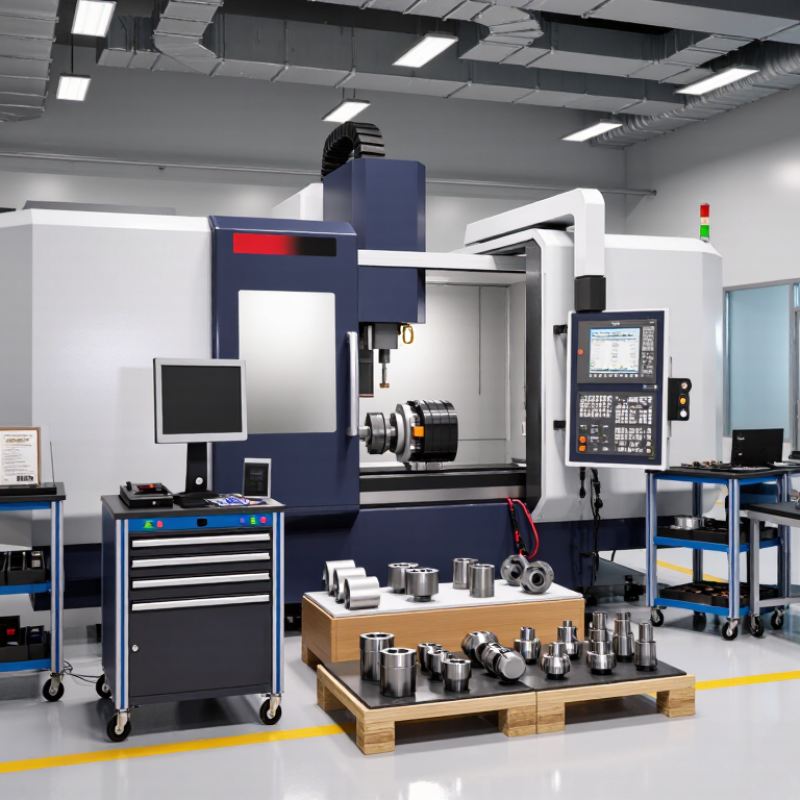
The global CNC parts manufacturing industry connects engineering teams, machine shops, and distributors across many regions. Buyers often compare suppliers by tolerance, material control, capacity, and communication quality. A capable manufacturer should explain machining methods clearly, from multi-axis milling to precision turning. They should also provide inspection records, material certificates, and consistent part numbering. These details reduce confusion when components cross borders.
Real experience shows that a low price can hide extra costs. Rework, unclear drawings, and delayed samples can damage an entire production schedule. Buyers should review a supplier’s experience with similar geometries, surface finishes, and production volumes. A small aluminum bracket may need different controls than a hardened steel shaft. Reliable manufacturers ask practical questions before quoting. That is a good sign, though it does not guarantee perfection. Even strong suppliers can misunderstand a drawing.
Tips:
Leading CNC parts manufacturers combine precision, process control, and practical engineering judgment. Their workshops should support three-, four-, and five-axis machining for complex geometries. They also need reliable control of aluminum, stainless steel, titanium, engineering plastics, and hardened alloys. A capable supplier can hold tight tolerances, but tolerances alone prove little. Surface finish, burr control, thread accuracy, and edge consistency matter on the shop floor. Details matter.
Inspection capability separates serious manufacturers from ordinary job shops. Coordinate measuring machines, optical comparators, calibrated gauges, and documented first-article reports help verify critical dimensions. According to the 2024 Smart Manufacturing and Operations Survey, 86% of manufacturers view smart manufacturing as important for competitiveness over the next five years. That pressure is visible in CNC production. Leading suppliers connect machine data, inspection records, material certificates, and revision histories in one traceable workflow. Buyers should ask how rejected parts are investigated, not only how many parts pass.
Production flexibility is another key capability. World Robotics 2024 reported 541,302 industrial robots installed globally in 2023, showing the expanding role of automation in manufacturing. However, automation cannot replace experienced machinists during difficult setups or unusual material behavior. A strong supplier balances robotic loading with skilled supervision. This is where many claims become vague. Some manufacturers promise repeatability without explaining fixture design, tool-life monitoring, or sampling plans. Buyers should request measurable evidence, such as capability studies, inspection records, and realistic lead-time data. Mistakes still happen. The difference is whether the process detects them early.
Global CNC buyers should judge parts by evidence, not polished capability lists. Material selection affects strength, corrosion resistance, heat response, and cost. Aluminum suits lightweight housings, while stainless steel handles harsh exposure. Engineering plastics reduce weight, but moisture can change dimensions. Specify the exact grade, temper, hardness, and required material certificate.
Tolerances must match function. A drawing stating ±0.01 mm everywhere may increase inspection and machining costs without improving performance. ISO 2768 defines general tolerances, while ASME Y14.5 controls geometric dimensioning and tolerancing. Results depend on alloy, part size, tooling, machine condition, and temperature. A perfect drawing does not guarantee a perfect component. That assumption deserves review.
Tips: Request material certificates, first-article inspection reports, calibration records, and measured dimensions. The ISO Survey 2023 recorded over 1.2 million ISO 9001 certificates worldwide. Yet certification alone cannot prove every part is accurate. Ask for sampling plans, surface-finish readings, and actual inspection data. NIST Handbook 143 supports traceable measurement practices through calibrated equipment. Keep critical datums visible. Small omissions become expensive corrections.
| Material Family | Common International Grades | Typical CNC Applications | Typical General Tolerance | Precision Feature Tolerance* | Typical Machined Surface Roughness | Relevant Standards and Certifications | Recommended Quality Documentation |
|---|---|---|---|---|---|---|---|
| Aluminum Alloys | 6061-T6 6082-T6 7075-T6 | Housings, brackets, aerospace structures, heat sinks, inspection fixtures, and lightweight machine components. | Approximately ±0.10 mm to ±0.30 mm for many standard features, depending on part size, geometry, and drawing requirements. | Approximately ±0.01 mm to ±0.05 mm for selected features when controlled process planning and inspection are used. | Ra 1.6–3.2 µm is common after standard milling or turning; Ra below 0.8 µm may require additional finishing. | ISO 2768 for general tolerances; ASTM B221 or EN 755 for aluminum extrusions; ISO 9001 quality management. | Material certificate, dimensional inspection report, coating or anodizing certificate, and first-article inspection report when required. |
| Stainless Steel | 304 316L 17-4 PH | Medical components, food-processing parts, chemical equipment, valve bodies, shafts, and corrosion-resistant assemblies. | Approximately ±0.10 mm to ±0.30 mm for general machined dimensions, subject to feature size and thermal conditions. | Approximately ±0.01 mm to ±0.05 mm for controlled critical dimensions; tighter values require an explicit drawing specification. | Ra 1.6–3.2 µm is typical for CNC machining; polishing or grinding may be needed for lower roughness. | ASTM A276 or ASTM A479 for stainless steel bar and fabricated products; ISO 2768; ISO 9001. | Heat-lot material certificate, hardness report when specified, dimensional report, passivation certificate, and surface-finish record. |
| Carbon and Alloy Steel | AISI 1045 4140 A36 | Gears, shafts, tooling plates, couplings, machine frames, fixtures, and wear-resistant mechanical parts. | Approximately ±0.10 mm to ±0.30 mm for general dimensions under standard CNC production conditions. | Approximately ±0.01 mm to ±0.05 mm for selected dimensions with suitable tooling, workholding, and verification. | Ra 1.6–3.2 µm is common; heat treatment, grinding, or honing may be required for wear or bearing surfaces. | ASTM A29 or ASTM A108 for steel bars; ASTM A36 for structural carbon steel; ISO 2768; ISO 9001. | Mill test certificate, heat-treatment chart, hardness report, dimensional inspection report, and coating certificate if applicable. |
| Tool Steel | D2 H13 P20 | Molds, dies, punches, cutting tools, inserts, wear plates, and high-load production tooling. | Approximately ±0.05 mm to ±0.20 mm for general features, depending on hardness, geometry, and whether machining occurs before or after hardening. | Approximately ±0.005 mm to ±0.03 mm for selected critical features when precision machining, grinding, or wire EDM is applied. | Ra 0.8–3.2 µm after CNC machining; polished mold cavities may require additional polishing to meet optical or molding requirements. | ASTM A681 for tool steels; ISO 2768 where applicable; ISO 9001; heat-treatment requirements defined by the part drawing or process specification. | Material certificate, heat-treatment and hardness report, CMM report, cavity or profile inspection, and surface-finish record. |
| Brass and Copper Alloys | C360 C464 C110 | Electrical contacts, plumbing components, manifolds, connectors, heat-transfer parts, and decorative hardware. | Approximately ±0.05 mm to ±0.20 mm for many turned or milled features, depending on the alloy and part geometry. | Approximately ±0.01 mm to ±0.03 mm for selected features using controlled CNC turning or milling processes. | Ra 0.8–3.2 µm is common; polishing, brushing, or plating may alter the final measured surface condition. | ASTM B16 or ASTM B124 for brass products; ASTM B152 for copper plate and sheet; ISO 2768; ISO 9001. | Material certificate, elemental composition report when required, dimensional report, plating certificate, and visual inspection record. |
| Engineering Plastics | POM / Acetal PA6 / Nylon PEEK PTFE | Insulators, bushings, low-friction guides, seals, medical prototypes, electrical parts, and lightweight mechanical components. | Approximately ±0.10 mm to ±0.30 mm; moisture absorption, thermal expansion, creep, and part size can significantly affect stability. | Approximately ±0.02 mm to ±0.10 mm for selected features, with dimensional allowances often required for environmental conditions. | Ra 1.6–6.3 µm is common; the achievable finish depends on polymer type, cutter geometry, feed rate, and heat control. | ASTM D638 or ISO 527 for tensile characterization; ASTM D695 or ISO 604 for compression; ISO 9001; FDA or USP Class VI requirements where applicable. | Resin or lot certificate, dimensional report, moisture or conditioning record when relevant, material compliance statement, and visual inspection record. |
| Titanium Alloys | Grade 2 Grade 5 / Ti-6Al-4V | Aerospace brackets, medical implants and instruments, chemical-processing components, and high-strength lightweight parts. | Approximately ±0.10 mm to ±0.30 mm for general dimensions; distortion and residual stress require careful process control. | Approximately ±0.01 mm to ±0.05 mm for selected features when appropriate tooling, coolant, workholding, and inspection are used. | Ra 1.6–3.2 µm is common after CNC machining; critical bearing or sealing surfaces may require secondary finishing. | ASTM B265 for titanium plate and sheet; ASTM B348 for titanium bar and billet; ISO 2768; ISO 9001; AS9100 for aerospace supply chains when required. | Material traceability certificate, chemical and mechanical test results, dimensional report, surface-treatment certificate, and full inspection plan. |
| Nickel-Based Alloys | Inconel 625 Inconel 718 Hastelloy C276 | Hot-section aerospace parts, energy equipment, chemical-processing hardware, exhaust components, and high-temperature fixtures. | Approximately ±0.10 mm to ±0.30 mm for general dimensions; work hardening and heat generation can reduce process stability. | Approximately ±0.02 mm to ±0.05 mm for selected features using rigid equipment, specialized tooling, and controlled cutting parameters. | Ra 1.6–3.2 µm is common; grinding or advanced finishing may be necessary for sealing or fatigue-critical areas. | ASTM B443 or ASTM B670 for nickel-alloy plate and sheet; ASTM B637 for precipitation-hardened nickel alloys; ISO 9001; AS9100 where applicable. | Heat-lot material certificate, chemical analysis, mechanical-property report, dimensional inspection, hardness report, and non-destructive testing where specified. |
*Tolerance values are practical manufacturing benchmarks, not universal guarantees. Final acceptance should always follow the approved engineering drawing, specified GD&T requirements, material condition, part size, inspection method, and applicable industry standard. ISO 2768 does not replace individually specified tolerances for critical features.
Global buyers should evaluate CNC parts manufacturers beyond unit price. Ordering begins with a controlled drawing package, including material grade, tolerances, surface finish, inspection points, and revision status. A missing tolerance can create expensive rework. It happens more often than buyers admit.
The 2023 World Bank Logistics Performance Index shows that customs clearance and shipment tracking strongly affect supply-chain reliability. Request a commercial invoice, packing list, certificate of origin, and accurate HS classification before production. Confirm Incoterms in writing, because “delivered” can hide duties, taxes, or unloading costs. Ocean freight carries roughly 80% of global trade by volume, according to UNCTAD’s Review of Maritime Transport 2023. Sea transport costs less, but port delays can disrupt a tight production schedule. Air freight suits urgent prototypes, not usually heavy batches.
Compliance needs technical attention. Ask for material certificates, dimensional inspection records, and traceability for each lot. Check whether the destination requires product declarations, restricted-substance documentation, or special marking. Export-control screening should cover the part, end use, destination, and involved parties. Do not treat a supplier’s general certificate as universal proof. Requirements vary by jurisdiction. A practical purchase order should define sampling plans, nonconformance handling, packaging protection, and document retention. Wooden crates may need approved treatment marks. That detail is easy to miss. Build a realistic buffer into delivery dates, because perfect forecasts are uncommon. Supplier audits and pre-shipment inspections add cost, but they can expose weak process control before containers leave the port.
Indicative planning ranges for a CNC parts order, measured in calendar days. Actual timing depends on part complexity, production capacity, destination, shipping mode, customs documentation, and inspection requirements.
For global purchasing, buyers should confirm technical drawings and tolerances before ordering, agree on inspection standards, select an appropriate Incoterm, prepare accurate commercial documents, and verify import duties, product classification, and destination-country compliance requirements.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru