Choosing the top Flue Gas Desulfurization Equipment suppliers requires more than comparing catalog prices. Plant operators must examine sulfur content, boiler capacity, gas temperature, water availability, limestone quality, and maintenance access. A scrubber that performs well in a coastal power station may struggle beside a dry inland cement kiln.
The U.S. Environmental Protection Agency reports that modern wet scrubbers can achieve sulfur dioxide removal efficiencies above 90%, with some systems approaching 99%. The European Commission’s Large Combustion Plants reference documents also identify wet limestone systems as a mature solution for large boilers. Meanwhile, the International Energy Agency continues to track coal-fired generation as a major source of global emissions, keeping desulfurization investment commercially important.
Dr. Bruce G. Miller, a recognized flue-gas treatment specialist, states, “There is no single best FGD system; the best choice depends on coal, boiler, and site conditions.” That warning deserves attention. Supplier rankings can look precise, but performance data are not always comparable. Some vendors publish pilot results. Others provide only design guarantees.
This guide compares leading suppliers through engineering capability, removal efficiency, corrosion control, reagent use, by-product handling, delivery experience, and after-sales support. It also considers lifecycle cost, not only the initial quotation. Small details matter. A poorly positioned inspection door can increase shutdown time. A weak slurry-control system can reduce reliability.
The analysis draws on EPA technical guidance, European Commission BREF documents, IEA energy data, and publicly available supplier records. Some market forecasts remain inconsistent. That limitation should be acknowledged, not hidden.
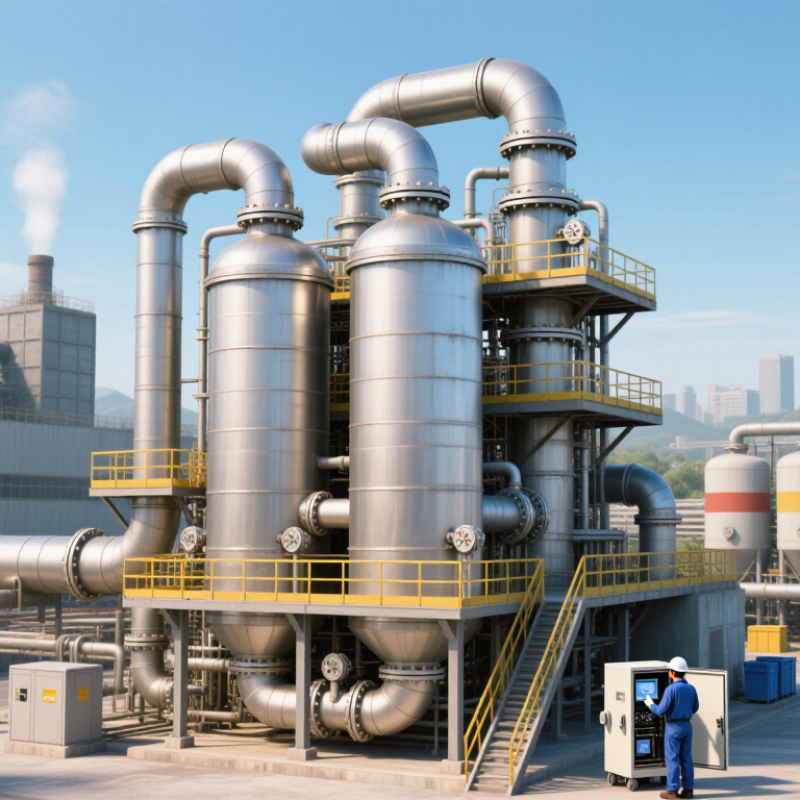
Flue gas desulfurization equipment removes sulfur dioxide from exhaust gases produced by coal-fired boilers, industrial furnaces, and waste-to-energy systems. It is commonly called an FGD system. The equipment sits between the combustion unit and the stack, where it treats hot gas before release.
A wet scrubber sprays limestone slurry through an absorber tower. Sulfur dioxide reacts with the slurry and forms calcium sulfite or calcium sulfate. Pumps circulate the liquid, while mist eliminators capture fine droplets. Oxidation air can improve gypsum formation. Dewatering equipment then separates usable solids from wastewater.
Dry and semi-dry systems use lime-based materials instead of large volumes of slurry. They can require less water, but their performance depends heavily on temperature and moisture control.
A reliable system also includes fans, ducts, valves, sensors, and a control platform. Operators monitor sulfur dioxide levels, pressure loss, slurry density, pH, and outlet moisture. Small measurement errors can affect compliance and maintenance costs.
It is not only a tower.
When comparing equipment suppliers, buyers should examine removal efficiency, corrosion protection, spare-parts access, energy use, and operating records.
Site conditions matter more than impressive brochures. A system designed for one fuel may perform poorly with another.
No FGD installation is perfect; scaling, nozzle blockage, and pump wear still occur. Careful inspection remains necessary.
How FGD Systems Work and Where They Are Used
Flue gas desulfurization (FGD) systems remove sulfur dioxide before combustion gases reach the stack. In a wet limestone scrubber, fans push hot flue gas through a spray tower. Limestone slurry reacts with sulfur dioxide and forms calcium sulfite. Air oxidation then produces gypsum, which may support wallboard manufacturing. According to the U.S. Environmental Protection Agency, wet FGD systems can achieve sulfur dioxide removal efficiencies above 90%, depending on operating conditions. Dry and semidry systems use less water, but their performance can vary with fuel chemistry and equipment control.
FGD is widely used in coal-fired power stations, industrial boilers, metal processing plants, and some waste-to-energy facilities. The International Energy Agency reported that coal-fired generation remained close to 10,000 terawatt-hours in 2023, keeping sulfur control relevant in many regions. Yet equipment selection is not simply about removal percentage. Operators must examine limestone quality, chloride levels, wastewater capacity, corrosion protection, and maintenance access. Small details matter. A blocked spray nozzle can reduce contact between gas and slurry, raising outlet emissions.
Experience also shows that laboratory performance does not always match field results. Load changes, ash buildup, and poor absorber cleaning can weaken reliability. Suppliers should therefore provide verified guarantees, process monitoring, spare-parts planning, and operator training. The most credible evaluation uses stack-test data, documented operating histories, and site-specific mass balances rather than attractive brochure figures.
| FGD System Type | Core Operating Principle | Typical Sorbent or Reagent | Typical SO₂ Removal | Main Equipment Supplied | By-Product or Waste Stream | Water Demand | Common Applications |
|---|---|---|---|---|---|---|---|
| Wet Limestone FGD | Flue gas passes through an alkaline limestone slurry. Sulfur dioxide is absorbed and oxidized to form calcium sulfite and, when air is added, gypsum. | Ground limestone and process water | 90–99% | Absorber tower, slurry tanks, recirculation pumps, limestone preparation system, oxidation air blower, mist eliminator, gypsum dewatering unit | Saleable or disposable gypsum, wastewater containing dissolved salts and suspended solids | High | Large coal-fired power stations, industrial boilers, refineries, and major process plants |
| Wet Lime FGD | A lime slurry reacts with sulfur dioxide in a spray tower or packed absorber. Lime is more reactive than limestone and can reduce reagent residence time. | Hydrated lime or quicklime converted into lime slurry | 90–99% | Absorber, lime slaking system, slurry circulation pumps, spray headers, mist eliminators, sludge handling equipment | Calcium sulfite or calcium sulfate sludge | High | Industrial boilers, waste-to-energy plants, chemical facilities, and applications requiring fast reagent reaction |
| Seawater FGD | Natural seawater alkalinity absorbs sulfur dioxide. The resulting sulfur compounds are oxidized in an aeration basin before the treated water is discharged under environmental controls. | Seawater; no added limestone is normally required | 90–98% | Absorber tower, seawater pumps, aeration basin, dilution system, monitoring instruments, discharge channel | Primarily dissolved sulfate and treated seawater; no solid gypsum product | Process water is seawater; freshwater demand is low | Coastal power plants and industrial facilities with suitable seawater intake and discharge conditions |
| Spray Dry Absorber | An atomized alkaline slurry contacts hot flue gas. Water evaporates while sulfur compounds react with the sorbent and form a dry powder. | Hydrated lime or lime-based slurry | 80–95% | Spray dryer absorber, rotary atomizer or dual-fluid nozzles, lime preparation system, fabric filter, ash conveying system | Dry mixture of calcium compounds, unreacted sorbent, fly ash, and captured pollutants | Medium; water evaporates into the flue gas | Medium-sized boilers, waste incinerators, biomass plants, and facilities needing a dry residue |
| Circulating Dry Scrubber | Dry hydrated lime particles circulate through a reactor and fabric filter. Recirculation increases contact time and sorbent utilization. | Hydrated lime, sometimes with humidification water | 90–98% | Absorber reactor, humidification system, fabric filter, solids recirculation conveyor, lime storage and dosing equipment | Dry calcium-based reaction products mixed with captured particulate matter | Low to medium | Coal-fired boilers, industrial furnaces, waste-to-energy facilities, and retrofit projects with limited space |
| Dry Sorbent Injection | Dry alkaline powder is pneumatically injected into the furnace, economizer, or flue-gas duct. The reacted material is captured downstream by a particulate-control device. | Hydrated lime, sodium bicarbonate, or trona | 50–80% | Sorbent silo, metering feeder, pneumatic conveying system, injection lances, control system, downstream baghouse or ESP | Dry unreacted sorbent mixed with fly ash and reaction products | Very low; no slurry system is required | Small to medium boilers, peak-load units, emergency sulfur-control projects, and space-constrained retrofits |
| Dual-Alkali FGD | A soluble sodium-based solution absorbs sulfur dioxide, while a separate calcium-based regeneration step produces an insoluble calcium sulfite or gypsum product. | Sodium carbonate or sodium hydroxide with lime or limestone regeneration | 90–99% | Absorber, alkaline liquor tanks, clarifier, regeneration reactor, oxidation system, pumps, and solids dewatering equipment | Calcium sulfite or gypsum, with controlled purge wastewater | High | High-sulfur fuels, industrial boilers, smelters, and plants requiring strong absorption with reduced scaling risk |
| Regenerable FGD | A sorbent absorbs sulfur dioxide and is thermally or chemically regenerated. The concentrated sulfur stream may be processed into sulfuric acid or elemental sulfur. | Regenerable alkaline sorbents, including selected carbon-based or metal-oxide systems | 90–99% | Absorber, sorbent regeneration unit, sulfur-product recovery system, heat exchangers, gas treatment equipment, and controls | Concentrated sulfur dioxide or recovered sulfur products; relatively little solid waste | Low to medium, depending on the process | Large industrial plants where sulfur recovery and reduced solid waste justify higher process complexity |
| Key Supplier Capability | Effective suppliers typically integrate gas-flow modeling, absorber design, reagent handling, particulate control, wastewater treatment, electrical systems, automation, commissioning, and long-term service. | Selected according to fuel sulfur content, flue-gas temperature, reagent availability, water balance, and waste-disposal requirements | Project-specific; verified through guarantees, testing, and operating data | Engineering, procurement, construction support, equipment packages, instrumentation, performance testing, spare parts, and maintenance services | Must comply with local waste, wastewater, air-emission, and by-product regulations | Depends on the selected FGD process | Power generation, cement, metals, chemicals, petroleum refining, marine facilities, and waste-to-energy plants |
| Primary Selection Factors | System selection should consider required sulfur dioxide limit, inlet gas volume, sulfur content, particulate loading, available space, operating flexibility, reliability, and the desired by-product route. | Limestone, lime, sodium compounds, seawater, or a regenerable sorbent | Must meet the applicable permit limit and performance guarantee | Compare absorber size, fan power, pumps, filters, reagent systems, wastewater equipment, and control architecture | Evaluate gypsum quality, dry-residue disposal, wastewater treatment, and potential by-product revenue | Balance water availability, discharge limits, evaporation, and zero-liquid-discharge requirements | Choose wet, semi-dry, or dry technology according to plant scale and site conditions |
Selecting top flue gas desulfurization equipment suppliers requires more than comparing brochure prices. Evaluate their experience with similar fuels, boiler sizes, sulfur levels, and operating conditions. A supplier should provide verified performance data, not only laboratory projections. Ask for references from facilities with comparable gas volumes and corrosion risks.
Technical expertise appears in the details. Review sulfur dioxide removal efficiency, pressure drop, absorber design, slurry circulation, oxidation control, and mist eliminator performance. Request expected reagent use and wastewater characteristics. Inspect the proposed materials, especially around chloride-rich slurry zones. Small design choices matter. A reliable supplier also explains instrumentation, automation, emergency operation, and spare-part availability. Their engineers should visit the site before final sizing.
Commercial reliability deserves equal attention. Compare lifecycle costs, commissioning support, operator training, maintenance access, and documented response times. Examine warranty terms carefully. A low purchase price can become expensive when pumps fail or scaling reduces capacity. I would not trust impressive guarantees without clear test methods and operating limits. Even experienced suppliers can underestimate dust loading, fluctuating fuel quality, or local water chemistry. That uncertainty should appear in the risk assessment. Ask how the supplier handles performance shortfalls and design changes. Their answers often reveal more than polished presentations.
Top Flue Gas Desulfurization Equipment Suppliers: Leading Global Suppliers and Their Product Strengths
Global FGD suppliers now compete on removal efficiency, water use, maintenance access, and operating flexibility. The U.S. Environmental Protection Agency’s Air Pollution Control Cost Manual reports that wet limestone scrubbers can achieve sulfur dioxide removal above 90% under suitable conditions. This explains their continued use in large coal-fired and industrial facilities. However, performance depends on coal chemistry, absorber design, nozzle condition, and operator discipline.
Leading suppliers typically offer wet, dry, and semi-dry systems. Wet systems suit high-sulfur fuel and large gas volumes. Their strengths include stable absorption and gypsum by-product production. Dry sorbent injection uses less water and requires simpler equipment. It can fit smaller plants or sites facing water restrictions. Semi-dry systems provide a middle path, with spray dryers, lime slurry, and compact footprints. The International Energy Agency has repeatedly identified efficiency upgrades and emissions controls as important tools during the energy transition, especially where existing plants remain active.
Strong suppliers also provide process modeling, corrosion-resistant materials, online monitoring, and spare-parts planning. These details matter beside a hot absorber tower. A blocked nozzle can reduce contact efficiency quickly. A poorly tuned reheater can increase energy consumption. Market reports from MarketsandMarkets estimate continued growth in the global FGD market, driven by tighter emission standards and industrial expansion. Still, market forecasts are not guarantees. Equipment buyers should test site-specific gas data, lifecycle costs, wastewater needs, and maintenance records before selecting a supplier.
Typical sulfur dioxide removal performance varies by FGD technology, coal or fuel characteristics, reagent quality, and operating conditions. The values below represent representative midpoints of commonly reported performance ranges rather than data from any individual supplier or brand.
Wet limestone systems generally provide the highest removal efficiency, while seawater, spray-dry, and dry sorbent injection systems can offer advantages in water use, footprint, or simpler operation.
Selecting the right flue gas desulfurization supplier requires more than comparing equipment prices. Start with coal or fuel sulfur content, gas flow, inlet temperature, and required outlet limits. A supplier should model these conditions using measured plant data, not optimistic assumptions. Wet limestone systems often achieve above 90% sulfur dioxide removal, according to the U.S. EPA Air Pollution Control Cost Manual. Higher performance may require additional absorber stages, better mist elimination, or more reagent control.
Check the supplier’s engineering record carefully. Ask for verified operating data from plants with similar fuel, capacity, and wastewater conditions. The EU Large Combustion Plants BREF links achievable emission levels with process design, fuel quality, and operating discipline.
This matters because a system meeting its guarantee during commissioning may perform differently after years of scaling and nozzle wear. Request details on corrosion-resistant materials, pump redundancy, gypsum quality, and maintenance access. Small design omissions become expensive later.
Reliability is not only mechanical. It includes commissioning support, operator training, spare-part availability, and transparent performance testing. Compare lifecycle cost, not only capital cost. The cheapest proposal can create higher limestone use, fan power, and disposal expenses. That is easy to underestimate. Independent testing should confirm removal efficiency, pressure drop, and water consumption. Some project teams still accept generic guarantees without defining test conditions. That deserves a second look. A capable supplier should explain its assumptions plainly and identify where performance remains uncertain.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru