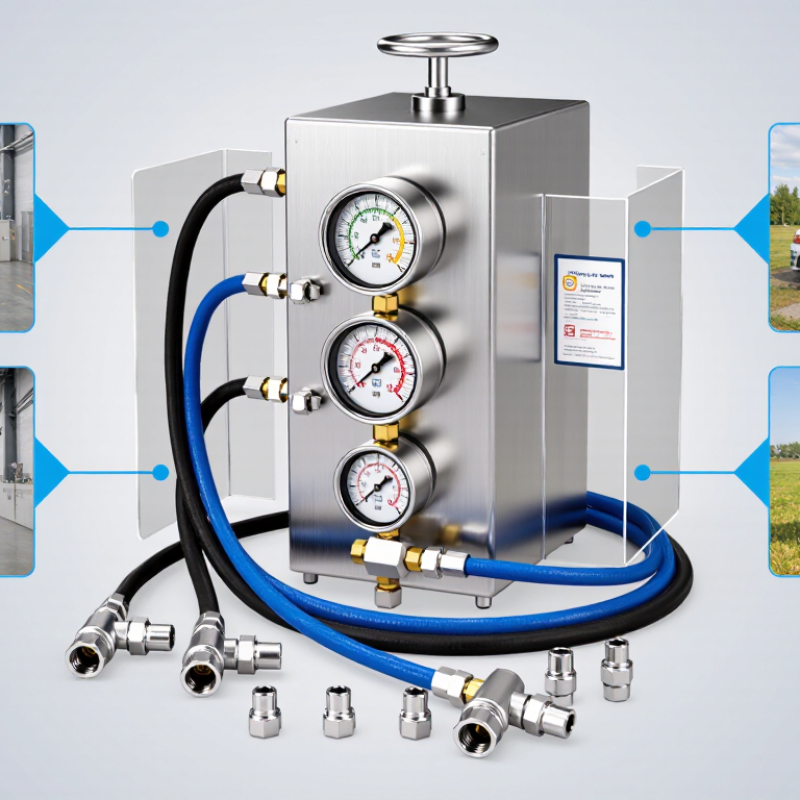
Global buyers need more than a machine that displays rising pressure. They need confidence in every reading, connection, and test record. A reliable Hydraulic Hose Pressure Tester should expose weak assemblies before they enter demanding service. It should also support safe, repeatable decisions across workshops, factories, and mobile maintenance teams.
Hydraulic testing specialist Daniel R. Moore offers a practical reminder: “A pressure test is useful only when the gauge, hose, and record can be trusted together.” That principle shapes this guide. We examine pressure range, accuracy, calibration evidence, fitting compatibility, guarding, fluid control, and data logging. We also consider portability, because a compact tester may serve a field technician better than a larger bench unit. Sometimes, smaller wins.
Experienced buyers should compare working pressure with proof-test pressure, not confuse the two. They should check whether the instrument follows recognized practices such as ISO 1402 and relevant hose specifications. A clear calibration certificate matters. So does a readable gauge under workshop lighting.
The best equipment does not remove human judgment. Operators still need correct adapters, clean connections, controlled pressurization, and suitable protective barriers. One overlooked seal can distort an otherwise careful result. That is the uncomfortable part.
This introduction evaluates leading Hydraulic Hose Pressure Tester options for international purchasers. It focuses on measurable performance, service support, documentation, and practical ownership costs. Some products appear impressive on paper but offer limited regional support. Others lack polished software yet perform consistently for everyday testing. The right choice depends on risk, workload, hose types, and the quality of evidence behind each specification.
Hydraulic hose pressure testers generally fall into three groups: manual, pneumatic, and automated systems. Manual testers use a hand pump and a calibrated gauge. They suit workshops handling occasional repairs, short hoses, and moderate test volumes. Operators can feel pressure changes directly, but readings depend heavily on technique. That is a weakness.
Pneumatic testers use compressed air to drive hydraulic fluid through the test circuit. They reduce physical effort and provide steadier pressure for repeated checks. They work well in service centers testing several assemblies daily. However, the air supply must remain dry and stable. ISO 1402 specifies hydrostatic testing methods, while ISO 6803 addresses impulse testing for hydraulic hose assemblies. These standards help define pressure, timing, and equipment requirements. MarketsandMarkets’ 2024 hydraulic hose market report projects continued growth through 2029, increasing demand for faster and more repeatable inspection equipment.
Automated systems control pressure ramps, hold times, leak detection, and digital records. They are valuable for production lines, certification work, and traceability audits. A practical setup should include guarding, emergency shutdown, calibrated sensors, and a test medium compatible with the hose. Automated does not mean foolproof. Poorly entered test parameters can create precise but wrong results. In real workshops, I would match the tester to hose diameter, working pressure, test frequency, and operator skill. The cheapest system may become expensive when retesting, downtime, and undocumented failures appear.
ISO 1402 defines hydrostatic pressure testing for rubber and plastic hoses. A suitable tester should raise pressure smoothly, hold it steadily, and record results clearly. Operators commonly check leakage, visible damage, proof pressure, and burst pressure. The exact pressure and holding time must come from the hose specification, not guesswork.
A calibrated pressure sensor matters. So does a guarded test chamber. Water is normally preferred because it stores less energy than compressed gas. Keep the test area controlled.
ISO 19879 applies mainly to metallic tube connections used in hydraulic systems. It describes test methods for connection performance, including leakage resistance and pressure capability. This matters when a hose assembly includes metal adapters, tube ends, or mechanical fittings.
Testers for global buyers should support controlled ramp rates, accurate data logging, and traceable calibration records. A practical detail is often missed: the fitting, hose, and tester must share compatible pressure ranges. Otherwise, the weakest part controls the result. That is not always obvious.
Experienced technicians also inspect hose routing, fitting alignment, and seal condition before pressurizing.
A pressure reading alone cannot prove assembly quality. Some test programs need impulse, vacuum, or temperature testing beyond these standards.
ISO 1402 and ISO 19879 should guide the method, while the product specification defines acceptance.
Field conditions can be imperfect. Review the procedure after each failure.
That habit improves reliability.
For global buyers, a pressure tester should make SAE J517 limits easy to verify. The key figure is the hose’s maximum working pressure. Under SAE J517, the minimum burst pressure is commonly four times that value. A 3,000 psi working rating therefore indicates a 12,000 psi minimum burst benchmark. That figure is not a routine test setting. It describes failure resistance.
Choose a tester whose rated output covers the required procedure without operating at its limit. Use the lowest pressure rating among the hose, fittings, adapters, and test chamber. A stronger hose cannot upgrade a weaker coupling. Small detail matters. Trapped air can store dangerous energy during testing. Fill the assembly with compatible fluid, remove air, and increase pressure gradually. Watch the gauge and connection points. A calibrated digital gauge helps, but calibration records still need review. Burst testing is destructive. Use shielding, remote control, and a suitable relief system. Never treat the 4:1 ratio as permission to test every assembly at four times working pressure.
In practice, compare pressure range, accuracy, data logging, fluid compatibility, and service support. A tester rated far above the job may offer poor low-pressure resolution. That surprised me during equipment checks. More capacity is not always more control. Temperature can also change hose behavior and readings. Record hose size, construction, temperature, test medium, ramp rate, and failure pressure. If the procedure is unclear, pause and confirm the applicable specification. I once trusted a readable gauge too quickly. Its display was clear, but its calibration status was not. Reliable testing depends on the whole setup, not one impressive number.
Global buyers need hydraulic hose pressure testers that produce more than a passing number. A digital display should show pressure clearly, even beside a noisy assembly line. During field inspections, I look for stable readings, responsive controls, and repeatable test cycles. Different technicians should reach similar results. Small details matter. A pressure spike of 5 bar can change a pass decision.
Calibration is the foundation of credible results. The tester should support traceable calibration with defined intervals and accessible certificates. Before testing, operators should inspect fittings, seals, and the pressure sensor. I have seen good equipment deliver questionable data after a neglected sensor check. That weakness is easy to overlook. Calibration records should identify the instrument, date, reference standard, and technician.
Data logging turns a test into usable evidence. Look for time-stamped results, hose identification, peak pressure, hold time, and operator details. Exportable files help quality teams compare production sites and answer customer audits. Yet automatic records are not perfect. Incorrect hose numbers or skipped fields can weaken an otherwise reliable report. Clear prompts and secure user access reduce these errors. For global compliance, teams should map stored data to internal procedures and applicable market requirements, rather than assuming one format fits every region.
Top Hydraulic Hose Pressure Testers for Global Buyers
A pressure tester is only as credible as its safety evidence. The ILO reported nearly three million work-related deaths annually in 2023, making basic risk controls impossible to ignore. For European shipments, check the CE declaration, risk assessment, technical file, and applicable machinery standards. CE is a conformity declaration, not always independent certification. This distinction is often missed.
Look for guarding designed under ISO 14120 and hydraulic safety practices aligned with ISO 4413. A steel enclosure should contain hose fragments during rupture testing. The viewing window must resist impact and remain clear after repeated cycles. Emergency shutdowns should be reachable without leaning across the test chamber, following ISO 13850 principles. Test the button physically. A label alone proves little.
For North American buyers, verify whether electrical parts and the complete tester require recognized safety certification, such as UL evaluation. Ask for the exact standard, certificate scope, and production inspection method. ISO 19879 also supports consistent testing of hydraulic hose assemblies, including pressure measurement and test records. Record the hose ID, test pressure, hold time, calibration date, and operator. Digital logs help, but they can still contain wrong entries. I have seen excellent machines fail practical reviews because relief valves were poorly adjusted or guards were awkward to close. Certification reduces uncertainty; disciplined inspection removes more.
| Evaluation Dimension | Standards-Based Requirement or Benchmark | What Global Buyers Should Verify | Safety and Purchasing Significance | Recommended Status |
|---|---|---|---|---|
| Pressure Range | Testing capacity should cover the maximum working pressure of the hose assemblies, with suitable margin for proof and burst testing. Many hydraulic hose standards use proof pressures around 2 times working pressure and burst pressures around 4 times working pressure, but the applicable hose standard must be confirmed. | Check the maximum rated test pressure, pressure units, pressure transducer range, and whether the system supports MPa, bar, psi, or interchangeable displays. | Insufficient range can make the tester unsuitable for the intended hose class and may encourage unsafe overloading of the equipment. | Required |
| Pressure Accuracy | A calibrated pressure-measuring system is required for dependable test results. Accuracy should be stated as a percentage of full scale or of reading, together with the operating temperature range. | Request the instrument accuracy specification, calibration certificate, calibration interval, serial-number traceability, and calibration method. | Accurate measurement supports repeatable acceptance decisions and reduces the risk of approving weak assemblies or rejecting compliant assemblies. | Required |
| Applicable Hose Test Standards | ISO 1402 is widely used for hydrostatic testing of rubber and thermoplastic hoses. ISO 19879 covers test methods for hydraulic fluid power hose assemblies, while ISO 6803 addresses hydraulic hose impulse testing. | Confirm which standards the tester can support and whether the supplied software, fixtures, and test reports use the correct test sequence and hold time. | Standards compatibility is more important than a generic pressure rating because different hose types require different procedures. | Required |
| CE Compliance for EU Buyers | CE marking indicates that the manufacturer declares conformity with applicable European Union requirements. Depending on the machine design, relevant legislation may include the Machinery Directive or Machinery Regulation, the Low Voltage Directive, and the EMC Directive. | Request the EU Declaration of Conformity, technical documentation details, risk assessment summary, operating instructions, and the list of applied harmonised standards. | CE is a regulatory conformity marking, not a general product-quality award or a universal third-party certification. | Required for applicable EU markets |
| UL and North American Acceptance | UL certification or listing is generally voluntary unless required by a purchaser, authority having jurisdiction, insurer, or applicable installation rule. Electrical construction should also be evaluated against relevant North American electrical safety requirements. | Ask whether the complete machine or only individual components have been evaluated. Verify the exact certification scope, file information, voltage, frequency, and factory configuration. | A component mark does not automatically mean that the complete pressure tester is certified. | Verify by market |
| Pressure Guard and Enclosure | The test chamber should use a robust guard, enclosure, or barrier capable of containing foreseeable hose, fitting, and coupling failures during pressurisation. | Inspect guard material, door construction, hinge strength, viewing window rating, access openings, anchoring, and resistance to ejected fragments and hose whip. | Physical containment is a primary control against stored-energy hazards during proof and burst testing. | Required |
| Guard Interlock | Where a hazardous pressure condition can exist, opening the guard should prevent pressurisation and should initiate a safe pressure-release sequence where required by the risk assessment. | Test the interlock under realistic conditions. Verify that bypassing is difficult, faults are detected where required, and the machine cannot restart unexpectedly after guard closure. | An interlocked guard is stronger than a warning label because it links physical access control to the machine safety circuit. | Strongly recommended |
| Emergency Shutdown | An emergency-stop function should be readily accessible, clearly identified, and designed to bring the equipment to a safe state. ISO 13850 provides principles for emergency-stop function design. | Verify the location and color of emergency-stop devices, reset behavior, pressure isolation, depressurisation response, and prevention of automatic restart. | Emergency shutdown should stop hazardous motion and energy generation; it should not be treated as a substitute for guarding or isolation procedures. | Required for risk-controlled designs |
| Hydraulic Isolation and Depressurisation | The system should provide controlled pressure release, isolation from the pressure source, and protection against trapped pressure in the test chamber and hose assembly. | Check bleed valves, dump valves, lockable isolation points, pressure indicators, residual-pressure warnings, and the time required to reach a safe pressure level. | Residual pressure can remain dangerous even after the pump stops, especially when disconnecting fittings or opening the enclosure. | Required |
| Overpressure Protection | A pressure-relief device or equivalent protective control should limit pressure to a safe value consistent with the machine design and test procedure. | Verify relief-valve setting, tamper resistance, discharge routing, maintenance instructions, and whether the relief device is independent of the normal control interface. | Overpressure protection reduces the likelihood of catastrophic equipment failure caused by control faults or incorrect settings. | Required |
| Hose Restraint and Fixture Security | Test fixtures should securely retain hose ends, adapters, and couplings and should control hose movement in the event of rupture or fitting separation. | Confirm compatible thread standards, rated adapters, restraint cables or sleeves, fixture load ratings, and the maximum assembly length and diameter. | Incorrect adapters or inadequate restraint can create projectile and hose-whip hazards even when the pressure source is correctly rated. | Required |
| Control-System Safety | Safety-related control functions should be designed according to the machine risk assessment, with suitable monitoring of critical devices such as guard switches, emergency stops, and pressure sensors. | Request the safety-circuit diagram, component safety ratings, fault-response description, reset logic, and validation records where applicable. | Control reliability is essential when software or automatic sequencing is used for high-pressure testing. | Required for automated systems |
| Electrical Protection | Electrical construction should include appropriate protective earthing, overcurrent protection, enclosure protection, wiring identification, and compatibility with the destination voltage and frequency. | Verify electrical schematics, rated voltage, frequency, short-circuit protection, ingress-protection rating, grounding method, and conformity documentation. | Electrical compliance affects safe installation, inspection, serviceability, and acceptance by local authorities. | Required |
| Noise, Leakage, and Fluid Containment | The design should control hydraulic-fluid leakage and provide suitable containment, drainage, and housekeeping access. Noise exposure should be evaluated where pumps or intensifiers operate frequently. | Check drip trays, drain points, seals, hose routing, fluid compatibility, spill-control provisions, declared sound-pressure levels, and required personal protective equipment. | Leak prevention protects personnel, equipment, floors, and the environment while reducing maintenance downtime. | Recommended |
| Test Data and Traceability | Test records should identify the assembly, test pressure, pressure-hold time, date, operator, instrument identification, and pass/fail result. | Evaluate electronic export formats, audit trails, barcode or serial-number input, report locking, backup options, and the ability to print or export results without proprietary restrictions. | Traceable records support customer acceptance, internal quality systems, warranty investigations, and regulatory audits. | Strongly recommended |
| Calibration and Maintenance | Pressure sensors, gauges, relief devices, interlocks, and emergency-stop circuits require documented inspection and maintenance according to the risk assessment and manufacturer instructions. | Confirm calibration procedures, spare-part availability, service access, recommended inspection intervals, and the process for handling failed calibration results. | Regular verification preserves measurement reliability and keeps safety functions operational over the equipment life cycle. | Required |
| Operator Documentation and Training | Operating instructions should cover setup, approved hose types, maximum pressure, test procedures, emergency response, depressurisation, inspection, and maintenance. | Request manuals in the destination language, safety labels, training materials, lockout or isolation instructions, and documented operator competency requirements. | Clear documentation helps prevent incorrect fixture selection, unsafe access, and operation beyond the tester’s design limits. | Required |
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru