In 2026, Shuttle Automation is helping warehouses move totes, cartons, and pallets through dense storage areas with less manual travel. But “top” does not mean the same thing for every operation. A high-throughput e-commerce site may value rapid order consolidation, while a parts distributor may need reliable access to many small stock-keeping units. The details matter.
This guide compares leading shuttle system approaches and the capabilities buyers should examine before selecting a supplier. Key considerations include storage density, shuttle speed, lift and conveyor integration, software compatibility, scalability, and service support. A fast shuttle is only useful when the full system can keep work flowing. Real performance depends on aisle layout, order profiles, labor practices, and how well equipment communicates with warehouse management software.
Readers will find practical context for evaluating multi-level shuttle systems, pallet shuttles, and goods-to-person solutions. We will also consider installation demands, maintenance access, energy use, and the potential costs of expansion. Published throughput figures can be useful, but they may reflect ideal test conditions rather than a busy facility. That distinction is easy to overlook. No system is best in every building, and a shortlist should be checked against measured site data, reference installations, and clearly defined service commitments. The goal is a more informed comparison—not a promise that automation alone will solve every operational constraint.
What Are the Top Shuttle Automation Systems in 2026?
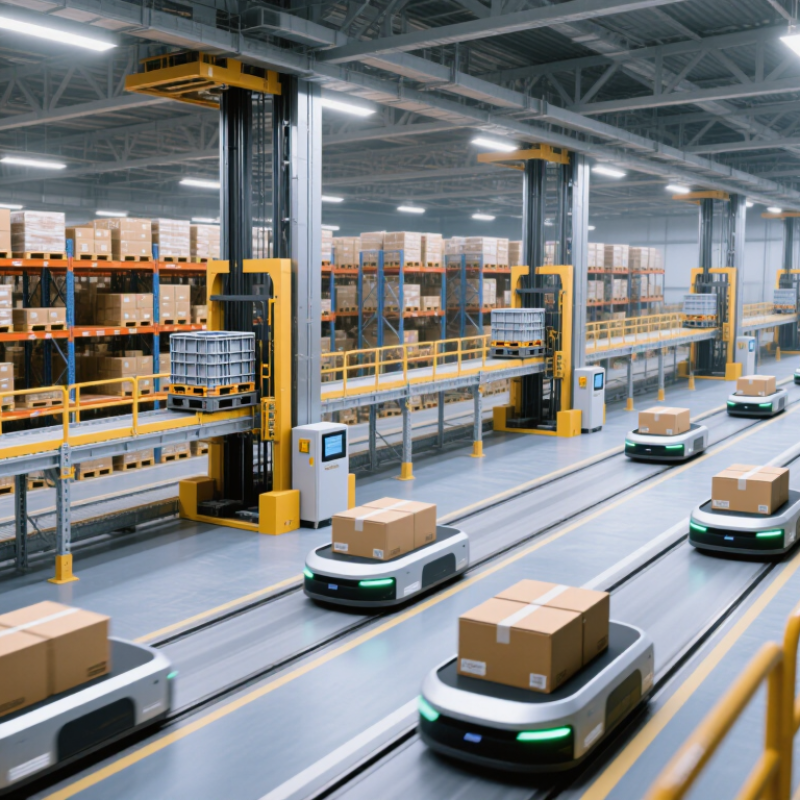
Shuttle automation uses mobile carriers to move totes or cartons through storage lanes and between storage and workstations. The system’s value depends on more than how many shuttles it contains. Two useful measures are loads per hour and storage density. Loads per hour describes throughput: how many handling units the system can reliably move during a set period. A peak-speed figure can look impressive, but sustained performance is more useful.
Measure throughput under realistic conditions. Include the actual mix of items, replenishment tasks, operator pauses, and transfer delays. For example, a system moving 500 loads in a busy hour may perform differently during a full shift. Storage density measures how much usable inventory fits within a given floor area or volume. Count accessible storage positions, not just the theoretical number of lanes. A compact layout may save space but could create congestion or slower retrieval. The trade-off is real.
Tips: Compare systems using the same load definition and operating conditions. Ask for sustained, not just peak, loads per hour. Check whether density figures include aisles, workstations, and service access. Small details matter. Review your own order patterns before setting targets; I’ve seen neat averages hide awkward demand spikes. A pilot can expose assumptions that spreadsheets miss.
Pallet, tote, mini-load, and 4-way shuttles solve different storage problems. In 2026, the right choice depends less on headline speed than on load size, order patterns, and available building space. Pallet shuttles move full pallet loads through deep storage lanes, reducing forklift travel inside dense areas. They work well when many pallets share a product type, but lane depth can make access less flexible. A blocked lane is frustrating.
Tote shuttles handle smaller containers and suit operations with frequent, varied order lines. Mini-load systems typically retrieve cartons or trays from compact storage, balancing storage density with controlled access. Their value depends on how reliably the system connects with picking stations and inventory software. 4-way shuttles travel across multiple directions and levels, which can improve access and make layouts more adaptable. That flexibility also brings more coordination demands. Operators should compare peak throughput, maintenance access, container standards, and recovery procedures—not just storage capacity. A useful assessment uses actual order data and tests busy periods, since forecasts can be wrong. Aisle plans may look tidy on paper, yet even small changes in carton dimensions can affect performance. Choosing a system is rarely a clean calculation; service needs and future product changes deserve careful review.
A headline rate above 1,000 totes per hour sounds compelling, but it needs a clear definition. Does it count tote transfers, totes delivered to a workstation, or completed order lines? These are not interchangeable. A shuttle may move totes quickly while picking, replenishment, or packing becomes the constraint. That distinction matters. Published ratings often assume favorable layouts, steady demand, and tuned software. Real shifts bring uneven orders, replenishment pauses, blocked stations, and occasional tote misalignment. Small interruptions add up.
Compare the stated rate with the actual operating window, not just peak minutes. Ask for test results using your tote dimensions, load weights, SKU mix, and expected order profile. Track sustained throughput and recovery after a jam or station delay. Measure the queues. A useful test reports availability, jams, and manual interventions alongside hourly tote rate. Even careful tests have blind spots; one unusually calm day can flatter the result. If a quote promises more than 1,000 totes per hour, request its assumptions in writing. Then validate performance with a site pilot.
The right shuttle system is the one that fits your inventory, building, and order profile—not simply the one with the largest capacity claim. Start by comparing usable pallet positions with your actual storage requirement. Separate occupied positions from empty locations reserved for growth or operational flexibility. A system may offer impressive nominal capacity, yet leave little room for irregular pallets or changing stock levels.
SKU count matters, too. A site holding 300 fast-moving SKUs has different retrieval demands from one storing 3,000 slow-moving SKUs. Check how the system handles access frequency, replenishment, and product rotation. Measure cube utilization as stored inventory volume divided by usable storage volume. Keep pallet dimensions consistent when comparing options. Small measurement differences can distort the result.
Tips: Record pallet positions, SKU count, and cube utilization during a representative operating period. Include peak demand and seasonal stock, not just an average day. Ask for throughput figures under your own order mix. A spreadsheet can help, but it may miss awkward pallets, blocked aisles, or manual workarounds. Walk the proposed layout with warehouse staff. Their observations often reveal gaps in the model.
A shuttle system should match the work your warehouse actually sees, not just its busiest hour. Peak throughput is not the whole story. Measure concurrent inbound and outbound moves, order patterns, replenishment demand, and the buffer space needed between tasks. A multi-level shuttle may suit dense case or tote storage, while a four-way system can move loads across several aisles. Pallet shuttles may fit deep-lane storage with fewer handling touches. The best choice depends on your load mix.
Check load dimensions carefully: length, width, height, weight, and any overhang. A small variation in pallet size can affect clearances and usable capacity. Then compare the system’s rated performance with your required peak, including lifts, conveyors, and transfer points. A fast shuttle cannot fix a slow handoff. For payback, include installation, software, maintenance, energy, labor changes, and expected downtime—not only equipment cost. Estimate savings under normal demand, then test a slower-growth scenario. This estimate is never neat; forecasts rarely are. A common mistake is trusting one optimistic volume forecast. If the result only works under perfect conditions, revisit the assumptions before committing.
Planning guide: The figures below are indicative engineering ranges, not guaranteed system specifications. Peak throughput depends on layout, lifts, ports, software, staffing, and load mix. Payback estimates assume a high-utilization operation and should be validated with site-specific labor, space, energy, and implementation costs.
| System Type | Typical Load Dimensions and Weight | Indicative Peak Throughput | Best-Fit Use Case | Indicative Simple Payback | Key Selection Consideration |
|---|---|---|---|---|---|
| Radio shuttle for pallet lanes | Pallets commonly around 1,200 × 800 mm or 1,200 × 1,000 mm; typically up to about 1,000–1,500 kg per pallet, subject to rack and shuttle design. | Approximately 20–60 pallet moves per hour per active aisle, depending on travel distance, forklift exchange, and lane depth. | High-volume storage of a limited number of product types, especially where dense, deep-lane storage is more valuable than direct access to every pallet. | About 2–5 years | Compare lane depth and SKU turnover. Deep lanes improve storage density but reduce selectivity and can increase replenishment complexity. |
| Four-way pallet shuttle | Typically standard pallet footprints of 1,200 × 800 mm or 1,200 × 1,000 mm; common design loads are approximately 1,000–1,500 kg per pallet. | Approximately 40–120 pallet moves per hour per operating zone; actual output is often constrained by lifts, transfer points, and the number of active shuttles. | Large pallet-buffer or distribution operations that need dense storage, multiple-level movement, and more routing flexibility than a single-direction lane system. | About 3–6 years | Model lift and interface capacity alongside shuttle count. Adding shuttles alone may not raise system throughput if vertical transfer is the bottleneck. |
| Aisle-based tote or carton shuttle | Commonly totes or cartons up to roughly 600 × 400 mm; load weight often falls in the 20–50 kg range, depending on carrier and rack design. | Approximately 300–1,000 tote or carton movements per hour per aisle; port, lift, and workstation capacity determine the practical rate. | Order picking and replenishment for small goods where fast access to many stored items is more important than pallet-level storage density. | About 3–6 years | Check the full item-to-picker path, including replenishment and workstation ergonomics. Specify whether the quoted rate means storage movements or completed picks. |
| Three-dimensional tote shuttle grid | Typically standardized totes around 600 × 400 mm or smaller; common payloads are approximately 20–50 kg per tote, subject to grid and carrier limits. | Approximately 500–2,000 tote presentations per hour per system in suitably sized installations; the number and placement of ports are major constraints. | Compact, high-throughput e-commerce, retail, or spare-parts operations with many small items and a strong goods-to-person picking requirement. | About 3–7 years | Assess peak order profile, tote replenishment, port utilization, and recovery strategy. Grid capacity and order-picking capacity are different measures. |
| Shuttle-based goods-to-person system | Usually totes or trays up to roughly 600 × 400 mm; typical payloads are around 20–50 kg, with heavier loads requiring a specifically rated design. | Approximately 300–1,000 order lines per hour per picking workstation; the result varies with lines per order, presentation rate, and operator process. | Facilities seeking to reduce picker travel while supporting frequent, small-item orders and predictable workstation workflows. | About 2–5 years | Use order lines per hour—not tote movements alone—to size the operation. Include labor availability, replenishment workload, and workstation staffing in the business case. |
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru