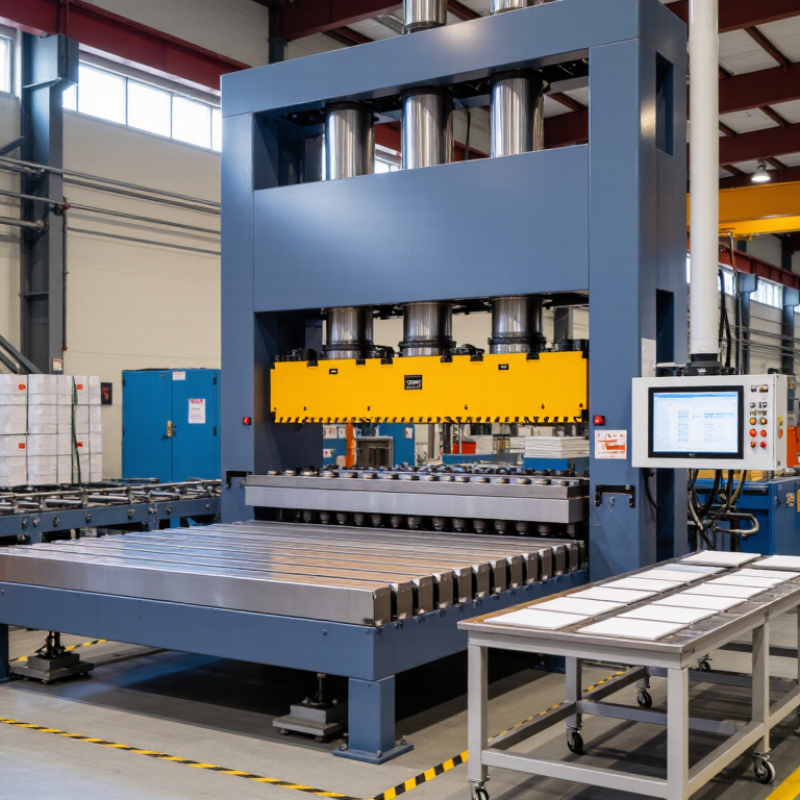
| SMC Slice Material | Material definition | Sheet Molding Compound (SMC) is a pre-impregnated, fiber-reinforced thermoset molding material supplied in sheets or pre-cut charges. | Confirms that the material is designed for compression molding rather than conventional thermoplastic injection molding. |
| Typical resin system | Unsaturated polyester resin is common; vinyl ester and other thermoset systems are also used for specialized performance requirements. | Resin chemistry affects cure behavior, chemical resistance, surface quality, emissions, and press-cycle requirements. |
| Reinforcement | Chopped glass fibers are widely used, commonly in lengths of approximately 25–50 mm; fiber loading often falls in the 10–30% by weight range. | Fiber type, length, and loading influence stiffness, strength, shrinkage, flow, and dimensional stability. |
| Typical density | Approximately 1.5–2.0 g/cm³, depending on resin, glass content, mineral fillers, and formulation. | Useful for estimating part weight, shipping cost, press loading, and material consumption. |
| Common sheet thickness | Many commercial SMC sheets are supplied at approximately 1.5–6 mm, while custom formats may be available outside this range. | The charge thickness must be compatible with the molded part design and the press-loading method. |
| Storage requirement | Many SMC formulations require cool, controlled storage; the exact temperature and shelf life must be confirmed in the supplier’s technical data sheet. | Controlled storage helps preserve flow, tack, cure response, and final mechanical performance. |
| Material form | Continuous rolls, cut sheets, or pre-weighed and pre-cut charges. | Pre-cut charges can reduce handling time and improve material placement consistency in automated or semi-automated production. |
| Press and Process Requirements | Molding method | Compression molding using heated, matched-metal molds. | The press must provide controlled closing, stable pressure, parallel platens, and reliable mold-temperature control. |
| Typical mold temperature | Approximately 140–160°C for many polyester-based SMC systems; the approved formulation determines the final setting. | Accurate temperature balance is essential for complete curing, surface finish, cycle time, and dimensional control. |
| Typical molding pressure | Approximately 5–15 MPa at the molding area, subject to part geometry, material formulation, and mold design. | Press capacity should be calculated from projected part area, required specific pressure, and an appropriate safety margin. |
| Typical cure cycle | Often approximately 1–5 minutes after mold closure, depending on thickness, temperature, chemistry, and part complexity. | Cycle time directly affects production capacity, energy use, and the required number of presses. |
| Press tonnage selection | Determine tonnage from projected area × required molding pressure, then add allowance for process variation and machine safety. | Correct sizing prevents flash, incomplete filling, excessive mold deflection, and premature equipment wear. |
| Preferred press features | Hydraulic or servo-hydraulic drive, programmable pressure and speed profiles, platen parallelism control, heated platens, and safety interlocks. | These features improve repeatability, operator safety, mold protection, and process documentation. |
| Supplier Evaluation Criteria | Capacity range | Confirm available press capacities, daylight, stroke, platen size, and mold-height range against the intended part portfolio. | Ensures one press can accommodate current production needs and planned product expansion. |
| Control and data logging | Request programmable recipes, pressure and temperature monitoring, alarm history, and production data export. | Traceable process data supports quality audits, troubleshooting, and repeatable global production. |
| Electrical and safety compliance | Verify conformity with the destination market’s machinery, electrical, guarding, and emergency-stop requirements. | Compliance can affect import approval, installation, insurance, and workplace acceptance. |
| Installation and service | Evaluate commissioning support, spare-parts availability, remote diagnostics, training, and local service coverage. | Responsive technical support reduces downtime and shortens the learning curve for operators. |
| Testing and acceptance | Include factory acceptance testing, sample-part trials, pressure verification, temperature uniformity checks, and documentation review. | A structured acceptance process verifies that the press can achieve the required SMC part quality before shipment or final payment. |
| Common Applications | Automotive components | Body panels, under-hood parts, battery covers, structural supports, and other corrosion-resistant components. | SMC offers low-density alternatives to some metal parts while providing good stiffness and molded-in detail. |
| Electrical equipment | Enclosures, switchgear covers, meter boxes, cable-management components, and insulation-support parts. | Electrical-grade SMC can provide dimensional stability, insulation, and resistance to environmental exposure. |
| Infrastructure products | Utility cabinets, access covers, drainage components, and corrosion-resistant outdoor housings. | Thermoset composites are useful where weathering, corrosion resistance, and long service life are important. |
| Industrial equipment | Machine covers, pump housings, fan components, protective panels, and chemical-service parts. | Material selection can combine rigidity, corrosion resistance, electrical insulation, and molded surface quality. |
| Consumer and building products | Sanitary components, seating parts, appliance panels, lighting housings, and building-service enclosures. | Compression molding supports repeatable geometry, integrated ribs, inserts, and textured or Class-A-type surfaces when properly formulated. |