Top Cell Assembly Machines for Sale Worldwide
Cell Assembly Machines turn prepared components into finished battery cells through precise, repeatable operations. Depending on the cell format and production plan, a line may include stacking or winding, tab welding, electrolyte filling, sealing, and inspection. Each stage affects the next. A slightly misaligned electrode can create problems that later checks may not catch.
This guide explores machines available from suppliers worldwide and explains how to compare them. It focuses on practical details: supported cell formats, production speed, changeover time, automation level, process monitoring, and after-sales support. Ask for test data using materials similar to your own. A machine’s advertised output may not reflect actual performance across different products or shifts. Small details matter.
Price alone rarely tells the full story. Consider installation, operator training, spare parts, maintenance access, and how easily the equipment can fit into an existing line. Request clear information on accuracy, safety features, quality checks, and service response times. Where possible, review a sample run before making a commitment. No shortlist is perfect. Supplier claims still need scrutiny, and a fast machine is not always the best match. The right choice depends on your cell design, target volume, facility, and team’s experience. A careful comparison can help buyers identify suitable options without treating one specification as the whole answer.
Cell Assembly Machines: Definition and Role in Manufacturing
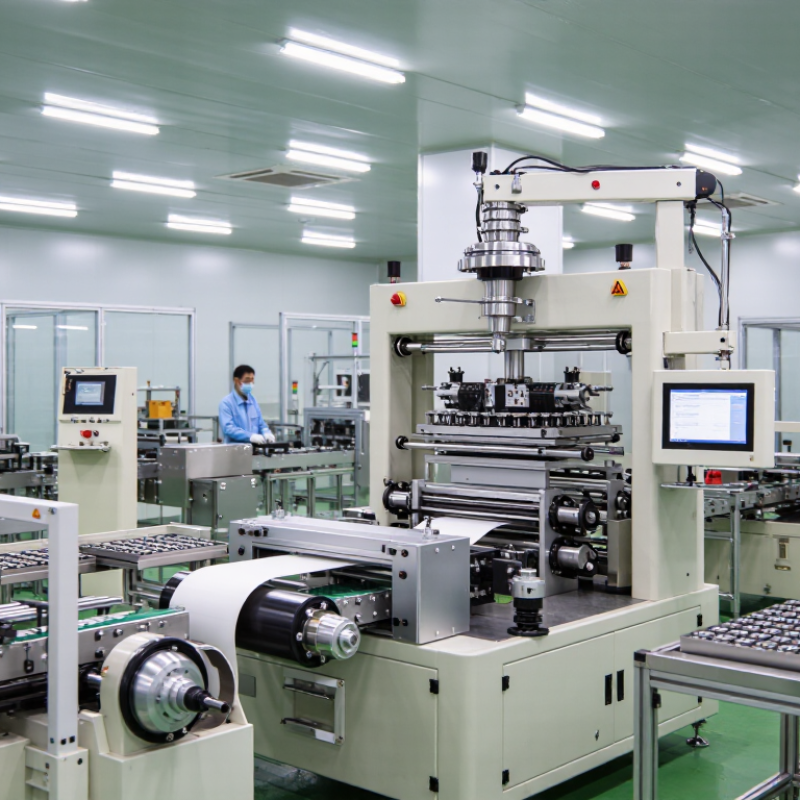
Cell assembly machines are systems used to build battery cells from prepared components. Depending on the cell design, they may handle stacking or winding, tab joining, enclosure placement, and sealing. Sensors and controlled motion help maintain repeatable positioning. A few millimeters can matter when layers must align closely. Small errors matter.
In manufacturing, these machines connect separate production steps and help control cycle time, handling, and process consistency. Operators still need to verify settings, inspect samples, and respond to alarms; automation does not guarantee a sound cell. Equipment choice depends on cell format, target output, available floor space, and the level of process monitoring required. A machine that suits one line may not suit another. That trade-off deserves honest review.
Tips: Compare equipment against your actual cell design and production plan. Ask how changeovers, routine cleaning, and fault recovery work. Check sample data from trial runs, not only the stated production rate. Keep records. A practical detail can be overlooked: operators need clear access to inspection points, even when the machine is running smoothly.
Major Types of Cell Assembly Machines Available Worldwide
Cell assembly machinery varies with cell format and production volume. Winding machines roll electrode and separator layers into a compact jelly roll, commonly used for cylindrical cells. Stacking machines place flat electrode sheets in alternating layers, a method often chosen for pouch and prismatic formats. Alignment matters: a small offset can affect the finished cell.
Other key equipment handles joining, filling, and enclosure. Tab welding machines connect electrode tabs to terminals, while shell insertion or pouch-forming machines prepare the outer case. Electrolyte filling systems meter liquid into each cell, sometimes under vacuum to help it penetrate the electrode layers. Sealing machines then close pouch edges or join rigid covers. Clean surfaces and controlled handling are important here. Tiny particles can cause trouble.
Inspection and handling systems may check dimensions, weld quality, leaks, and cell identification. Some lines also connect assembly stations with formation and aging equipment, though these are downstream processes rather than assembly itself. The choice is rarely neat. A fast machine may still create bottlenecks if changeovers take too long or operators struggle to access maintenance points. Buyers should compare cell format, target output, process tolerances, and service support, then verify performance using representative materials. A factory trial can reveal issues that a specification sheet misses.
Key Assembly Stages and Their Required Equipment
Cell assembly starts with electrode handling. Slitting and notching machines cut coated sheets to specified dimensions, while vision systems check edges for burrs or alignment errors. Winding or stacking equipment then builds the electrode assembly. Small defects matter. A misplaced layer can affect later sealing and performance, so operators should verify alignment rather than rely on machine settings alone.
Next, tab-welding equipment joins current collectors, and insertion systems place the assembly into its housing. Welding parameters need close control; excessive heat may damage nearby materials. Electrolyte filling machines often use vacuum cycles to help fluid reach narrow internal spaces. Dry-room conditions also matter, because moisture can compromise sensitive cell materials. The exact setup varies by cell format, and one line rarely fits every design.
Sealing machines close the housing, followed by formation equipment that charges and discharges cells under monitored conditions. Aging racks hold cells while voltage and temperature are tracked. Inspection tools can identify leaks, dimensional issues, or unusual electrical readings before shipment. Timing matters. In practice, equipment performance depends on process tuning, maintenance, and operator training. A machine’s rated speed is not the whole story; changeovers and rejected cells can quietly reduce useful output. Teams should review real production data and revise assumptions when results disagree.
How to Compare Machine Capabilities and Specifications
When comparing cell assembly machines, look beyond the advertised hourly output. Ask how that rate was measured: with which cell dimensions, process steps, and inspection settings? A line rated for 60 cells per minute may slow down when operators change formats or remove rejected parts. Check the supported cell size range, positioning tolerance, changeover time, and required operator involvement. Small details matter. A few seconds added at each station can affect an entire shift.
Tips: Request a sample production run using your actual materials. Record output, reject rate, and changeover time, then compare those results with the supplier’s stated figures. Review safety guarding, maintenance access, spare-part availability, and training needs. Ask for machine drawings and utility requirements before planning the floor layout.
Specifications are useful, but they rarely tell the whole story. Confirm how the machine detects misalignment, incomplete steps, or inconsistent bonding, and ask what data it stores for traceability. If possible, speak with technicians who operate similar equipment. Their feedback may reveal awkward cleaning points or frequent adjustments that a brochure omits. I would still treat any single test as limited evidence; longer runs can expose issues that a short demonstration misses.
Global Suppliers, Applications, and Purchasing Considerations
Cell assembly machines support winding, stacking, tab joining, sealing, and inspection for different battery cell formats. The right configuration depends on cell size, target output, and process sequence. Suppliers operate across major manufacturing regions, but local installation and spare-parts access can vary. Remote service matters when a line stops. Small details matter.
Before requesting quotes, define the cell format, planned production rate, and available factory conditions. Ask suppliers for sample-run results using materials similar to yours. Check changeover time, operator training, safety interlocks, and compatibility with dry-room requirements. Request clear acceptance criteria for alignment, sealing, and inspection performance. Numbers need context.
Purchasing decisions should weigh more than the machine price. Compare commissioning support, maintenance needs, lead times, and the availability of replacement parts in your region. Inspect reference installations where possible, and speak with operators about routine stoppages. No checklist catches every mismatch. A tidy proposal may still overlook a difficult material or a cramped production area, so leave room for a technical review before ordering.
Top Cell Assembly Machines for Sale Worldwide: Suppliers, Applications & Purchasing Considerations
Typical Pouch-Cell Assembly Workflow
Bars show ordinal process positions, not market share, output, or machine performance. This simplified workflow is typical of pouch-cell production; the sequence and equipment configuration vary by cell format and factory. When comparing machines, assess process compatibility, line interfaces, cleanliness controls, recipe traceability, and validated throughput.