Choosing among the Top 10 Zinc Die Cast Parts Suppliers for Global Buyers takes more than comparing unit prices. A bright sample on a desk can hide weak dimensional control, slow communication, or inconsistent production. Ask how each supplier manages alloy selection, die design, cycle time, and inspection. Request drawings, tolerance records, material details, and evidence of repeatable runs. Small details matter. A rough gate mark or a porous section can affect finishing, assembly, and service life.
Zinc-industry specialist Frank C. Goodwin offers a useful technical perspective. The following line is an editorial paraphrase, not a verified verbatim quotation: “Reliable castings begin with the right alloy, sound tooling, and disciplined process control.” Buyers should also compare finishing options, sampling procedures, production capacity, and shipment planning. A low quotation may leave out tooling changes or secondary operations. Check what the price actually includes. Then assess how clearly the supplier explains risks and corrective actions. This guide introduces ten suppliers and the questions worth asking before a sourcing decision. No supplier is perfect. Even strong factories can face capacity limits, design constraints, or communication gaps. A careful comparison helps buyers find a partner suited to their part, volume, and quality expectations—not merely the lowest offer.
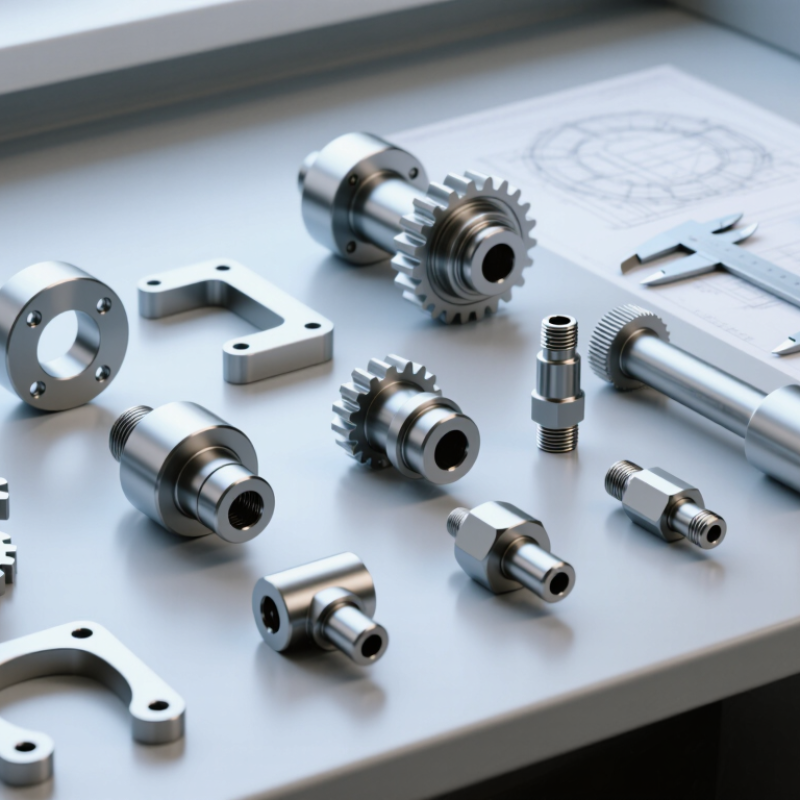
Zinc die casting combines a relatively low melting temperature with good fluidity, allowing molten metal to fill fine cavities and form thin walls. Common zinc alloys contain small amounts of aluminum and copper, adjusted for strength, hardness, and dimensional stability. The exact composition matters. A small change can affect how a part fills or wears.
Most zinc parts are made using hot-chamber die casting. A machine injects molten alloy into a hardened steel die under pressure, producing repeatable shapes with smooth surfaces. After ejection, operators trim gates and inspect critical dimensions. Tight tolerances are possible, but they should be confirmed against part geometry and production conditions. Tooling can also leave marks. That is not always a defect, though it may need attention on visible surfaces.
These parts often appear in door hardware, electrical connectors, appliance components, and small mechanical housings. Zinc suits intricate features such as ribs, bosses, and threaded details, reducing the need for separate machining. Designers should still check wall thickness, draft angles, and expected loads before approving a die. A thin section may cool unevenly. Testing real samples is useful, and sometimes the first design needs revision.
How to read this table: These are ten common supplier capability profiles, not named companies or a verified ranking. Capabilities vary by facility; confirm specifications, certifications, and production capacity directly with each prospective supplier.
| No. | Supplier Profile | Typical Materials & Process | Common Applications | Useful Buyer Checks |
|---|---|---|---|---|
| 1 | High-volume automotive component supplier | Zinc alloy pressure die casting, commonly using hot-chamber equipment for suitable zinc alloys; secondary machining may be available. | Interior mechanisms, housings, brackets, and small functional components. | Automotive quality-system certification, process traceability, dimensional capability data, and approval requirements for the intended vehicle program. |
| 2 | Electronics and electrical enclosure supplier | Zinc alloy die casting with options such as machining, conductive finishing, and surface coating, depending on the part design. | Connector bodies, shielding components, compact housings, and heat-dissipating parts. | Wall-thickness limits, shielding or conductivity requirements, finish compatibility, and inspection of critical interfaces. |
| 3 | Precision small-parts specialist | Hot-chamber zinc die casting is commonly used for small, repeatable parts; tooling and process design determine achievable detail and tolerances. | Fasteners, miniature levers, latches, and precision mechanical components. | Parting-line location, flash control, stated tolerance capability, sampling plan, and measurement methods. |
| 4 | Decorative hardware supplier | Zinc die casting followed, where required, by polishing, plating, painting, or other specified finishing operations. | Furniture fittings, architectural hardware, handles, knobs, and trim pieces. | Finish samples, coating specification, corrosion-test requirements, appearance standards, and protection during packing. |
| 5 | Tooling and production engineering supplier | Provides or coordinates die design, mold construction, casting trials, and production tooling for zinc alloy parts. | Custom components requiring dedicated dies, controlled geometry, or repeat production. | Tool ownership, maintenance responsibility, expected tool life assumptions, trial schedule, and change-control process. |
| 6 | Integrated casting and machining supplier | Combines die casting with CNC machining, tapping, drilling, or other secondary operations as specified. | Parts with accurately located holes, threads, flat faces, or assembly interfaces. | Datum strategy, machining allowances, fixture plan, burr removal, and inspection of cast-to-machined features. |
| 7 | Surface-finishing-focused supplier | Coordinates zinc casting with finishing processes such as plating, powder coating, or painting; suitability depends on alloy, geometry, and specification. | Visible consumer-product parts, decorative fittings, and components requiring specified surface protection. | Pre-treatment method, coating thickness or appearance criteria, adhesion testing, corrosion testing, and finish-subcontractor controls. |
| 8 | Industrial equipment component supplier | Zinc alloy die casting for shaped components, with optional machining and finishing based on service conditions. | Instrument housings, adjustment mechanisms, brackets, and small equipment components. | Load and environment requirements, alloy designation, dimensional inspection, and validation against the approved drawing. |
| 9 | Prototype and low-volume project supplier | May offer prototype tooling or production tooling for evaluation and smaller initial quantities; the available route depends on geometry and budget. | Design validation parts, pilot builds, and early-stage custom products. | Whether parts are made with production-intent tooling, sample quantity and lead time, material documentation, and the plan for scaling production. |
| 10 | Export-oriented contract manufacturer | May coordinate casting, secondary processing, finishing, inspection, and export packing through one production program. | Global OEM components across hardware, electronics, automotive, and general industrial markets. | Export documentation, packaging standard, production-site details, quality records, delivery terms, and responsibility for outsourced processes. |
A supplier’s sample part is only a starting point. Ask for alloy certificates, inspection plans, and results from recent production runs. The USGS Mineral Commodity Summaries 2025 estimates 2024 global zinc mine production at about 12 million metric tons. That scale does not guarantee stable supply, so check how suppliers trace ingots and manage material changes. Ask for records. For critical dimensions, request measurement data and the inspection method, not just a tolerance promise. NADCA’s Product Specification Standards for Die Castings provide a reference for dimensional tolerances and alloy requirements. Compare quotations against the same drawing and specification.
Tooling and process control deserve close scrutiny. Ask how the supplier monitors die temperature, injection settings, and tool wear across shifts. Request samples from a normal production run, not hand-selected parts. A polished sample can still mislead. Check thin ribs, threaded bosses, and sealing faces under magnification; these areas can reveal flash, porosity, or inconsistent fill. Ask whether X-ray or other internal checks are appropriate for your part’s function. Also review finishing capacity, packaging, and documented corrective actions. A supplier may have good equipment but weak records; that gap matters. Visit the production floor when possible, and compare what operators do with what the process documents say.
The ten supplier profiles reflect different strengths, not a simple ranking. An export-focused producer may offer multilingual support and established shipping routines. A high-volume automotive supplier often emphasizes repeatable cycles and process control. An electronics-focused shop may cast compact housings with thin walls. Plumbing specialists tend to prioritize pressure integrity and consistent surface finish. Details matter.
Other profiles include a precision-focused producer, an in-house tooling specialist, and a supplier with extensive machining capacity. The first may invest in tighter inspection; the second can coordinate die design and revisions. The third can deliver drilled, tapped, or milled components. A small-batch supplier may suit pilot runs, while a nearshore producer can shorten communication and transit times. An engineering-led supplier may help refine part geometry before tooling begins.
For global buyers, compare more than quoted price. Ask how each supplier controls alloy composition, porosity, dimensions, and sample approval. Request inspection records and clarify who handles finishing and packaging. Check capacity against your forecast, not only an attractive sample. A profile can look ideal on paper, yet tooling delays or unclear specifications may change the picture. Even careful screening cannot remove every risk. That part is easy to underestimate.
Zinc die-casting alloys are typically denser than aluminum and magnesium alloys. Density is one factor buyers may consider when comparing component weight and material options; actual values vary by alloy and specification.
Comparing Supplier Capabilities, Certifications, and Markets
Choosing among zinc die casting suppliers takes more than comparing quoted prices. Ask about machine capacity, tooling ownership, alloy options, and secondary processes such as tapping or plating. A capable supplier should explain how it controls porosity, dimensional variation, and surface finish. Request sample inspection reports, not just a polished product photo. A small housing with thin ribs can reveal more than a broad capability claim.
Certifications help buyers assess systems, but their scope matters. ISO 9001 can indicate established quality processes; automotive projects may require IATF 16949, while ISO 14001 addresses environmental management. Verify current certificates and confirm that the relevant production site is covered. Suppliers serving different markets may vary in export experience, local support, and familiarity with customer documentation. These differences can affect lead times and communication. Still, a certificate alone cannot guarantee consistent parts. That is easy to overlook.
Tips: Send a clear 2D drawing, 3D model, annual volume, and finish requirements when requesting quotes. Compare tooling costs and production assumptions alongside unit price. Ask how defects are tracked and corrected. One honest question: can the supplier show a recent example of a similar part?
Selecting an international zinc die casting supplier starts with a clear part brief. Specify the alloy, annual volume, critical dimensions, surface finish, and operating environment. A drawing alone may leave room for costly assumptions. Ask how the supplier controls die temperature, injection parameters, and trimming, since these can affect consistency and porosity. Request recent inspection records for comparable parts, not just a polished capability sheet.
Qualification should include sample parts made with production-intent tooling. Check critical dimensions against your drawing and discuss any defects, such as flash near a sealing face or uneven coating. Review the supplier’s inspection plan, material traceability, corrective-action process, and packaging method. A remote audit can reveal useful details, but it cannot show everything. One attractive sample is not proof of stable production; I would be cautious about treating it as such. Compare lead times and shipping arrangements, too, and agree on how changes will be approved.
Tips: Ask for measurable evidence. Confirm who owns the tooling and how maintenance is recorded. Keep questions in writing, with drawings and revision dates attached. Small details matter. If an answer is vague, ask for an example from a recent production run.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru