Zinc Die Casting supports compact, detailed components used in automotive systems, electronics, appliances, and hardware. A well-made zinc housing can show crisp ribs, clean edges, and consistent dimensions. Those details matter when parts must fit tightly on a production line. Still, choosing a supplier requires more than judging sample pieces.
The U.S. Geological Survey’s Mineral Commodity Summaries 2025 estimates global refined zinc production at about 14 million metric tons in 2024. This figure describes the wider supply base, not die-casting output. It offers useful context, but it cannot confirm a manufacturer’s capacity or material traceability. The North American Die Casting Association’s Product Specification Standards for Die Castings provide a more direct reference for alloy and casting requirements. Buyers should also examine tooling experience, inspection methods, finishing options, delivery performance, and support for design changes.
A polished website proves little. Factory audits, verified certifications, and customer references can reveal more. Even then, rankings have limits: a strong supplier for a small electrical connector may not suit a large automotive program. The manufacturers featured here are assessed through practical criteria, including process capability, product range, quality controls, and international reach. Treat the list as a starting point, not a substitute for checking samples, specifications, and production records.
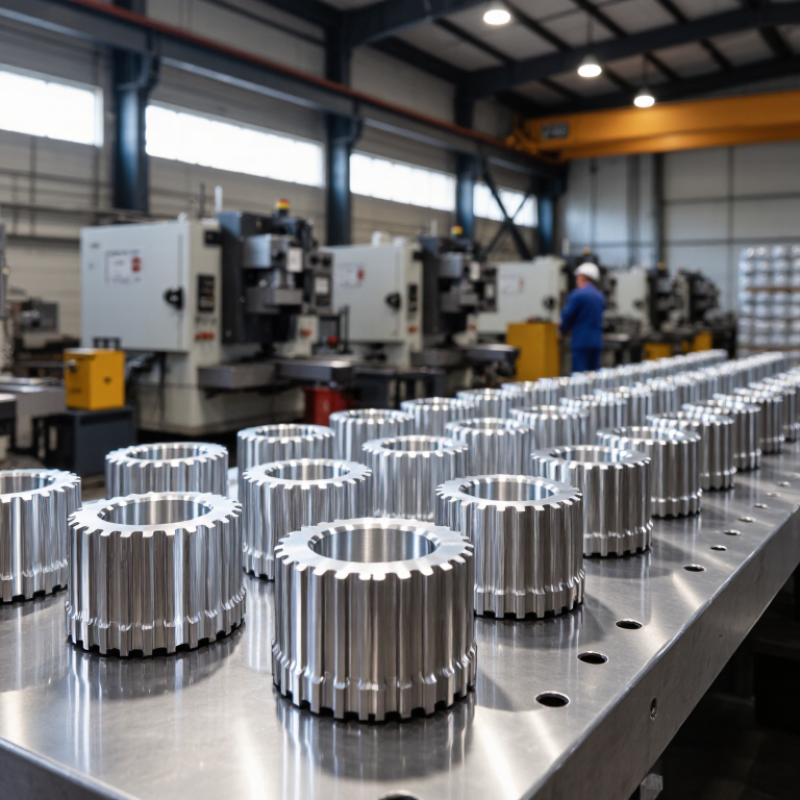
Zinc melts at 419.5°C in its pure form, a useful reference point for understanding zinc die casting. Commercial alloys do not necessarily melt at one exact temperature. Their composition affects melting behavior, flow, strength, and dimensional stability. That distinction matters. A production temperature should be set from alloy and process data, not from the pure-metal figure alone.
Common die-casting alloys include Zamak 3 and Zamak 5, along with higher-strength zinc alloys such as Zamak 2. Their exact properties vary, but they can fill fine cavities and reproduce details such as narrow ribs, small lettering, and smooth surface features. Zinc’s relatively low melting temperature can also reduce thermal load on dies compared with some higher-temperature metals. Still, temperature is only one part of the process. Die design, venting, lubricant, and cycle control all influence porosity and finish.
For a manufacturer, alloy choice starts with the part’s job. A thin decorative cover may prioritize surface quality and consistent dimensions, while a loaded bracket may need greater strength. Ask for the alloy specification, recommended processing range, and relevant test data. One point deserves a second look: higher strength does not automatically mean better performance if the design, corrosion exposure, or joining method is unsuitable.
Pure zinc melts at 419.5°C. The chart compares the approximate nominal aluminum content by mass of common zinc die-casting alloy families. Alloy composition affects properties and melting behavior, so aluminum content alone does not determine an alloy’s melting range.
A credible worldwide ranking should compare verified plant capacity, certification scope, served markets, and geographic footprint—not headline claims alone. Grand View Research valued the global die-casting market at about US$80.1 billion in 2023 and projected 6.4% annual growth through 2030. That figure covers die casting broadly, not zinc alone, so it signals market scale rather than proving any supplier’s zinc capacity. Capacity checks should record annual zinc-alloy output, machine tonnage, shift patterns, and available production lines. Ask for site-level figures. A large press does not guarantee dependable delivery.
Certifications should be checked against the specific plant and process, including current validity and audit scope. ISO 9001 supports quality-system comparison; automotive programs may also require sector-specific evidence. Market coverage matters too: automotive, electronics, hardware, and industrial customers can demand different tolerances and traceability. Plant locations affect freight distance, lead time, and supply resilience, but a map alone says little about backup capacity. The USGS Mineral Commodity Summaries 2024 estimated 2023 global zinc mine production at roughly 12 million metric tons. This is upstream context, not die-casting capacity. Rankings should separate the two. They can still miss practical differences, such as spare-tooling access or whether quoted capacity is already committed.
A worldwide comparison of zinc die casting manufacturers should begin with location, not a ranking alone. China and Taiwan have dense supplier networks, supporting high-volume production and in-house tooling. Japan and South Korea are known for tightly controlled processes and precision components. Location changes the equation.
In India, manufacturers often combine casting with machining and finishing, while European facilities in Germany, Italy, and Central Europe may focus on engineered parts and close customer coordination. North American suppliers, including those in the United States and Mexico, can offer regional production and shorter shipping routes for nearby buyers. Capabilities vary by plant. Ask about alloy control, die design, cycle consistency, and inspection methods rather than relying on broad claims.
A useful shortlist compares ten suppliers across regions, then checks their actual equipment and production records. Look for clear details: machine clamping capacity, part-size limits, secondary machining, surface finishing, and documented quality checks. Request sample parts and review measurement reports. No map is perfect. Freight costs, communication, and tooling ownership can change the best choice. I would not assume that a nearby factory is automatically the most reliable; verify process fit and production capacity before committing.
This table summarizes established zinc die-casting manufacturing regions rather than ranking or identifying individual companies. Capabilities listed are representative of the regional supply base and can vary by facility.
| No. | Manufacturing Region | Common Industrial Hubs | Representative Core Capabilities | Typical End Markets |
|---|---|---|---|---|
| 1 | China | Guangdong, Zhejiang, Jiangsu | Hot-chamber die casting, multi-cavity tooling, high-volume production, machining, plating, and assembly. | Electronics, automotive components, hardware, appliances, and consumer products. |
| 2 | Taiwan | Central and northern industrial areas | Precision zinc casting, close-tolerance components, toolmaking, secondary machining, and surface finishing. | Hardware, electrical equipment, automotive parts, and consumer devices. |
| 3 | South Korea | Gyeonggi, Incheon, and southeastern industrial areas | Precision production, automated casting operations, dimensional inspection, machining, and finishing. | Automotive systems, electronics, appliances, and industrial equipment. |
| 4 | Japan | Kanto, Chubu, and Kansai manufacturing areas | High-precision components, controlled-process manufacturing, tooling, surface treatment, and quality inspection. | Automotive, electrical equipment, precision instruments, and machinery. |
| 5 | India | Maharashtra, Gujarat, Tamil Nadu, and Karnataka | Hot-chamber casting, tooling and machining, batch-to-volume production, and component finishing. | Automotive, electrical products, locks and hardware, and general engineering. |
| 6 | Germany | Baden-Württemberg, Bavaria, and North Rhine-Westphalia | Engineering-led component development, precision casting, process monitoring, machining, and quality documentation. | Automotive, industrial machinery, electrical systems, and building hardware. |
| 7 | Italy | Lombardy, Veneto, and Emilia-Romagna | Custom tooling, precision zinc components, machining, decorative finishing, and integrated production services. | Furniture fittings, architectural hardware, automotive, and household products. |
| 8 | Spain | Catalonia, the Basque Country, and Valencia | Die casting for engineered components, tool maintenance, machining, surface finishing, and assembly. | Automotive supply chains, electrical equipment, hardware, and industrial products. |
| 9 | United States | Midwest and Great Lakes manufacturing areas | Custom die-casting programs, tooling support, machining, finishing, inspection, and domestic supply-chain integration. | Automotive, electrical and electronic equipment, plumbing, and industrial hardware. |
| 10 | Mexico | Nuevo León, Coahuila, Chihuahua, and central manufacturing corridors | Production for regional supply chains, hot-chamber casting, machining, finishing, and assembly. | Automotive, electrical equipment, appliances, and industrial components. |
Zinc’s density is about 7.14 g/cm³, giving small cast parts a solid feel while adding weight. That trade-off matters in handles, connectors, housings, and compact mechanisms. Zinc alloys can fill detailed die cavities, helping produce thin walls, sharp lettering, and consistent features at scale. A crisp edge is useful. But precision is not automatic: alloy selection, die temperature, venting, and tool wear all influence results. Compare stated tolerances with your actual drawing, rather than relying on broad claims.
For a worldwide manufacturer comparison, production capacity should be considered alongside dimensional control. Ask how parts are measured, how process variation is monitored, and whether sample parts match the intended production method. High output is valuable only when quality remains stable across runs. I would not treat density alone as a quality score; part geometry, required strength, and total assembly weight matter too. Some designs need another review.
Tips: Request a molded sample and a simple inspection report. Check wall thickness, critical dimensions, surface finish, and part weight. If a tolerance seems unusually tight, confirm it is necessary before tooling begins.
Zinc die castings suit compact parts that need fine detail, repeatable dimensions, and a smooth surface. Common applications include electrical enclosures, appliance hardware, and automotive interior components. When comparing suppliers, check whether their proposed alloy meets the relevant ASTM B86 requirements for your part. Ask for the exact alloy designation, not simply “zinc alloy.” Small details matter.
Evaluate quality using evidence from actual production. Request sample inspection reports, dimensional data for critical features, and information on how the supplier monitors porosity and surface defects. If parts need plating or painting, confirm that the process has been tested on the chosen alloy. Ask for evidence. A polished sample is useful, but it does not prove that every production run will match it.
Tips: Share a clear 2D drawing, 3D model, annual volume, and finish requirements before requesting a quote. Ask suppliers to separate tooling, sampling, and production lead times. Confirm how design changes affect timing. Compare their capacity against your forecast, and ask how delays are communicated. A spreadsheet helps, but it can hide uncertainty; estimates may shift after tooling trials. Leave room for that reality.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru