Overlay Welded Pipe is used to extend service life in pipelines exposed to corrosion, abrasion, heat, or a combination of these conditions. It consists of a base pipe with a metallurgically bonded alloy layer on its internal or external surface. The base material provides structural strength, while the overlay resists the specific damage expected during operation. This practical combination can reduce replacement frequency and material costs.
Common applications include oil and gas gathering lines, slurry pipelines, mining systems, power plants, cement facilities, and chemical processing equipment. For example, a pipe carrying sand-laden slurry may suffer severe internal wear near elbows and pump discharge points. A nickel-based or chromium-rich overlay can protect these high-risk areas, depending on the fluid chemistry and temperature. In corrosive service, stainless steel, nickel alloys, or other engineered materials may offer better protection than ordinary carbon steel.
The correct choice requires more than selecting a hard alloy. Engineers should review pressure, temperature, flow velocity, particle size, chemical composition, and expected maintenance access. Welding procedure qualification, dilution control, overlay thickness, and nondestructive testing also affect reliability. Small defects matter. Poor bonding or excessive heat input may create weak zones that remain hidden until service begins. Overlay Welded Pipe is not a universal solution, and its benefits can be overstated without field data. A sound specification should identify the damage mechanism, inspection method, and acceptance criteria before fabrication starts. Performance depends on details, including fit-up, surface preparation, and operating discipline.
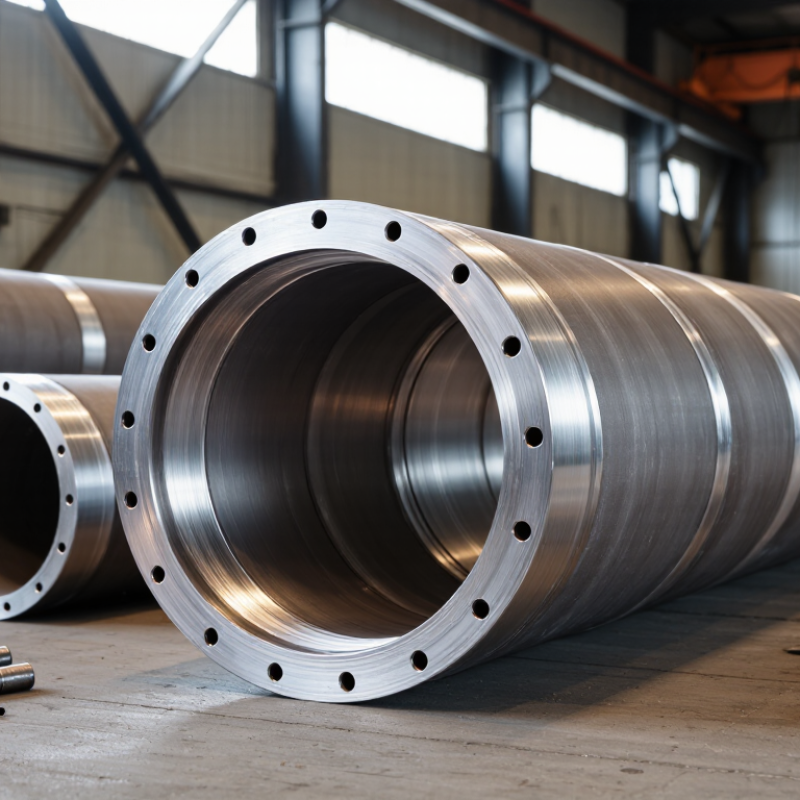
Overlay welded pipe is a composite pipe made from a structural base pipe and a welded alloy layer. The base pipe provides pressure strength, stiffness, and dimensional stability. The overlay protects the working surface from corrosion, erosion, or both. It acts like a durable skin over a load-bearing body. This definition separates structural duty from surface protection.
During production, welding equipment deposits alloy beads onto the base pipe. Several passes may build the required thickness. Heat changes the nearby base metal, creating a heat-affected zone. A sound overlay needs strong metallurgical bonding, controlled dilution, and consistent coverage. The inner surface should remain reasonably smooth for fluid flow and cleaning. Pipe ends may require special treatment because cutting can expose the base material. Quality checks commonly include visual examination, dimensional measurement, and ultrasonic testing. These checks reveal gaps, excessive waviness, or weak bonding.
This structure suits pipelines carrying abrasive slurry, corrosive chemicals, heated fluids, or process gases. It can extend service life where replacing a complete solid-alloy pipe would be impractical. Designers still match the overlay alloy to temperature, chemistry, flow speed, and pressure. The design is not perfect. More alloy is not automatically safer. Too much thickness can increase cost, residual stress, and fabrication difficulty. Field failures sometimes begin with poor surface preparation or overlooked weld defects. That is why installation records and independent inspection deserve attention.
What Is Overlay Welded Pipe Used For?
How Overlay Welding Improves Pipe Performance
Overlay welded pipe is used where ordinary steel faces corrosion, abrasion, or high-temperature damage. Common applications include oil and gas gathering lines, chemical processing, power generation, mining slurry systems, and water-treatment equipment. A corrosion-resistant or wear-resistant alloy is welded onto the pipe’s internal surface. The carbon-steel base provides strength, while the overlay forms a protective working layer.
This design can reduce wall loss from sour fluids, chlorides, acids, sand, and high-velocity flow. Welding methods include submerged arc, plasma transferred arc, and laser cladding. Each method controls dilution, thickness, and heat input differently. Poor control can create cracks or weak bonding. That detail is often underestimated.
The NACE IMPACT study estimated global corrosion costs at about $2.5 trillion annually, equal to 3.4% of global gross domestic product. It also reported that effective corrosion management could save 15% to 35% of those costs. Overlay welding supports this goal by extending service intervals and reducing replacement work. However, it is not a universal fix. Engineers must match alloy chemistry, operating temperature, pressure, and fluid composition. Inspection remains essential, especially around weld starts, bends, and internal defects. In practice, a slightly thicker overlay may improve durability, but it can also increase distortion and fabrication cost. That trade-off deserves careful review.
Overlay welding is used on oil and gas lines, slurry pipelines, mining equipment, chemical-process piping, boiler tubes, and valve sealing surfaces. The chart shows representative hardness ranges for common overlay weld deposits: higher hardness generally improves resistance to abrasion and erosion, while nickel- and cobalt-based overlays are selected mainly for corrosion, heat, and metal-to-metal wear resistance. Actual values vary with alloy chemistry, welding process, dilution, and heat treatment.
What Is Overlay Welded Pipe Used For?
Industries and Applications of Overlay Welded Pipe
Overlay welded pipe combines a strong carbon steel base with a corrosion-resistant alloy surface. The overlay is deposited by welding, creating a durable working layer. This design can reduce material costs while protecting the pipe from aggressive service conditions.
In oil and gas facilities, it carries fluids containing water, carbon dioxide, chlorides, or hydrogen sulfide. Operators use it in gathering lines, risers, manifolds, and process piping. Refineries also apply overlay pipe around elbows and flow sections, where erosion and corrosion often accelerate. Chemical plants use it for acids, solvents, and heated process streams, but compatibility must be verified carefully.
It also serves power generation, desalination, mining, and pulp production. Slurry pipelines benefit from abrasion-resistant overlays when sand or mineral particles strike the internal wall. Desalination systems may use corrosion-resistant layers near seawater intake and treatment equipment. In power plants, overlay pipe can support demanding steam and cooling-water applications.
The details matter.
Engineers should check alloy chemistry, weld dilution, overlay thickness, hardness, and inspection records. Poor fusion or uneven coverage can create weak areas beneath an attractive surface. Temperature cycling can expose problems that pressure testing misses. From field experience, overlay pipe is not a universal fix. A cheaper base material may lower the initial price, yet incorrect alloy selection can cause early failure. Service history, fluid analysis, and realistic inspection planning should guide every specification.
What Is Overlay Welded Pipe Used For?
Common Materials Used for Pipe Overlay Welding
Overlay welded pipe combines a strong base pipe with a corrosion-resistant or wear-resistant surface. It is used in chemical processing, oil and gas, power generation, mining, and water treatment. The base pipe usually contains carbon steel because it offers strength and reasonable cost. The overlay protects the inner surface from aggressive fluids, heat, particles, or repeated pressure changes.
Stainless steel is a common overlay material. Grades similar to 316L resist chlorides, moisture, and many chemical solutions. Austenitic alloys such as 309L can support transition layers between carbon steel and stainless surfaces. Nickel-based alloys, including chromium-nickel compositions, handle severe corrosion and high temperatures. They are often selected for acidic media, but they require careful heat control. Hardfacing alloys containing chromium and carbide particles are useful when sand, ash, or mineral solids cause abrasion. They resist wear rather than chemical attack.
Material selection depends on the service environment, not only the alloy name. In practical fabrication, engineers check temperature, pressure, fluid chemistry, flow speed, and expected wear. Dilution is easy to underestimate. Base metal can mix into the overlay and reduce its intended performance. Welding procedure qualification, hardness testing, chemical analysis, and visual inspection help control that risk. A perfect choice on paper may still fail after poor surface preparation or excessive heat input. The selection process deserves a second review.
| Overlay Material | Typical Pipe Substrate | Primary Protection | Common Applications | Common Welding Processes | Typical Service Conditions |
|---|---|---|---|---|---|
| Stainless steel 309/309L or 312 | Carbon steel and low-alloy steel | General corrosion resistance and a transition layer between dissimilar steels | Chemical processing lines, thermal equipment, repair welds, and pipe fittings | GTAW, GMAW, SMAW, and SAW | Moderate corrosion and elevated-temperature service |
| Stainless steel 316L | Carbon steel, low-alloy steel, or stainless steel | Resistance to chlorides, moisture, and many chemical environments | Water treatment, chemical piping, food-processing utilities, and marine-related systems | GTAW, GMAW, SMAW, and SAW | Wet service and chloride-containing environments; exact suitability depends on concentration and temperature |
| Duplex stainless steel | Carbon steel, low-alloy steel, or compatible stainless steel | High resistance to chloride stress-corrosion cracking and pitting, with good strength | Desalination, offshore piping, chemical processing, and produced-water systems | GTAW, GMAW, FCAW, and SAW with controlled heat input | Chloride-bearing water and moderately aggressive process fluids |
| Nickel-chromium-molybdenum alloy | Carbon steel, low-alloy steel, or stainless steel | Severe resistance to pitting, crevice corrosion, and reducing or oxidizing chemicals | Flue-gas treatment, acid processing, waste treatment, and highly corrosive chemical lines | GTAW, GMAW, FCAW, SMAW, and PTA | Severe chemical exposure; alloy selection must match the process chemistry |
| Nickel-copper alloy | Carbon steel and low-alloy steel | Resistance to seawater, hydrofluoric acid, and selected saltwater environments | Marine piping, seawater systems, heat exchangers, and chemical transfer lines | GTAW, GMAW, SMAW, and PTA | Seawater and selected acidic services; galvanic compatibility must be evaluated |
| Cobalt-based wear alloy | Carbon steel, stainless steel, and heat-resistant steel | Metal-to-metal wear, galling, erosion, and high-temperature wear | Valves, elbows, pump components, furnace piping, and high-wear process sections | GTAW, PTA, laser cladding, and GMAW | High-temperature sliding or impact wear; final hardness depends on alloy grade and dilution |
| Iron-based chromium carbide overlay | Carbon steel and abrasion-resistant steel | Severe abrasive wear caused by hard mineral particles | Mining slurry lines, cement systems, ash handling, dredging, and mineral processing | SAW, FCAW, SMAW, and open-arc welding | Dry or wet abrasion; generally less suitable for high-impact or highly corrosive service |
| Nickel-based wear-resistant alloy | Carbon steel, stainless steel, and nickel-alloy pipe | Combined corrosion, erosion, cavitation, and moderate wear | Oil and gas production, slurry transport, chemical pumps, and corrosive flow lines | GTAW, GMAW, FCAW, PTA, and laser cladding | Corrosive fluids containing suspended solids; service limits depend on alloy composition |
| Aluminum-bronze or nickel-aluminum bronze | Carbon steel and compatible copper-based components | Seawater corrosion, cavitation, and selected erosion mechanisms | Marine piping, seawater pumps, valves, shipboard systems, and hydraulic equipment | GTAW, GMAW, and SMAW | Marine and saltwater service; joint design and dilution control are important |
Note: Actual overlay selection depends on the fluid chemistry, temperature, pressure, flow velocity, wear mechanism, substrate compatibility, required thickness, and applicable welding procedure qualification.
Overlay welded pipe protects a carbon-steel or alloy-steel base from aggressive service. It is used in oil and gas gathering lines, chemical plants, power facilities, and mining slurry systems. The overlay typically contains corrosion-resistant alloy, stainless steel, or wear-resistant material. It provides a protective working surface while retaining the substrate’s structural strength.
Selection should begin with the actual damage mechanism. Will the pipe face hydrogen sulfide, chlorides, acids, high temperature, or abrasive particles? The NACE IMPACT study estimated global corrosion costs at about $2.5 trillion annually, equal to roughly 3.4% of global GDP. That figure supports careful material selection, not automatic use of thicker steel. Chemistry matters.
Operating pressure and temperature come next. Engineers should verify hardness, dilution, weld integrity, and resistance to thermal cycling. API 5LD provides requirements for corrosion-resistant alloy lined and lined steel pipe. ASTM G65 testing can help compare abrasive wear performance. Non-destructive examination is also important, especially ultrasonic testing around weld boundaries.
A practical choice balances cost, repairability, and service life. I would not select overlay pipe from a datasheet alone. Field dust, misalignment, and imperfect welding can change performance. That uncomfortable detail is often overlooked. A cheaper overlay may fail sooner if the process chemistry was estimated poorly. Maintenance records, inspection history, and representative laboratory testing should influence the final decision.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru