Tape Applicators are practical machines that place adhesive tape accurately, repeatedly, and at controlled speed. They appear in carton sealing, product bundling, cable assembly, labeling, and protective packaging. A typical unit includes a tape roll, tension control, guide rollers, a cutting blade, and an application head. The machine feeds the tape across a surface, presses it firmly, and cuts it at a programmed length. Some models use sensors to detect package position. Others depend on timed movement or operator control.
Industry reports show why this equipment matters. Smithers’ The Future of Packaging: Long-Term Strategic Forecast to 2028 identifies e-commerce, labor efficiency, and packaging optimization as continuing market drivers. The World Packaging Organisation’s Global Packaging Trends Report also highlights automation and material efficiency as important operational priorities. Packaging machinery estimates from PMMI and other market analysts vary because their definitions differ. That variation deserves attention. Still, the direction is clear: manufacturers want consistent sealing with less waste and fewer interruptions.
In practice, performance depends on more than speed. A dusty carton can weaken adhesion. Excessive tension can stretch thin tape. A misaligned roller may create wrinkles, exposed edges, or incomplete seals. Experienced technicians therefore match the applicator with tape width, backing material, surface texture, package dimensions, and production volume. The best system is not always the fastest one. It is the one that delivers repeatable results under real factory conditions. This guide explains how Tape Applicators work, what their main components do, and where careful setup can prevent costly mistakes.
What Are Tape Applicators and How Do They Work?
Tape applicators place adhesive tape onto products, packages, panels, or continuous materials. They control tape tension, guide the roll, and press the adhesive onto a surface. A cutting or dispensing mechanism may follow, depending on the application.
The most useful way to define an applicator is by web width. Web width means the maximum tape width the machine can handle. A narrow web suits labels, edge sealing, and small packages. Wider webs support panel joints, protective films, and industrial wrapping. Measure the actual tape width, not only the product width. A few extra millimeters can affect tracking.
Core size describes the hole inside the tape roll. The applicator spindle must match that core or use a secure adapter. Common core dimensions vary by equipment and roll type. Roll diameter defines the outside size of the wound tape. A larger diameter reduces roll changes, but it also adds weight and inertia. The machine must support both safely. Practical checks matter.
In setup work, I have seen operators focus on width and overlook diameter. That mistake can cause slipping, uneven tension, or poor adhesion. Core adapters may solve one issue while creating another. They can introduce wobble if fitted loosely. The best selection compares all three measurements with the machine’s tension range and pressure settings. Even experienced users should verify the roll path before production. Small differences matter.
| Applicator Type | Typical Web Width | Compatible Core Size | Typical Maximum Roll Diameter | How It Works | Common Applications |
|---|---|---|---|---|---|
| Handheld Pressure-Sensitive Tape Applicator | 25–100 mm (1–4 in) | 76 mm (3 in) | 150–200 mm (6–8 in) | A hand-operated roller presses adhesive tape onto a surface while a cutting blade separates the applied section. | Carton sealing, bundling, labeling, and general packaging work. |
| Bench-Top Tape Dispenser | 6–150 mm (0.25–6 in) | 25 or 76 mm (1 or 3 in) | 150–300 mm (6–12 in) | The roll is mounted on a fixed spindle, and the operator pulls tape across a guided feed path and cutting edge. | Assembly stations, component packaging, office use, and small-batch production. |
| Pneumatic Tape Applicator | 12–100 mm (0.5–4 in) | 76 mm (3 in) | 200–400 mm (8–16 in) | Compressed air drives the feed or application mechanism, providing repeatable tape placement and pressure. | High-volume packaging, insulation placement, and industrial assembly lines. |
| Automatic Web Tape Applicator | 25–300 mm (1–12 in) | 76 mm (3 in) | 300–600 mm (12–24 in) | Powered rollers unwind, position, and press the tape onto a moving product or web with limited operator input. | Continuous converting, packaging machinery, printed materials, and product assembly. |
| Double-Sided Tape Laminator | 25–1,500 mm (1–59 in) | 76 or 152 mm (3 or 6 in) | 300–800 mm (12–31.5 in) | A nip roller bonds adhesive tape to a substrate while a liner is removed or rewound during lamination. | Foam bonding, signage, labels, gaskets, insulation, and composite materials. |
| Transfer-Tape Applicator | 6–300 mm (0.25–12 in) | 25, 76, or 152 mm (1, 3, or 6 in) | 200–600 mm (8–24 in) | Transfers a pressure-sensitive adhesive layer from a release liner to a surface using controlled nip pressure. | Paper converting, label production, graphics, electronics, and thin-material bonding. |
| Strapping Tape Applicator | 12–50 mm (0.5–2 in) | 76 mm (3 in) | 200–400 mm (8–16 in) | A tensioned roller applies reinforced or filament tape around a package, while a cutter trims the strap. | Pallet stabilization, bundling, appliance packaging, and heavy-duty carton closure. |
| Narrow-Web Label Tape Applicator | 10–100 mm (0.4–4 in) | 25 or 76 mm (1 or 3 in) | 150–300 mm (6–12 in) | A peel plate or applicator roller separates the label or adhesive strip from its liner and applies it at a controlled position. | Product identification, barcode labeling, price marking, and small-package decoration. |
| Wide-Web Industrial Applicator | 300–2,000 mm (12–79 in) | 76 or 152 mm (3 or 6 in) | 600–1,000 mm (24–39 in) | Large unwind and pressure-roll assemblies apply a continuous adhesive web across wide sheets or rolls. | Furniture panels, insulation boards, flooring, laminates, and large-format converting. |
Note: The dimensions shown are common industrial ranges rather than universal limits. Actual capacity depends on tape thickness, adhesive type, liner material, machine configuration, and required application speed.
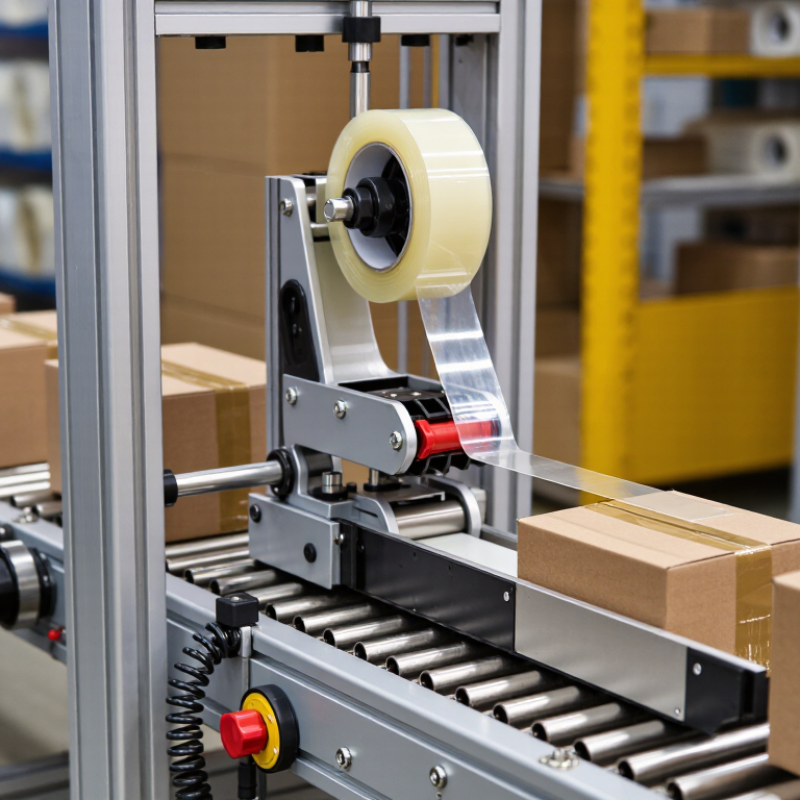
Tape applicators are mechanical systems that place adhesive tape accurately and consistently. Their work follows a clear application cycle: unwind, tension, press, cut, and release. Each stage affects the next one, so a small adjustment can change the final bond.
During unwinding, the supply roll feeds tape toward the application head. The unwind brake prevents sudden acceleration and loose loops. Tension rollers then keep the tape straight without stretching its backing. Excessive tension may narrow the tape or weaken its adhesive contact. Too little tension can create wrinkles, slack, or uneven placement. I usually check the roll edge and path before production begins.
Next, a pressure roller presses the tape against the surface. Pressure should be firm, not crushing. The surface must also be clean, dry, and suitable for adhesion. After the target length passes, a knife or shear mechanism cuts the tape. The cut should be clean and square. A rough edge often signals poor blade alignment or incorrect tension. The release stage separates the applicator from the applied tape without lifting its edge. This requires controlled movement and the right peel angle.
Small mistakes become visible quickly. A misaligned roller can shift the entire strip. No setting works everywhere. Material thickness, temperature, speed, and surface texture all matter. In practice, operators often improve results by recording adjustments and checking bond quality at regular intervals. I still recheck the first few applications, because stable-looking equipment can produce inconsistent tape placement.
Tape applicators place pressure-sensitive tape on cartons, bundles, or protective materials. Manual models rely on an operator’s hand pressure and alignment. They suit short runs, changing carton sizes, and workstations with limited space. An experienced operator may seal 10 to 20 cartons per minute, but fatigue can reduce consistency.
Automated applicators use sensors, drive rollers, and programmed controls. Many production units reach 30 to 60 cartons per minute, depending on tape width, carton size, and line layout. PMMI’s 2023 Automation Solutions for Packaging and Processing report identifies labor availability and productivity as major automation drivers. This supports automated adoption, but speed alone is not enough. A poorly adjusted machine can waste tape quickly.
Accuracy usually favors automation. Controlled tension and fixed placement can keep tape centered within a few millimeters. Manual application may vary by operator, especially during long shifts. MHI’s 2024 Annual Industry Report states that 55% of supply-chain professionals planned to increase investment in automation, reflecting pressure to improve reliable output. Duty cycle also matters. Manual tools can manage intermittent work, while automated systems are built for extended cycles and higher daily volumes. Still, maintenance, sensor cleaning, and changeover time must be counted. Real plants are messier. A smaller automated unit may lose its advantage when products change every few minutes. For stable, repetitive packaging, however, its accuracy and endurance are difficult to match.
Tape applicators control how adhesive tape meets a surface. Their rollers apply pressure while guiding tape at a steady angle and speed. Pressure matters. Insufficient force leaves air pockets, weak contact, and visible edge lifting. Excessive force can stretch foam tape or distort thin films. The Pressure Sensitive Tape Council’s technical guidance emphasizes firm, uniform application rather than a single maximum force value. In practice, operators should verify pressure with a controlled roller and record the setting.
Dwell time is the period between application and loading. Many pressure-sensitive adhesives build strength gradually after contact. ASTM D3330 measures peel adhesion under controlled conditions, while ASTM D3654 evaluates holding power over time. These methods show why immediate testing can misrepresent real performance. A practical trial might compare one-minute, one-hour, and twenty-four-hour dwell periods. The result can change sharply. Temperature also affects flow and wet-out. Below the adhesive’s recommended range, the tape may feel stiff and bond poorly. Excessive heat can soften the adhesive and increase residue risk. A 2024 market analysis from Grand View Research identifies pressure-sensitive tapes as a growing industrial materials segment, increasing the need for repeatable process controls.
Peel angle and speed complete the setting. Pulling slowly at 180 degrees usually produces different readings than a fast, shallow peel. The exact angle must match the test method. Surface dust, moisture, and release coatings can overwhelm carefully selected settings. That is easy to underestimate. Record substrate condition, roller passes, temperature, dwell time, and peel speed for every trial. I would not trust one successful sample; production variation deserves a second test.
What Are Tape Applicators and How Do They Work?
Tape applicators guide adhesive tape onto a surface with controlled pressure and alignment. A roller presses the tape while the cutting system creates a clean edge. Performance depends on pressure, speed, surface energy, and operator handling. Small positioning errors can leave visible gaps or uneven overlaps. That is why ±1 mm placement checks matter during production.
ASTM D3330 provides standardized peel-test methods for pressure-sensitive tapes. Common 180-degree tests use a controlled peel angle and speed, often 300 mm per minute. Results should record tape width, backing, dwell time, temperature, and peel force. The Pressure Sensitive Tape Council also emphasizes conditioning and repeatable preparation. Without these controls, two tests may appear comparable but are not. A practical inspection combines a calibrated ruler, digital gauge, or vision system. Measure the tape edge at several points, not only one. I have seen clean-looking applications fail near corners.
Tips: Mark a fixed reference line before testing. Check ±1 mm placement after every setup change. Keep samples conditioned. Do not trust one peel value. Three to five specimens provide a more useful view, although production decisions may require a larger sample. ASTM D3330 is a test method, not a guarantee of field performance. Real surfaces remain imperfect. That detail deserves attention.
The chart shows example test-run results for a pressure-sensitive tape applicator. Peel adhesion is reported in N/25 mm using an ASTM D3330-style 180° peel measurement, while placement accuracy is shown as absolute deviation from the target line. The dashed threshold represents the ±1 mm placement requirement.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru