A Filter Materials Lamination Machine bonds filter layers into a stable, functional composite. It may combine nonwoven fabric, melt-blown media, wire mesh, film, or support paper. The machine controls pressure, heat, adhesive application, and web tension. These variables shape filtration performance and production consistency.
In practical manufacturing, operators watch the material as it passes between heated rollers. A slight wrinkle can affect sealing, airflow, or pleat formation. Reliable machines often include tension controls, temperature sensors, alignment systems, and adjustable lamination speeds. However, automation does not remove every risk. Incorrect settings may damage delicate fibers or create uneven bonding. This is where process knowledge matters.
Good equipment selection begins with the filter design. Engineers should review material thickness, thermal sensitivity, adhesive compatibility, line speed, and required bond strength. Testing should include peel strength, air permeability, dimensional stability, and visual inspection. Supplier data is useful, but it should not replace production trials. Real materials behave differently.
Small details matter.
A clear operating record can reveal problems early. It can also support repeatable quality checks across different batches. This guide explains how a Filter Materials Lamination Machine works, where it fits in filter production, and which specifications deserve careful attention. Some applications may need customized rollers, cleaning systems, or curing stages. The best solution is not always the fastest one. Reliability, maintainability, and verified performance should guide the final decision.
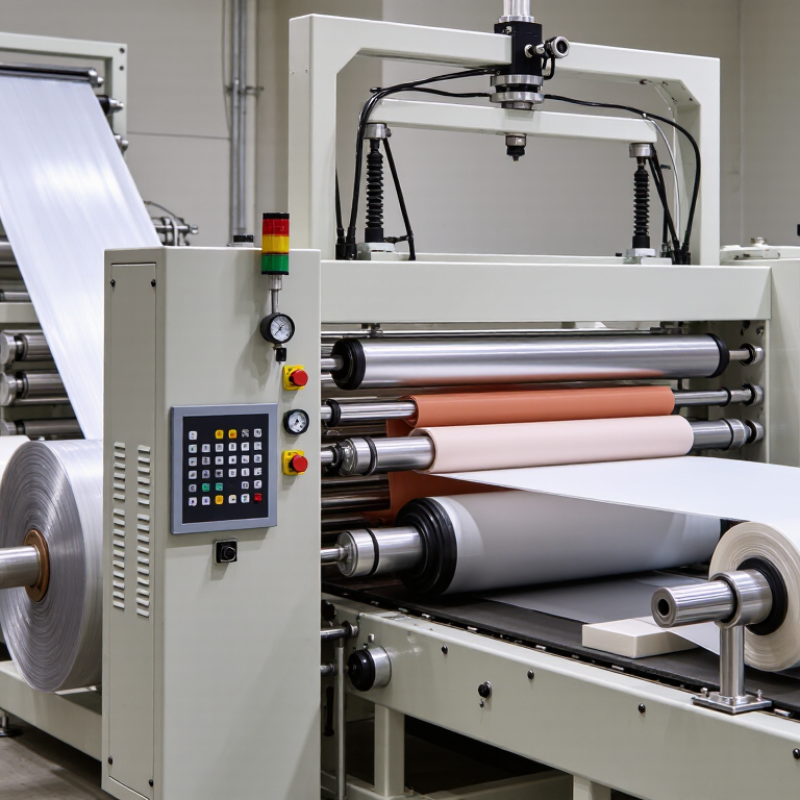
A filter materials lamination machine is industrial equipment designed to bond multiple filter layers into one functional structure. It joins media, support fabrics, meshes, or protective films with controlled heat, pressure, or adhesive. The core purpose is to create a stable composite without damaging the filter’s pores. This structure can improve handling, durability, and resistance to separation during installation or use.
In a typical line, separate rolls unwind at a controlled speed. Tension systems keep each layer flat and aligned. Heated rollers, pressure rollers, or adhesive coating units then combine the materials. Operators monitor temperature, line speed, nip pressure, and adhesive coverage. Small adjustments can change the final result. This is where experience matters.
A reliable lamination process must protect airflow, filtration efficiency, and mechanical strength. The bonded material should not wrinkle, peel, or seal important pores. Technicians usually inspect samples and test peel strength, thickness, and visual uniformity. Practical trials often reveal problems that specifications miss. The process is not flawless. An apparently smooth surface can still hide weak bonding. Humidity, coating weight, and roll alignment may shift performance. For this reason, careful records and measured adjustments remain essential when setting up production.
| Dimension | Definition or Function | Typical Technical Information | Practical Importance |
|---|---|---|---|
| Equipment Definition | A filter materials lamination machine is industrial equipment that bonds two or more layers of filter media, support materials, films, meshes, or nonwoven fabrics into a composite structure. | The machine may use heat, pressure-sensitive adhesive, hot-melt adhesive, ultrasonic energy, or other controlled bonding methods. | It creates a multilayer filter material with more stable handling, improved strength, and controlled functional performance. |
| Core Purpose | The primary purpose is to join separate material layers continuously and uniformly while preserving the required filtration, airflow, and structural properties. | Key controls generally include web tension, bonding pressure, temperature, line speed, adhesive application, and material alignment. | Consistent lamination helps reduce delamination, wrinkles, weak bonds, and variations in finished filter quality. |
| Common Input Materials | Input materials can include melt-blown media, spunbond nonwovens, needle-punched fabrics, filtration paper, synthetic membranes, woven meshes, and protective films. | Materials are commonly supplied in rolls and may differ in thickness, porosity, basis weight, surface energy, and heat sensitivity. | Material compatibility determines the suitable bonding method and operating window. |
| Typical Product Structures | Laminated products may contain a filtration layer combined with a support layer, pre-filter layer, scrim, membrane, drainage layer, or protective facing. | Examples include two-layer, three-layer, and multilayer constructions used in air, liquid, medical, industrial, and automotive filtration. | Layer selection allows a product to combine filtration efficiency, mechanical support, protection, and processability. |
| Bonding Methods | Bonding can be achieved through thermal calendering, hot-melt adhesive coating, powder or web adhesive, flame lamination, ultrasonic bonding, or pressure-sensitive adhesive systems. | Thermal methods require controlled heat and nip pressure; adhesive methods additionally require coating-weight and curing or cooling control. | The method affects bond strength, flexibility, air permeability, chemical resistance, and the risk of blocking or media damage. |
| Feeding and Web Handling | Roll-to-roll feeding systems guide, unwind, align, and combine continuous material webs before bonding. | Typical features include unwind stands, tension controllers, edge guides, splice handling, web guides, and synchronized drive systems. | Stable web handling helps maintain layer registration and prevents stretching or creasing of delicate filter media. |
| Temperature Control | Temperature control is used when the bonding process depends on heat activation, melting, softening, or drying. | Heated rollers, hot-air zones, infrared heaters, or heated platens may be used, depending on the process design. | Accurate temperature control supports repeatable bonding while limiting thermal shrinkage, melting, odor, or deformation. |
| Pressure and Nip Control | Nip pressure brings the layers into contact and helps distribute heat or adhesive across the bonding area. | Pressure may be adjusted mechanically, hydraulically, or pneumatically; the correct setting depends on material thickness and compressibility. | Proper pressure improves bond uniformity without excessively compressing pores or reducing airflow. |
| Line Speed | Line speed is the rate at which the material web passes through the lamination zone. | Speed is normally expressed in metres per minute and must be balanced with heating, adhesive setting time, pressure, and web tension. | Higher speed can increase output, but inadequate process energy or residence time may reduce bonding quality. |
| Adhesive Application | When adhesive lamination is used, the machine applies a controlled amount of adhesive between selected layers. | Application formats may include dots, lines, spray patterns, grids, films, powders, or full-surface coatings. | A controlled pattern preserves flexibility and air permeability while providing sufficient bond coverage. |
| Quality Control Parameters | Quality checks evaluate whether the laminated material meets required structural and filtration-related specifications. | Common checks include peel or bond strength, thickness, basis weight, width, appearance, air permeability, pressure drop, and layer alignment. | Monitoring these parameters helps identify process drift and supports stable downstream converting and assembly. |
| Filtration Performance Considerations | The lamination process must maintain the functional properties of the filter media rather than obstructing or damaging the active filtration layer. | Important factors include pore structure, air or liquid permeability, pressure drop, filtration efficiency, and resistance to the intended operating environment. | Excessive adhesive, heat, or compression can reduce permeability or alter the designed filtration performance. |
| Automation and Monitoring | Modern systems may use sensors and control units to regulate tension, temperature, pressure, speed, adhesive delivery, and web position. | Monitoring may include digital recipe control, alarm systems, closed-loop tension control, and production data recording. | Automation improves repeatability, reduces operator-dependent variation, and supports faster changeovers. |
| Typical Applications | Laminated filter materials are used in air filtration, liquid filtration, dust collection, respiratory protection, cleanroom products, automotive systems, and industrial process filtration. | The final material may be converted into cartridges, panels, bags, masks, pleated elements, or other filter assemblies. | Different applications require different combinations of filtration efficiency, strength, chemical resistance, and permeability. |
| Main Benefits | Lamination can improve dimensional stability, tear resistance, handling strength, layer protection, and product integration. | Benefits depend on the selected materials and bonding process; lamination does not automatically improve every filtration characteristic. | The process enables engineered multilayer media designed for specific performance and manufacturing requirements. |
| Operational Safety | Operators must manage moving webs, heated surfaces, nip points, adhesive systems, and electrical or pneumatic components. | Important safeguards include guarding, emergency stops, temperature protection, ventilation where required, and lockout procedures for maintenance. | Proper safety controls reduce the risk of burns, entanglement, exposure, and equipment-related injuries. |
A filter materials lamination machine bonds two or more layers into a stable composite. Common layers include nonwoven fabric, melt-blown media, support mesh, and breathable films. The main components usually include unwinding units, tension controllers, an adhesive or thermal bonding system, laminating rollers, sensors, and a rewinding unit. Each part affects product consistency. A small tension error can create wrinkles, loose edges, or uneven airflow.
The process begins as the machine unwinds each material at a controlled speed. Tension sensors help keep the layers aligned. Depending on the material, the bonding system applies hot-melt adhesive, heat, or pressure. Nip rollers then compress the layers evenly. Cooling rollers may stabilize the bond before the composite reaches the rewinder. Operators should check temperature, pressure, line speed, and adhesive coverage together. Adjusting only one setting can hide the real cause of a defect. A technically correct setup may still perform poorly when humidity or material thickness changes.
Tips: Keep the web path clean and inspect rollers before production. Use sample strips to check bond strength, flatness, and layer alignment. Record every adjustment. This makes troubleshooting more reliable. Do not assume higher pressure creates a stronger laminate; excessive pressure can damage delicate filter media. Small trials are safer. A short trial can reveal large problems.
A filter materials lamination machine bonds several layers into a stable filter structure. Its value depends on material compatibility, not speed alone. Operators check fiber strength, surface texture, moisture, and heat tolerance before adjusting pressure or temperature.
Common combinations include spunbond nonwoven with meltblown media, cellulose paper with support scrim, and synthetic layers with activated carbon sheets. Some assemblies add a fine membrane over a coarse pre-filter. Each material reacts differently. Meltblown media can deform under excessive heat, while paper may curl when moisture changes. Small trials are essential. Keep samples.
Hot-melt lamination is widely used for fast, clean bonding. It suits many thermoplastic nonwovens and adhesive films. Thermal lamination uses heat and pressure to soften compatible fibers without added adhesive. Ultrasonic lamination creates narrow, precise bonds, especially around filter edges. Water-based or solvent-free adhesives may suit heat-sensitive materials, but curing time requires control. Operators should inspect bond width, air permeability, peel strength, and visible wrinkles. A perfect-looking bond can still restrict airflow. That is easy to miss. Test results should be recorded by material batch, temperature, line speed, and pressure. In practice, one setting rarely fits every filter design. A careful adjustment is often more reliable than a faster production run.
A filter materials lamination machine bonds two or more layers of filter media, support fabric, membrane, or protective film into a stable composite. The selected process depends on the material’s thermal behavior, thickness, porosity, and sensitivity to pressure or chemicals.
Note: The chart shows approximate material melting points, not recommended machine settings. Actual lamination temperatures depend on grade, layer structure, dwell time, pressure, and the required filtration performance. PTFE has a high melting point and is generally processed with specialized techniques rather than ordinary thermal lamination.
A filter materials lamination machine bonds two or more layers into one functional filter structure. It may use heat, adhesive, pressure, or ultrasonic energy. The selected method depends on material type, thickness, and temperature resistance. Operators control tension and alignment during production. Small errors can create wrinkles, weak seams, or uneven airflow.
In air filtration, laminated media supports HVAC panels, industrial dust collectors, and cleanroom pre-filters. In liquid filtration, layered membranes can improve particle retention and mechanical strength. Automotive filters may use laminated sheets to manage airflow inside compact housings. Manufacturing applications also include protective textiles, breathable construction materials, and composite sheets.
Each product needs practical testing, including peel strength, pressure drop, permeability, and thermal stability. A visually clean laminate is not always a reliable one. That assumption deserves testing.
Tips: Match adhesive chemistry with the filter medium. Check roll tension before production. Inspect cross-sections, not only surfaces. Record temperature and line speed for every batch. Trial runs often reveal problems that specifications miss.
What Is a Filter Materials Lamination Machine?
A filter materials lamination machine bonds layers such as nonwoven media, mesh, or support fabric. It uses controlled heat, adhesive, pressure, or a combination of these methods. Selection should begin with the material, not the machine’s advertised speed. Check the maximum web width, layer thickness, adhesive compatibility, and required bonding strength. A narrow tolerance can cause wrinkles, weak edges, or blocked pores.
During operation, confirm that each roll is clean and correctly aligned. Set web tension gradually. Excessive tension may stretch delicate media. Insufficient tension can create folds. Monitor temperature, nip pressure, and line speed together. A stable reading does not always mean a stable bond. Test a small sample and inspect peel strength, surface flatness, and visible contamination. Record the settings. This helps identify changes between production runs.
Maintenance should include daily cleaning around rollers, adhesive paths, and sensors. Remove residue before it hardens. Inspect roller surfaces for scratches and uneven wear. Check bearings, heaters, tension controls, and emergency switches at scheduled intervals. Calibration matters. A temperature display may look normal while the actual surface runs cooler. Replace worn parts before defects become routine. In practice, operators sometimes adjust speed to hide poor bonding, but this usually creates another problem. Review the process instead. Keep maintenance records with dates, findings, and corrective actions.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru