What Is Ion Exchange Membrane Equipment?
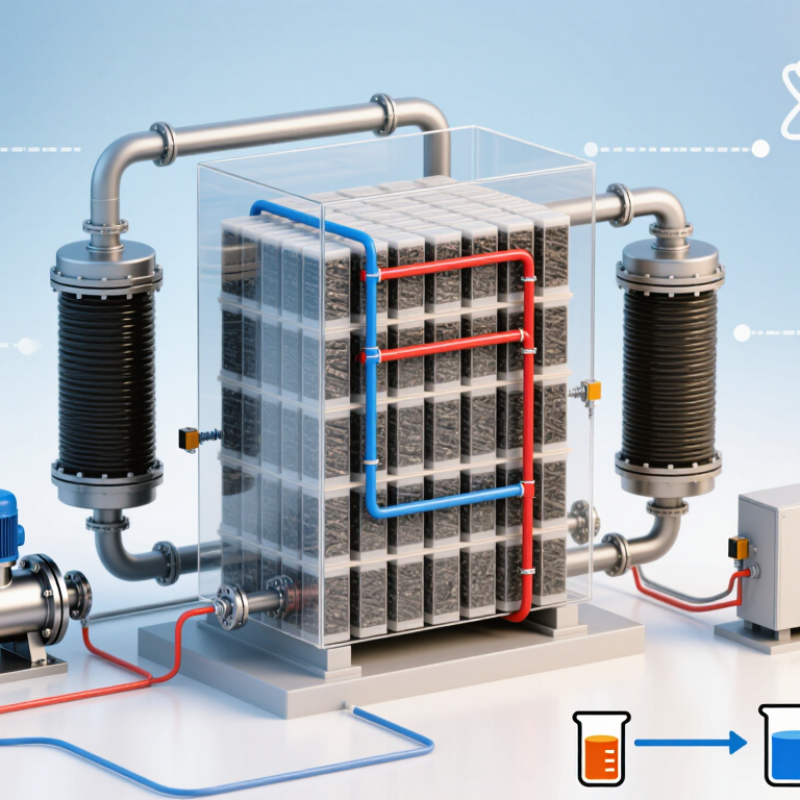
Ion Exchange Membrane Equipment is a specialized system for separating ions through selective membrane materials. It supports water treatment, chemical recovery, acid and base production, and resource purification. The equipment usually includes membrane stacks, electrodes, pumps, spacers, sensors, and control units. Together, these parts guide dissolved ions through carefully designed pathways.
The principle is precise. An electric field drives cations and anions across different membranes. Some ions pass through. Others remain behind. This controlled movement can transform saline feedwater into useful process streams. It can also recover valuable chemicals from industrial solutions. Professor Menachem Elimelech, a leading membrane technology researcher, has warned that “desalination is not a silver bullet.” His point matters here. Ion Exchange Membrane Equipment is powerful, but it cannot replace sound water management.
Real performance depends on more than membrane selection. Feed composition, temperature, pressure, current density, and fouling control all influence results. A membrane stack may look compact, yet small flow changes can affect energy use and product quality. Operators must inspect seals, monitor conductivity, and check voltage regularly. Practical experience matters.
The technology is not flawless. Organic fouling can reduce ion transport. Scaling may increase resistance inside narrow channels. Poor pretreatment can shorten membrane life. These weaknesses deserve attention, not polished promises. A reliable introduction should therefore examine equipment design, operating principles, applications, maintenance needs, costs, and environmental limits. That broader view helps engineers and buyers judge whether Ion Exchange Membrane Equipment truly fits their process.
Ion Exchange Membrane Equipment: Definition and Core Separation Functions
What Is Ion Exchange Membrane Equipment?
Ion Exchange Membrane Equipment: Definition and Core Separation Functions
Ion exchange membrane equipment uses electrically selective membranes to move ions while limiting unwanted species. A typical system includes membrane stacks, electrodes, pumps, sensors, and control units. Cation-exchange membranes transport positively charged ions. Anion-exchange membranes transport negatively charged ions. Under direct current, these layers create alternating dilute and concentrated channels.
Its core function is controlled separation. In electrodialysis, dissolved salts move from feed water into concentrate streams. The process can produce low-salinity water, recover valuable chemicals, or reduce wastewater volume. Bipolar membrane systems can also split water into hydrogen and hydroxide ions, supporting acid and base generation on site. Pretreatment remains essential. Suspended solids and scaling can reduce membrane life.
The International Energy Agency reported about 1.4 gigawatts of global installed water-electrolysis capacity by the end of 2023. That growth increases demand for reliable membrane assemblies and precise water management. The United Nations World Water Development Report 2024 states that agriculture represents roughly 70% of global freshwater withdrawals. This pressure strengthens interest in membrane-based reuse and concentration systems. Real operation is less perfect. Fouling still appears, and energy use depends heavily on salinity and recovery targets. A careful design must measure both separation performance and maintenance cost.
Membrane Structures, 100–200 μm Thickness, and Selective Ion Transport
Ion exchange membrane equipment uses charged polymer membranes to separate ions while blocking unwanted species. A typical unit includes membrane sheets, porous electrodes, flow channels, gaskets, frames, manifolds, and sensors. In water electrolysis, the membrane carries protons or hydroxide ions between electrodes. Its structure controls resistance, swelling, pressure tolerance, and gas crossover.
Membranes between 100 and 200 μm thick offer a practical balance. Thinner films usually reduce ionic resistance. However, they can tear, dry out, or permit greater crossover. Thicker films improve mechanical strength but may consume more energy. The U.S. Department of Energy’s electrolyzer technology assessments identify conductivity, durability, and gas crossover as major engineering constraints. These factors matter more than thickness alone.
Selective ion transport depends on fixed charged groups within the polymer network. Hydrated channels allow target ions to move, while larger molecules face stronger barriers. Temperature, hydration, pressure, and current density can change this behavior. The International Energy Agency reported global installed electrolyzer capacity above 1 GW in 2023, increasing demand for reliable membrane systems. Yet laboratory performance can look cleaner than factory operation. Dust, uneven compression, and imperfect sealing still cause failures. Engineers should verify membrane thickness, area resistance, crossover rates, and lifetime under real cycling conditions.
Electrodialysis Stacks: 10–50 mA/cm² Typical Current-Density Range
What Is Ion Exchange Membrane Equipment?
Electrodialysis Stacks: 10–50 mA/cm² Typical Current-Density Range
Ion exchange membrane equipment moves dissolved ions through selective membranes. An electrodialysis stack alternates cation-exchange and anion-exchange membranes. Spacers create narrow flow channels. Direct current then separates salts into concentrated and diluted streams.
A 10–50 mA/cm² current-density range is common for industrial electrodialysis design. The lower range usually supports stable operation with difficult feedwater. The upper range can improve throughput, but it increases concentration polarization and scaling risk. Current density is calculated from amperage divided by active membrane area. A 1,000 cm² membrane operating at 30 mA/cm² carries about 30 amperes.
That number matters.
Global Water Intelligence’s Global Water Market 2024 reports more than 20,000 desalination facilities worldwide, showing the scale of membrane-based water treatment. Industry reviews from the International Desalination Association also emphasize energy use, pretreatment, and reliable operation as major project concerns. These findings support careful stack sizing, not simply selecting the highest current.
During commissioning, operators should measure conductivity, temperature, pressure drop, and stack voltage. Feedwater hardness and suspended solids can change the practical limit. A 50 mA/cm² setting may perform well in clean laboratory water, yet fail in a real brackish stream. That gap is easy to underestimate. Some designs also need periodic polarity reversal or chemical cleaning. The best operating point is often below the theoretical maximum, which deserves more attention in equipment specifications.
Electrodeionization Units: Producing 15–18 MΩ·cm High-Purity Water
What Is Ion Exchange Membrane Equipment?
Electrodeionization units combine ion-exchange resin, selective membranes, and a direct-current field. They continuously remove dissolved ions from water without chemical regeneration. In well-designed systems, product resistivity can reach 15–18 MΩ·cm at 25°C. The theoretical ceiling for pure water is about 18.2 MΩ·cm.
That number needs context. The U.S. Pharmacopeia’s General Chapter <1231> treats conductivity and total organic carbon as important water-quality controls. ASTM D1125-23 also defines procedures for measuring conductivity and resistivity. These standards support reliable testing, but they do not make every EDI outlet equivalent. Feedwater quality matters greatly. Hardness, carbon dioxide, silica, boron, and residual chlorine can reduce performance.
A typical installation uses pretreatment, reverse osmosis, and EDI polishing. At the outlet, a resistivity sensor displays the result in real time. Stable readings should be checked against temperature compensation and laboratory verification. Small leaks, exhausted pretreatment media, or poor grounding may cause a sudden decline. It is not magic.
Operating experience shows that EDI performs best with consistent RO permeate and controlled flow. A higher resistivity reading is not automatically safer water. Organic contamination may remain even when ionic conductivity looks excellent. This is where USP testing and documented sampling become essential. The target is impressive, but the process still deserves skepticism.
Industrial Applications: Chlor-Alkali Processing, Desalination, and Reuse
What Is Ion Exchange Membrane Equipment?
Ion exchange membrane equipment uses electrically charged membranes to control ion movement in liquids. A typical system includes membrane stacks, electrodes, pumps, sensors, and a direct-current power supply. In chlor-alkali processing, brine flows through separated compartments. Sodium ions pass through the membrane, while chlorine and hydrogen form in different zones. This arrangement produces caustic soda with fewer unwanted by-products. Careful brine purification remains essential. Small amounts of calcium or magnesium can damage membrane performance.
Desalination plants use electrodialysis equipment to remove dissolved salts from brackish water. An electric field moves positive and negative ions through alternating membranes. The process creates separate concentrated and desalinated streams. Operators monitor conductivity, pressure, voltage, and flow balance. Feedwater quality changes daily, so fixed settings can become unreliable. Pretreatment may reduce scaling, suspended solids, and organic fouling. Still, membranes require regular inspection and controlled cleaning.
Water reuse facilities apply ion exchange membrane systems to industrial wastewater and process water. They can reduce salinity before cooling, washing, or boiler applications. Some systems also support selective recovery of useful ions. Results depend heavily on the wastewater composition and pretreatment design. A pilot test often reveals problems that laboratory data misses. Membranes are not maintenance-free. Fouling develops quietly. Even experienced operators must review energy use, membrane ageing, and changing discharge requirements.