Why Choose Grade 304L Stainless Steel Coils?
Why Choose Grade 304L Stainless Steel Coils?
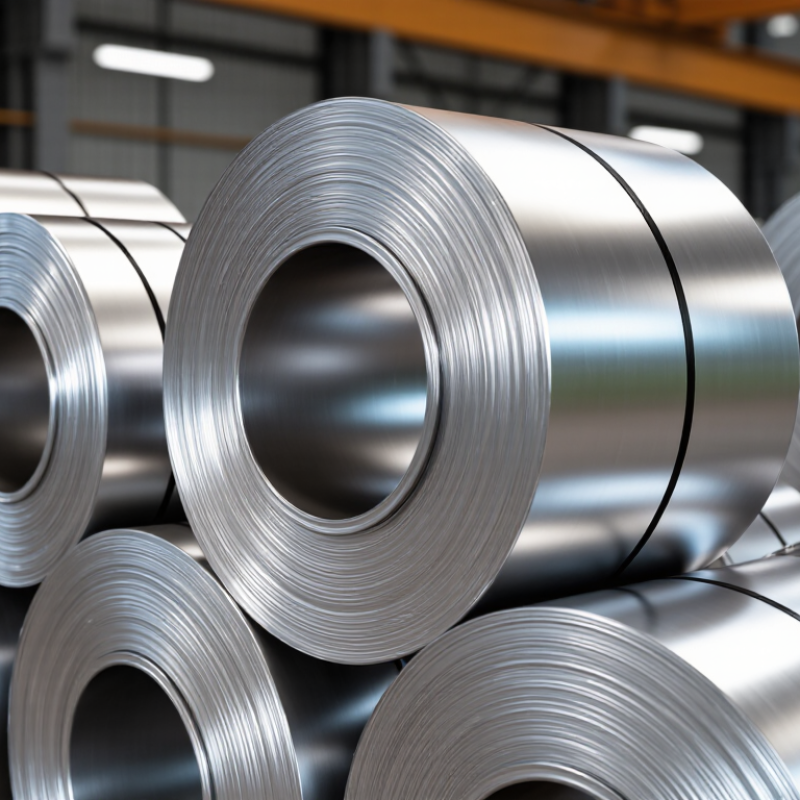
Grade 304l Stainless Coils remain a practical choice for demanding fabrication and everyday industrial service. ASTM A240 limits 304L carbon content to 0.030%, helping reduce carbide precipitation during welding. The specification also identifies chromium near 18–20% and nickel near 8–12%. These elements support corrosion resistance, surface durability, and reliable forming performance. It is a useful balance.
The World Stainless Association reported approximately 58.4 million tonnes of stainless steel production in 2023. That figure confirms stainless steel’s continuing importance across construction, food equipment, transportation, and process industries. However, production volume alone does not prove suitability. Project conditions still matter. Chlorides, heat, cleaning chemicals, and weld quality can change the result.
J. R. Davis, editor of ASM Specialty Handbook: Stainless Steels, describes Type 304 as “the most widely used stainless steel.” That observation explains its broad availability and familiar processing behavior. The low-carbon 304L variant is especially valuable when welded joints require better resistance to sensitization. Buyers can often source it in different thicknesses, finishes, and coil widths.
No grade is perfect. Severe chloride exposure may require a higher-alloy alternative, such as 316L. Yet 304L often delivers dependable performance without unnecessary alloy cost. Careful inspection remains essential. Mill certificates, dimensional checks, surface evaluation, and independent testing strengthen purchasing confidence. For engineers comparing lifecycle value, Grade 304l Stainless Coils offer a credible starting point, provided the environment and fabrication method receive equal attention.
What Is Grade 304L Stainless Steel?
Why Choose Grade 304L Stainless Steel Coils?
What Is Grade 304L Stainless Steel?
Grade 304L is a low-carbon austenitic stainless steel containing chromium and nickel. The lower carbon content helps reduce carbide precipitation during welding. This feature can improve resistance to intergranular corrosion near welded areas.
In practical fabrication, 304L coils are often cut, formed, and welded into tanks, panels, kitchen equipment, and process components. Their smooth surface is easy to clean, while their balanced strength supports many indoor and outdoor applications. The material also performs well in ordinary atmospheric conditions. However, it is not immune to corrosion. High chloride exposure can still cause staining or pitting, especially when moisture remains trapped on the surface.
Tips: Check the coil’s material certificate, thickness tolerance, surface finish, and heat number before production. Match the grade with the service environment, not only the purchase price. Keep tools clean during fabrication. Iron contamination can leave rust marks on stainless steel. Pickling or passivation may also be needed after welding, depending on the application.
A careful selection process matters. 304L is versatile, but it may not suit severe marine, chemical, or high-temperature conditions. I have seen specifications rely too heavily on the word “stainless.” That assumption deserves a second look. Temperature, chloride levels, cleaning methods, and welding design should guide the final choice.
Why Choose Grade 304L Stainless Steel Coils?
Grade 304L is the low-carbon version of 304 stainless steel. Its reduced carbon limit helps minimize chromium carbide precipitation during welding, supporting better resistance to intergranular corrosion in welded components.
Minimum mechanical properties and maximum carbon limits shown for annealed sheet, plate, and coil specifications commonly listed under ASTM A240. Values may vary by product form and applicable standard.
Key Properties of 304L Stainless Steel Coils
304L stainless steel coils are valued for their balanced mechanical and chemical properties. ASTM A240/A240M specifies a carbon limit of 0.030% maximum, with approximately 18–20% chromium and 8–12% nickel. The reduced carbon level helps limit carbide precipitation during welding. That matters when fabricators join thin coil sections and cannot fully solution-anneal every seam.
In the annealed condition, ASTM A240/A240M lists a minimum tensile strength of 485 MPa, a yield strength of 170 MPa, and 40% elongation. These figures explain its practical flexibility. A 304L coil can be stamped into clean curves, formed around tight radii, and welded with relatively low cracking risk. ASM Handbook data also places its density near 8.0 g/cm³ and thermal conductivity near 16 W/m·K at room temperature. Operators still need controlled tooling and suitable lubrication. Forming is not effortless.
Its chromium content supports a passive surface film, giving useful resistance in many food-processing, architectural, and indoor industrial environments. However, 304L is not corrosion-proof. Chloride-rich water, stagnant moisture, and rough weld areas can still produce staining or localized attack. The International Stainless Steel Forum notes that surface finish and maintenance strongly influence stainless steel service performance. In practice, a smooth coil surface, clean handling, and proper post-weld treatment may matter as much as the nominal grade. That is an easy detail to underestimate.
Why Choose 304L Coils for Different Applications?
Why Choose Grade 304L Stainless Steel Coils?
Why Choose 304L Coils for Different Applications?
304L stainless steel coils suit many applications because they combine formability, weldability, and practical corrosion resistance. ASTM A240/A240M limits carbon to 0.030%, reducing carbide precipitation during welding. This matters for tanks, food-processing panels, kitchen equipment, and fabricated tubing. The low-carbon chemistry can help preserve corrosion resistance near welded areas, although poor cleaning may still cause staining.
Industry data supports stainless steel’s broad importance. The International Stainless Steel Forum reported global stainless crude steel production of about 58.4 million tonnes in 2023. NACE’s IMPACT study estimated annual corrosion costs at approximately 3.4% of global gross domestic product. These figures explain why material selection deserves more than a price comparison. A correctly specified 304L coil can reduce maintenance risks when thickness, surface finish, forming radius, and welding practice match the service environment.
Yet 304L is not a universal solution. High chloride exposure, warm seawater, or aggressive chemical conditions may require a higher-alloy grade. A bright surface also does not guarantee long-term performance. Fabricators should inspect edges, remove heat tint, and verify passivation when necessary. In real workshops, small process errors often matter more than the datasheet. That is easy to overlook.
Factors to Consider Before Buying 304L Coils
Why Choose Grade 304L Stainless Steel Coils?
Factors to Consider Before Buying 304L Coils
304L coils suit welded equipment because their carbon limit is 0.030% maximum under ASTM A240/A240M. This reduces carbide precipitation near welds, especially during repeated fabrication. The grade contains roughly 18% chromium and 8% nickel, supporting a stable passive surface in many indoor and moderately corrosive environments. Still, 304L is not universally corrosion-proof. Chlorides, stagnant water, and hot chemical exposure can cause pitting.
Check more than the grade name. Confirm thickness, width, coil weight, surface finish, edge condition, and flatness against ASTM A480/A480M requirements. Request a material test certificate with chemistry, tensile results, yield strength, elongation, heat number, and solution-annealing details. ISO 6892-1 provides the tensile-testing framework, but test results can vary with sampling direction and product thickness. That detail is easy to overlook.
Think about the actual service environment. A bright 2B finish may work for process frames, while brushed surfaces need tighter cosmetic control. World Stainless reported approximately 58.4 million tonnes of crude stainless steel production in 2023, showing the scale of supply, not guaranteed consistency. Compare several heat numbers and inspect samples before committing to a large coil. A low price can hide slitting burrs, uneven edges, or questionable traceability. This is where buyers sometimes learn expensively. Also check packaging, moisture protection, delivery tolerances, and whether the supplier can provide replacement material when specifications are missed.