Why choose a Green Machine Optical Sorter when valuable materials still leave modern recycling lines? The World Bank reported approximately 2.01 billion tonnes of municipal solid waste in 2016. At least 33% lacked safe management. UNEP’s Global Waste Management Outlook 2024 projects annual municipal waste could reach 3.8 billion tonnes by 2050. These figures expose a practical problem: disposal volumes are rising, while sorting accuracy remains essential.
A Green Machine Optical Sorter can identify materials through near-infrared sensors, cameras, metal detection, and controlled air jets. It may separate plastics by polymer type, colors, or contamination levels. The exact result depends on belt speed, moisture, material size, and maintenance. No sorter is magic. Circular-economy expert Walter R. Stahel expressed the principle clearly: “Waste is a resource in the wrong place.” That idea gives optical sorting a measurable purpose: returning misplaced resources to productive streams.
The OECD Global Plastics Outlook estimated 353 million tonnes of plastic waste in 2019, with only 9% recycled. A well-tested Green Machine Optical Sorter can support higher recovery and more consistent product quality. Operators can inspect rejected items beside the conveyor, adjust air pressure, and compare purity data across shifts. However, performance claims require site trials, not attractive brochures. Energy use, spare parts, operator training, and downtime also deserve attention. The best choice is not simply the fastest machine. It is the system that delivers verified recovery, stable purity, and practical service support in the real facility. Sometimes, the overlooked details decide everything.
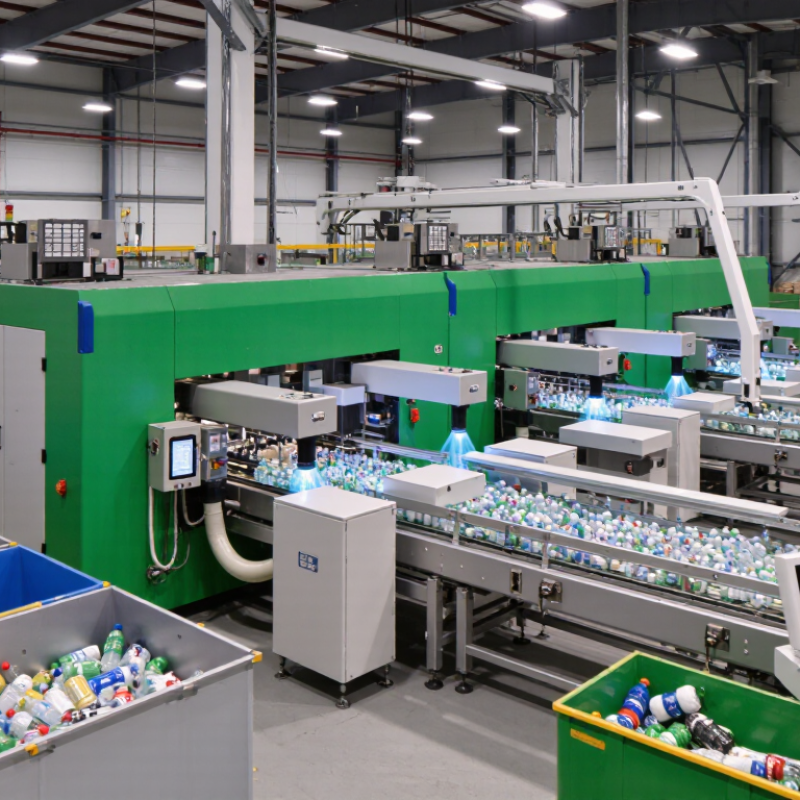
A green machine optical sorter is an automated system for identifying and separating materials on a moving conveyor. Cameras, near-infrared sensors, and software examine each item within milliseconds. Air jets then push selected materials into separate chutes. The system can recognize plastics, paper, metals, and specific colors. It supports cleaner output with less manual handling.
The need is growing. The World Bank’s What a Waste 2.0 report estimated 2.01 billion tonnes of municipal solid waste in 2016. It projects 3.40 billion tonnes annually by 2050. Better sorting can protect material value before contamination spreads. The Global E-waste Monitor 2024 reported 62 million tonnes of electronic waste in 2022. However, an optical sorter cannot identify every complex product reliably. Dark plastics, wet packaging, and crushed items remain difficult.
Tips: Test representative waste samples before selecting equipment. Measure accuracy, recovery, energy use, and maintenance time. Ask for independent performance data, not only demonstration results. Keep conveyors evenly loaded. A crowded belt reduces detection quality.
From practical sorting operations, calibration often matters as much as hardware. Sensor lenses need cleaning, and air pressure requires regular checks. I would not promise perfect purity. Operators should compare results across seasons and changing material streams. According to the U.S. Environmental Protection Agency, recycling systems depend on reducing contamination and improving material quality. A well-managed sorter can help, but process discipline still decides the final performance.

Optical sorting technology uses cameras, sensors, software, and precise air jets to identify materials on a moving conveyor. As mixed recyclables pass beneath the sensor housing, high-speed cameras capture color, shape, size, and surface details. Near-infrared sensors can also distinguish paper, plastics, and other material types by their light-reflection patterns. The system compares this information with programmed specifications within milliseconds.
When the software detects a target item, it calculates the item’s position and speed. A row of small air nozzles then releases a short burst of compressed air. This redirects the selected material into another chute while the remaining items continue forward. The timing must be extremely accurate. A delay of only a fraction of a second can send an item into the wrong stream.
In practical facilities, performance depends on more than advanced sensors. Clean lenses, stable lighting, correct belt speed, and regular calibration all influence sorting accuracy. Operators should inspect rejected materials and adjust settings when contamination changes. No sorter is perfect. Dark objects, overlapping items, dust, and damaged packaging can still confuse the system. Careful testing with local material samples makes the results more dependable and reduces unnecessary manual rechecking.
A modern optical sorter uses near-infrared cameras, air jets, and software to identify materials on a conveyor. It can separate PET bottles, HDPE containers, PP packaging, mixed paper, cardboard, and selected films. Some glass systems also use optical sensors. However, moisture, color, breakage, and belt speed can reduce accuracy. Real-world trials matter.
The OECD Global Plastics Outlook reported that only 9% of plastic waste was successfully recycled worldwide in 2019. Better identification can keep valuable plastic from entering residue streams. It cannot fix contamination. Operators can tune sorting by polymer type, color, shape, and target purity. Clear PET may be separated from colored PET, while natural HDPE can be recovered from mixed containers. Thin films remain difficult when they cling to paper or wrap around shafts.
The U.S. Environmental Protection Agency reported 67.4 million tons of paper and paperboard in municipal solid waste generation in 2018. That volume makes stable paper sorting essential. Airflow, belt loading, and moisture require regular checks. No sorter is perfect. A practical installation begins with a material audit. Measure particle size, contamination, seasonal changes, recovery, and purity. Test samples across different shifts. Operators may need daily lens cleaning and recalibration after feed changes. These less visible tasks often determine actual performance.
Optical sorting systems use visible cameras and near-infrared sensors to identify and separate common recyclable materials by color, shape, and spectral response.
The chart shows representative sensing bands commonly used for material recognition. Paper, cardboard, PET, HDPE, PP, and textiles are frequently identified with near-infrared detection, while glass is commonly recognized through visible-light color and shape analysis. Actual performance depends on material color, contamination, moisture, particle size, and sensor configuration.
A green machine optical sorter can improve recovery without adding unnecessary manual handling. In a modern materials recovery facility, cameras and sensors identify color, shape, and polymer type. Air jets then separate selected items within milliseconds. This supports steadier throughput and more consistent product quality.
The World Bank’s What a Waste 2.0 report estimates global municipal waste could reach 3.4 billion tonnes annually by 2050. Better sorting capacity will matter. The OECD’s Global Plastics Outlook reports that only 9% of plastic waste was recycled globally in 2019. Optical sorting can remove unwanted items earlier, protect recyclable streams, and reduce landfill dependence. It can also lower repetitive labor demands and provide useful performance data.
However, the system is not magic. Dust, crushed containers, dark materials, and poor calibration can reduce accuracy. A machine may reject valuable material when settings are rushed. Operators still need training and regular quality checks.
Tips: Test representative material before purchasing. Measure recovery rate, purity, uptime, energy use, and maintenance hours. Review results across wet, dusty, and high-volume shifts. The U.S. Environmental Protection Agency reported a 32.1% municipal recycling and composting rate in 2018, showing that equipment alone cannot solve every process gap. Pair optical sorting with clear collection rules, routine sensor cleaning, and documented calibration. Small errors become expensive when they repeat every hour.
Why Choose a Green Machine Optical Sorter?
How Should Businesses Evaluate and Maintain the Equipment?
A green optical sorter should be judged by measurable performance, not attractive claims. Request a trial using your own material, including wet, dusty, and mixed samples. Record throughput, recovery rate, purity, false rejects, energy use, and compressed-air consumption. The U.S. Environmental Protection Agency reported 292.4 million tons of municipal solid waste in 2018, with only 32.1% recycled or composted. Small accuracy losses can therefore create substantial material waste.
Check the complete operating environment. Examine conveyor speed, sensor resolution, software updates, access panels, spare-part availability, and operator training. UNEP’s Food Waste Index Report 2024 estimated 1.05 billion tonnes of food waste in 2022. For food applications, hygienic design and cleaning access deserve equal attention. A spreadsheet may look convincing. A damp morning can reveal poor calibration. Businesses should also compare verified production data against vendor test results. The gap may be uncomfortable, but it matters.
Tips: Clean sensor windows at every shift change. Inspect air filters and ejector nozzles daily. Keep a calibration log with material type, temperature, and moisture. Review rejected samples weekly. Replace worn seals before dust enters the camera housing. Do not adjust sensitivity without recording the reason. Maintenance teams sometimes focus on breakdowns and overlook gradual accuracy loss. That mistake is expensive. EPA and UNEP data show why recovery quality, stable operation, and measured maintenance deserve careful investment.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







