Why Choose an SMT Reflow Machine for PCB Assembly? The answer begins with control. A Smt Reflow Machine applies heat through a programmed profile, helping solder paste melt and form reliable joints across a populated board. That matters when a PCB carries tiny components, fine-pitch leads, or mixed thermal masses. Heat is unforgiving. A few degrees or seconds can change the result.
IPC’s monthly North American Electronics Manufacturing Services (EMS) Business Conditions Report tracks industry indicators such as sales, orders, and capacity. It offers useful context: electronics production operates under shifting demand, so repeatable processes matter. IPC’s J-STD-001 and IPC-A-610 standards also set widely used requirements for soldered assemblies and workmanship. They do not guarantee a good process by themselves. Setup still matters.
A reflow oven can help manufacturers repeat thermal conditions, reduce reliance on manual soldering, and support higher-volume assembly. Its value depends on the board, solder paste, component mix, and profile validation. A machine is not a shortcut. It must be configured and monitored.
Quality pioneer W. Edwards Deming wrote, “In God we trust; all others must bring data.” Deming was not an SMT reflow specialist, so this is a quality-management principle, not a reflow-machine endorsement. Still, it points to a practical question: can the chosen Smt Reflow Machine produce stable, measurable results on your actual boards? Before buying, compare profile control, temperature uniformity, throughput, maintenance needs, and support. Then test with your own assemblies. That step is easy to overlook.
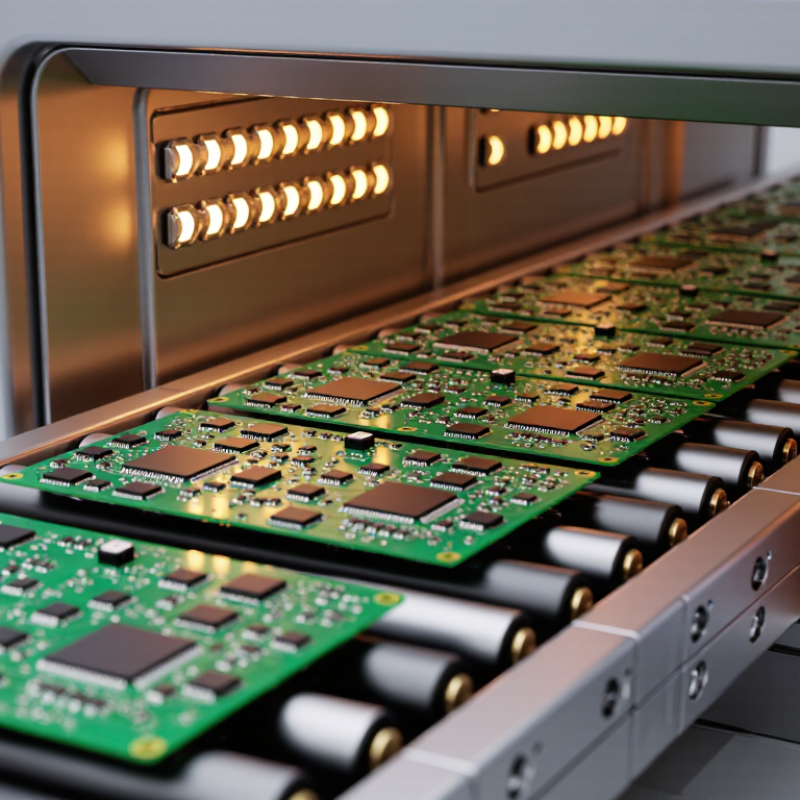
An SMT reflow machine heats a populated PCB in controlled stages. Solder paste first warms and releases volatiles, then melts and wets component leads and board pads. Cooling solidifies the joints. That is the job. The conveyor carries each board through heating zones, while operators tune the temperature profile to the solder alloy, board thickness, and component limits. A heavy copper ground plane may heat more slowly than a small connector. Thermocouples placed at these points reveal what the board actually experiences, not just what the oven display shows.
Grand View Research’s printed circuit board market report estimated the market at USD 73.6 billion in 2022 and projected 5.2% annual growth from 2023 to 2030. That scale makes repeatable assembly important, though market growth alone does not prove a particular process is better. IPC-7530 provides guidance on developing reflow profiles, and IPC J-STD-001 sets requirements for soldered electrical and electronic assemblies. Small details matter. A profile that is too hot can damage sensitive parts; too cool, and joints may not form properly. Even a well-set oven needs checks when board designs or paste batches change. The process is precise, but not foolproof.
An SMT reflow machine heats a populated PCB according to a controlled temperature profile, melting solder paste to form electrical and mechanical connections between surface-mount components and the board. The values below are typical examples; the correct profile depends on the solder paste, components, PCB design, and process requirements.
| Process Stage or Factor | What the Reflow Machine Does | Typical Example | Why It Matters |
|---|---|---|---|
| Preheat | Raises the PCB and components’ temperature gradually. | Often ramps toward approximately 150–200°C, depending on the selected profile. | Reduces thermal shock and begins activating the solder-paste flux. |
| Soak | Holds the assembly within a controlled temperature range before peak heating. | A common profile may use a soak around 150–200°C for roughly 60–120 seconds. | Helps equalize temperatures across the board and allows flux to remove surface oxides. |
| Reflow above liquidus | Heats solder paste above its melting point so solder particles fuse into joints. | For SAC305 lead-free solder, the liquidus temperature is about 217°C; time above liquidus is often around 45–75 seconds. | Creates the solder connections that attach surface-mount components to PCB pads. |
| Peak temperature | Provides a controlled peak to complete solder melting and wetting. | A typical SAC305 profile may peak around 235–250°C, subject to paste and component limits. | Too little heat can cause incomplete joints; excessive heat can damage components or the PCB. |
| Cooling | Lowers the assembly temperature in a controlled way so molten solder solidifies. | Cooling rates around 2–4°C per second are commonly used as a starting point for profile development. | Influences solder-joint solidification and helps avoid excessive thermal stress. |
| Temperature-zone control | Uses independently controlled heating zones to shape the thermal profile. | Zone count and settings vary by machine, PCB size, and production needs. | Allows the process to be adjusted for different assemblies and solder-paste requirements. |
| Conveyor speed | Moves each PCB through the heating and cooling zones at a set rate. | Speed is set to achieve the required dwell times and profile; there is no single value suitable for every assembly. | Supports repeatable processing and helps maintain consistent results across a production run. |
| Profile verification | Works with thermocouples and a profile logger to measure temperatures at points on the PCB. | Measurements are compared with the solder-paste specification and component temperature limits. | Confirms that the actual board—not just the oven settings—experiences an appropriate thermal profile. |
Practical note: Treat temperature ranges as profile-development examples, not universal settings. Validate the profile on the actual PCB assembly using the solder-paste supplier’s recommendations and the temperature limits of the components.
Why Choose an SMT Reflow Machine for PCB Assembly?
Reliable electrical connections begin with controlled heat, not appearance alone. An SMT reflow machine follows a programmed thermal profile across preheat, soak, reflow, and cooling. For common lead-free solder, IPC/JEDEC J-STD-020 data typically specifies peak temperatures around 235–260°C and time above liquidus near 60–150 seconds. This controlled exposure melts solder evenly around component leads and pads. It also reduces cold joints, tombstoning, and uneven wetting. IPC J-STD-001 and IPC-A-610 provide workmanship requirements for acceptable solder joints and assembly quality. In practice, a smooth joint can still hide weak bonding. Inspection must include process records, not only visual checks.
An SMT reflow machine improves repeatability across hundreds of boards. Its conveyor speed, zone temperatures, and oxygen control can be monitored and adjusted. The 2024 Global Electronics Association industry outlook identifies quality and reliability as continuing manufacturing priorities, while rising product complexity increases process sensitivity. That pressure makes profile verification essential. However, reflow is not automatically perfect. Warped boards, poor paste storage, and inaccurate thermocouple placement can still create defects. I have seen apparently clean assemblies fail after thermal cycling. The profile was close, but not stable enough.
Tips: Measure the actual board profile regularly. Use thermocouples near large ground planes and heat-sensitive components. Keep solder paste within its specified storage limits. Record every correction. Small changes matter.
A controlled reflow profile gradually heats the PCB, activates the solder paste, melts the alloy, and cools the assembly at a controlled rate. This repeatable thermal cycle helps create consistent solder joints and reliable electrical connections.
The chart shows a typical lead-free SAC305 reference profile: a controlled preheat and soak stage, a peak temperature near 245°C, and approximately 90 seconds above the 217°C melting point. Actual settings should be verified with thermocouple measurements for the specific PCB, components, and solder paste.
In a modern PCB assembly line, a reflow machine heats solder paste through controlled temperature zones. Components remain aligned while the paste melts and forms reliable joints. Operators can monitor each zone, conveyor speed, and oxygen conditions during production. This control supports repeatable results across different board sizes and component densities.
Consistency matters most.
A well-tuned thermal profile reduces common defects, including insufficient solder, bridging, tombstoning, and component damage. The process also supports fine-pitch packages that are difficult to solder manually. With stored profiles, technicians can compare production runs and adjust settings using measured data. Thermocouples attached to test boards provide practical evidence instead of relying on visual judgment alone.
Small details matter.
Reflow machines also improve productivity by reducing manual handling and supporting continuous production. They can lower variation between operators and make process records easier to maintain. However, the machine does not guarantee perfect assemblies. Incorrect paste storage, poor stencil design, or uneven board loading can still create defects. This is where experience becomes important. Engineers should review inspection results, confirm profile accuracy, and reconsider settings after material or layout changes. Sometimes, a profile that worked yesterday performs poorly today. That uncomfortable result deserves investigation, not excuses.
Selecting an SMT reflow machine requires more than comparing heating zones or purchase prices. The machine must match your board size, component density, solder paste, and daily production volume. Consistency matters. A stable temperature profile protects fine-pitch parts and reduces defects such as solder bridges, tombstoning, and incomplete joints.
I have found that thermal profiling reveals problems that visual checks often miss. Attach thermocouples to large ground areas, small passive components, and heat-sensitive packages. Then compare the measured curve with the solder paste manufacturer’s recommended range. Do not guess. Zone control, conveyor speed, and cooling capacity should support that profile. A machine with too few zones may struggle with heavy boards or uneven copper areas.
Practical maintenance also deserves attention. Check whether filters, heaters, sensors, and conveyor parts are easy to inspect and replace. Reliable data logging helps operators trace temperature changes across production batches. Consider nitrogen capability only when your materials and quality targets justify it; it can add operating complexity. Safety controls, power consumption, exhaust handling, and operator training affect long-term value. A wider conveyor may seem useful, but it can waste energy when most boards are small. My own judgment would remain cautious here: an impressive specification sheet does not guarantee better assemblies. Trial runs with real boards provide stronger evidence.
Reflow soldering suits PCB assemblies with many surface-mount components. It applies heat through a controlled thermal profile. This process creates consistent solder joints across an entire panel. In production, that repeatability reduces manual touch-up and placement errors. It works especially well for fine-pitch integrated circuits, small resistors, and compact capacitor arrays. These parts are difficult to solder reliably by hand.
High-volume consumer electronics, industrial controllers, communication modules, and LED boards often benefit from reflow processing. A well-tuned oven can handle lead-free solder and multilayer boards with different thermal capacities. Engineers should review component temperature limits before production begins. Plastic connectors, sensors, and heat-sensitive parts may need special protection or later assembly. Not every PCB belongs in the oven.
Thermal profiling remains essential. Technicians should measure temperatures at several board locations, not only inside the chamber. A profile that works for a small board may fail on a large copper-heavy panel. Solder paste age, stencil design, conveyor speed, and board spacing also affect results. Small defects can reveal larger process problems. Tombstoning, voids, and insufficient wetting deserve careful investigation. Reflow is efficient, but it is not automatic perfection. Sometimes, a slower profile produces better joints than a faster cycle.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru