Precision manufacturing demands more than attractive drawings and expensive machinery. It requires controlled movement, suitable materials, verified measurements, and experienced judgment. CNC Milling brings these elements together by guiding rotating cutting tools across multiple axes. This process can produce slots, pockets, holes, contours, and complex surfaces with consistent accuracy.
In a capable workshop, engineers begin with a manufacturable CAD model and a carefully reviewed CAM program. They select cutting speeds, feeds, tooling, and workholding according to the material. Aluminum may produce bright, clean chips, while hardened steel requires slower settings and stronger tooling. These details directly affect surface finish, dimensional stability, production time, and tool life. Reliable manufacturers also inspect critical features with calibrated gauges, probes, or coordinate measuring equipment. Small checks matter.
Repeatability is a major reason companies choose CNC Milling. Once a proven program is established, identical components can be produced with less variation between batches. This supports prototypes, medical equipment, aerospace components, and industrial machinery. However, CNC Milling is not a magic button. Poor fixture design, vague drawings, or an unchecked toolpath can still create costly defects. That limitation deserves attention.
The strongest results come from collaboration between designers, programmers, machinists, and inspectors. Clear tolerances and realistic expectations prevent unnecessary precision costs. A thoughtful manufacturing partner will also question unclear features instead of simply cutting metal. That professional hesitation can save time. In the end, CNC Milling offers precision, flexibility, and dependable production when technical knowledge supports the machine.
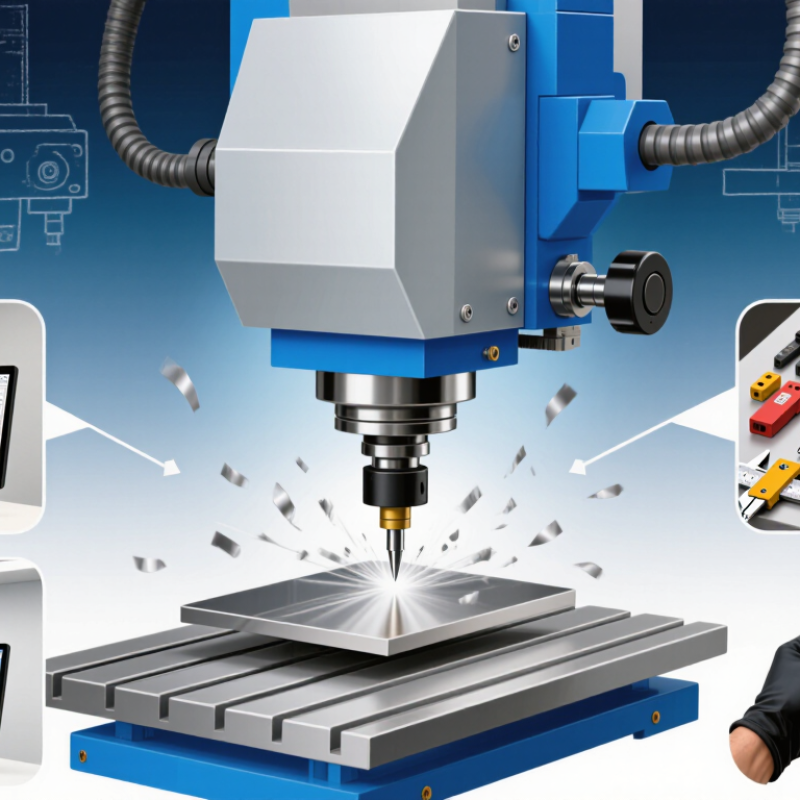
CNC milling is a subtractive manufacturing process. It shapes metal, plastic, or composite material by removing controlled amounts with rotating cutting tools. Unlike manual machining, the cutter follows programmed coordinates. This allows complex pockets, slots, holes, and curved surfaces to be produced repeatedly. The result depends on both machine accuracy and careful process planning.
The work begins with a digital 3D model or engineering drawing. A programmer converts this design into toolpaths through computer-aided manufacturing software. These instructions become machine code, which controls cutting speed, feed rate, tool movement, and depth. The operator then secures the raw material on the worktable. Strong workholding matters. Even slight movement can ruin a precise feature.
During cutting, the machine removes material layer by layer. Coolant may reduce heat and carry chips away from the cutting zone. Tool wear must be monitored because a dull edge can leave rough walls or incorrect dimensions. After machining, an inspector checks key features with gauges, probes, or coordinate measuring equipment. In practical production, measurement is not optional. It reveals problems that visual inspection misses. Still imperfect. Temperature changes, vibration, and setup errors can influence results. A reliable process records these variables and adjusts them when evidence demands it. Precision is engineered, not assumed.
CNC milling removes material through computer-controlled cutting along multiple machine axes. More controlled axes allow better access to complex surfaces and can reduce the number of setups required.
A 3-axis mill moves along X, Y, and Z. A 4-axis machine adds rotary motion, while a 5-axis machine combines three linear and two rotary axes. This axis flexibility supports accurate machining of angled faces, complex contours, and difficult-to-reach features.
Why Choose CNC Milling for Precision Manufacturing?
How CNC Milling Achieves High Precision and Repeatability
CNC milling converts a digital design into controlled tool movements. The machine follows programmed coordinates with consistent speed and depth. This reduces variation between parts, especially during repeated production. A rigid fixture keeps the workpiece from shifting under cutting pressure. Even a small movement can affect a tight tolerance.
Precision also depends on practical controls. Operators check tool wear, spindle temperature, and material stability during machining. A worn cutter may leave rough walls or change a pocket’s size. Tool offsets help correct these changes before they affect many parts. Coolant manages heat and carries chips away from the cutting zone. Clean chips matter more than many people expect.
Inspection confirms whether the process works. Probes can measure key surfaces inside the machine. Micrometers and coordinate measuring equipment provide additional verification. In my experience, the first part often reveals an overlooked detail. A thin wall may flex, or a fixture may distort a flat surface. That is not a failure to hide. It is useful process evidence. Adjusting the tool path, support points, or cutting conditions can improve repeatability. Still, no process remains perfect without regular calibration and careful human judgment.
Material choice determines whether a milled component performs reliably or becomes an expensive rework project. Aluminum offers low density, fast cutting, and strong corrosion resistance for housings, brackets, and heat sinks. The U.S. Geological Survey reported approximately 70 million metric tons of primary aluminum production in 2023, supporting broad material availability. Stainless steel suits shafts, fixtures, and fluid-handling parts where strength and hygiene matter.
Titanium is valuable for lightweight structural components exposed to heat or corrosive environments. It requires slower cutting, rigid workholding, and careful tool control. The 2024 USGS Mineral Commodity Summaries recorded global titanium sponge production near 280,000 metric tons in 2023. That supply is smaller than aluminum’s. Cost can rise quickly.
Engineering plastics, brass, and copper also work well for bushings, electrical parts, and low-load covers. Plastics may deform during clamping, however.
CNC milling produces precise pockets, threaded holes, slots, and curved surfaces from these materials. ISO 2768 guidance helps define general tolerances when detailed drawings omit them, but it cannot replace functional testing. A thin aluminum wall may look accurate yet vibrate during assembly. That is a practical lesson.
Design engineers should review tool access, corner radii, chip removal, and grain direction before machining. Data from the 2023 World Manufacturing Forum report emphasizes digital, flexible production, but automation does not remove material judgment. Human review still matters.
Why Choose CNC Milling for Precision Manufacturing?
CNC milling delivers repeatable accuracy, but quality depends on more than machine resolution. A 2024 global smart-manufacturing survey of 600 executives reported that 86% viewed digital production as vital for competitiveness. That value appears only when process controls are disciplined. Experienced machinists check material hardness, fixture stability, tool geometry, and spindle condition before cutting. Small errors accumulate. A weak fixture can leave chatter marks across an otherwise accurate aluminum housing.
Cutting speed, feed rate, step-over, and coolant flow directly influence surface finish and tool life. Excessive heat may soften the cutting edge and shift dimensions during long cycles. Even a modest spindle temperature rise can affect bore accuracy. Tool wear monitoring helps, but it is not perfect. A worn insert may still produce acceptable parts before failing inspection. That uncertain stage deserves attention. Many quality teams use process capability targets such as Cpk 1.33, supported by measurement practices aligned with ISO 230-2 and calibrated inspection equipment.
Quality also depends on measurement timing. Checking a warm part immediately after machining can create misleading results. Operators should control temperature, clean datum surfaces, and record inspection data beside tool-life information. The 2023 Manufacturing Quality Benchmark Report found that manufacturers using real-time process data reduced unplanned downtime by 18%. Yet data alone cannot correct poor setup decisions. A practical review still asks whether the cutter was suitable, the fixture was rigid, and the program matched the actual material batch.
CNC milling is valuable when a part needs accurate features, repeatable dimensions, and a clean surface. A rotating cutter removes material from aluminum, steel, plastics, or other machinable stock. In a typical workshop, machinists use digital models, calibrated tools, and inspection equipment to control holes, pockets, slots, and angled faces. Proper fixturing matters greatly. Even a precise machine can produce errors when the workpiece shifts.
Compared with CNC turning, milling handles complex prismatic shapes better, while turning suits round components such as shafts and bushings. Additive manufacturing creates intricate internal forms with less waste, but it may need post-processing and can show layered surfaces. Laser cutting is fast for flat profiles, yet it cannot easily create deep pockets or three-dimensional contours. Electrical discharge machining can achieve fine details in hard materials, though it is usually slower and more specialized. CNC milling is not always the best answer. I have seen simple plates become unnecessarily expensive because milling was chosen without considering sheet fabrication.
Tips: Define critical tolerances before requesting a quote. Separate functional dimensions from cosmetic preferences. Choose cutters that match corner radii and material hardness. Leave enough stock for finishing passes. Check burrs, tool marks, and hole locations after machining. A useful drawing should state datums, units, surface requirements, and inspection points. Small details prevent large revisions. Still, every design deserves review; assumed tolerances can quietly increase cost, and experienced engineers can overlook them too.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru