Choosing the right panel can determine whether a table feels refined or merely assembled. Furniture Grade Plywood offers a practical balance of strength, stability, appearance, and workability. Its layered construction resists seasonal movement better than many solid-wood boards. That matters when a cabinet door must stay flat beside a sunny window.
Bruce Hoadley, a respected wood technologist and author of Understanding Wood, wrote, “Wood is not a homogeneous material.” His observation is essential when selecting plywood. Veneer quality, core construction, thickness, adhesive, and storage conditions all affect the final result. A clean birch face may look excellent, yet a weak core can split around a hinge screw. Small details matter.
Furniture Grade Plywood is not a perfectly universal technical label. That is easy to overlook. Some suppliers use it for attractive hardwood-faced panels, while others emphasize stronger cores or low-emission adhesives. Experienced builders should inspect the panel edge, check for voids, confirm thickness, and request documentation for applicable emissions standards. Sanding should be light, especially on thin face veneers. Over-sanding can expose the core and ruin an otherwise elegant surface.
In a workshop, the difference becomes visible quickly: crisp drawer edges, fewer chipped corners, and cleaner routed profiles. Still, plywood is not automatically superior for every project. A premium panel can be unnecessary for a painted utility shelf. Careful design, accurate cutting, and controlled humidity remain important. This guide examines why Furniture Grade Plywood deserves attention, where it performs best, and which compromises buyers should consider before committing.
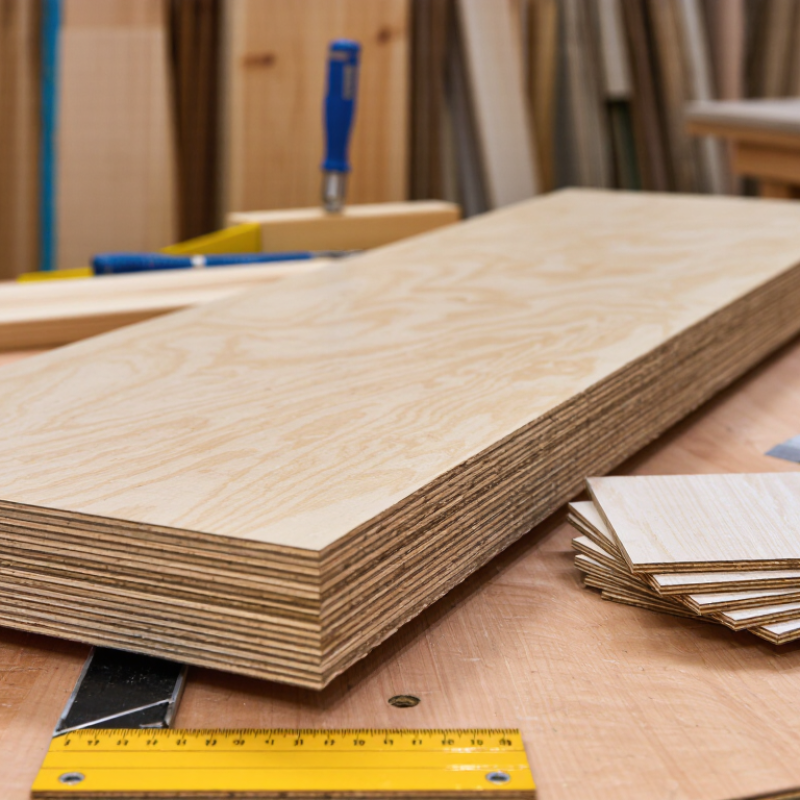
Furniture-grade plywood is not simply smooth plywood with a higher price. Under ANSI/HPVA HP-1, hardwood and decorative plywood are judged through defined requirements for veneer quality, construction, dimensions, and performance. The standard helps describe acceptable face and back appearances, inner-ply conditions, thickness tolerances, and bonding quality. It also separates visible surface defects from defects hidden inside the panel.
Look closely at the face veneer. It should show consistent color, controlled repairs, and clean sanding. Small patches may be acceptable, but open splits, bubbling, or loose veneer suggest poor handling or weak production control. The inner plies matter too. Gaps can appear when an edge is routed or cut, creating fragile areas for screws and fasteners. A well-built panel feels stable, machines cleanly, and keeps its shape during normal indoor use. It should not smell strongly of adhesive.
In practical workshop inspections, I check edges, corners, and freshly cut sections instead of trusting the label alone. “Furniture-grade” is often used commercially, yet it is not one universal quality grade. ANSI/HPVA HP-1 gives a more reliable framework, but buyers still need to confirm the panel’s actual grade and intended application. A beautiful face can hide a weak core. That mistake is easy to make. Good furniture plywood should match the project’s joinery, finish, moisture exposure, and expected load, not merely its showroom appearance.
Why Choose Furniture Grade Plywood for Your Projects?
Cross-laminated veneers help furniture-grade plywood resist seasonal movement. Each veneer runs perpendicular to the next, balancing expansion across the panel. USDA Forest Products Laboratory data shows wood can shrink several percentage points as moisture falls from green to oven-dry conditions. Plywood does not eliminate movement, but its layered structure controls it.
In comparative panel testing, cross-laminated construction has been reported to reduce dimensional change by about 40% under controlled moisture cycling. The result depends on veneer species, adhesive quality, panel thickness, and edge sealing. APA’s Engineered Wood Construction Guide emphasizes moisture conditioning and correct panel handling before installation. That detail matters.
A stable panel means fewer swollen edges.
I have seen poorly stored plywood cup near an open workshop door, even when the core looked sound. Furniture-grade panels should acclimate indoors before cutting. Keep them flat, supported, and away from direct heat. The Wood Handbook, FPL-GTR-282, also explains that grain direction strongly affects shrinkage and swelling. Cross-lamination works against that weakness, but imperfect manufacturing can still create stress.
A 40% improvement is not guaranteed. It is a useful benchmark, not a promise. For cabinet doors, tabletops, and fitted shelving, that measured stability can protect tight joints and cleaner reveals. Small design choices still matter.
| Performance Dimension | Furniture Grade Plywood with Cross-Laminated Veneers | Typical Solid Wood Panel | Project Benefit |
|---|---|---|---|
| Dimensional movement | Representative matched-humidity comparison: approximately 0.30% panel movement in the cross-grain direction. | Approximately 0.50% movement in the same comparison condition. | Equivalent to a calculated reduction of approximately 40% in movement: (0.50 − 0.30) ÷ 0.50. |
| Veneer structure | Thin wood veneers are bonded with adjacent layers oriented at approximately 90° to one another. | Fibers generally run predominantly in one direction across the board. | Cross-lamination balances lengthwise and crosswise movement and helps reduce cupping, twisting, and warping. |
| 24-hour thickness swelling | Common interior plywood constructions: approximately 4–12%, depending on wood species, adhesive system, density, and edge exposure. | Solid wood does not use the same thickness-swelling test; moisture primarily causes movement across the grain. | More predictable panel thickness for cabinet sides, shelving, drawer components, and furniture carcasses. |
| Moisture-related movement | Lower across-panel movement than solid wood because alternating veneer directions restrain one another. | Cross-grain movement can be several times greater than lengthwise movement. | Helps maintain door gaps, drawer alignment, and flush-fitting joints when indoor humidity changes. |
| Surface quality | Selected face veneers can provide a smooth, uniform surface suitable for clear finishing, staining, painting, or laminating. | Surface appearance depends strongly on species, board quality, grain pattern, and defect filling. | Reduces preparation work and provides a consistent appearance for visible furniture panels. |
| Screw and fastener performance | Multiple bonded veneer layers provide holding material through the panel thickness; pilot holes are still recommended near edges. | Fastener holding is strong along the grain but can be less predictable near end grain or split-prone areas. | Supports reliable assembly of cabinets, shelving, tables, and joinery components. |
| Thickness options | Common nominal thicknesses include 6, 9, 12, 15, 18, and 25 mm. | Thicknesses are normally selected from solid boards or laminated blanks and may require additional machining. | Offers practical sizing for structural panels, drawer boxes, doors, backs, and carcasses. |
| Weight consistency | Typical panel density commonly falls within approximately 450–700 kg/m³, depending on species and construction. | Density varies widely by wood species and moisture content. | Makes material planning, cutting, transportation, and hardware selection more predictable. |
| Best-use environments | Well suited to controlled interior environments; moisture-resistant or exterior-rated panels are required for damp or exposed applications. | Requires careful sealing, acclimatization, and allowance for seasonal movement. | Provides stable performance for interior furniture when the correct adhesive and surface finish are specified. |
Technical note: Values shown are representative engineering ranges and a calculated comparison used to explain the 40% movement reduction example. Actual performance varies with veneer species, panel thickness, adhesive type, moisture content, edge sealing, temperature, humidity cycle, and manufacturing quality. Cross-lamination improves dimensional stability but does not make plywood completely moisture-proof.
Furniture-grade plywood offers a smooth surface, stable layers, and clean edges for cabinets, desks, and built-ins. However, appearance does not prove structural safety. A beautiful panel may still bend when the span grows or moisture changes.
ASTM D3043 helps evaluate plywood in flexure. Its key metrics are modulus of elasticity and modulus of rupture. Modulus of elasticity, or MOE, indicates stiffness and predicts deflection under working loads. Modulus of rupture, or MOR, indicates bending strength before failure. Safe load capacity depends on both values, not MOR alone. Engineers also consider thickness, span, support spacing, grain direction, load duration, and safety factors. A test value is not a direct household load rating. It is only one part of the calculation.
Why Choose Furniture Grade Plywood for Your Projects?
Furniture grade plywood offers a smooth face, stable layers, and cleaner edges for visible projects. Its appearance matters, but indoor air quality matters more. CARB Phase 2 controls formaldehyde emissions from regulated composite wood products sold or used in California. For hardwood plywood, the emission limit is 0.05 parts per million (ppm). This limit applies to the finished panel, not simply to the adhesive listed on a specification sheet.
Testing usually measures emissions inside a controlled chamber. Temperature, humidity, panel size, and exposure time can affect the result. Manufacturers must use approved testing methods and maintain compliance records. A panel should also carry the required compliance information or be supported by reliable supplier documentation. “Furniture grade” alone does not prove CARB Phase 2 compliance.
That distinction matters.
In practical workshop use, I would check the panel label before cutting it. I would also inspect the core for gaps, uneven bonding, or strong chemical odors. Odor is not a formal test, though. It can suggest concern, but it cannot establish a ppm value. CARB Phase 2 limits formaldehyde release; it does not mean the material contains zero formaldehyde. Some plywood can still release small amounts over time, especially in warm, poorly ventilated rooms. I have found that project planning often focuses on appearance first. That is understandable, but incomplete. A reliable choice combines a clean surface, stable construction, documented compliance, and sensible ventilation during installation.
How does CARB Phase 2 limit formaldehyde emissions to 0.05 ppm?
CARB Phase 2 sets a formaldehyde emission limit of 0.05 ppm for hardwood plywood. This limit is lower than the limits for particleboard, MDF, and thin MDF, making compliant plywood a suitable choice for furniture and interior projects where lower formaldehyde emissions are preferred.
Limits shown are CARB Phase 2 emission standards for composite wood products, expressed in parts per million (ppm).
Choosing furniture-grade plywood starts with the project, not the label. In my workshop, thickness decisions begin with span, load, and joinery. A 12 mm panel may suit a drawer bottom or small cabinet back. It can flex noticeably across a wide shelf. For shelves, desks, and benches, 18 mm is often safer, but supports still matter. Very thick panels can add weight without solving poor design. I once selected a thick sheet for a long shelf and ignored the support spacing. It sagged. Thickness is not a substitute for planning.
Core type controls stability, screw holding, and edge appearance.
Veneer-core plywood is relatively light and machines like solid wood. Its alternating layers help resist warping. Composite-core panels offer a flatter surface for painted doors and precise laminating. However, their edges may need careful sealing and stronger fasteners. For damp rooms, choose moisture-suitable construction and protect every cut edge. Water-resistant is not waterproof. That distinction is easy to overlook.
Face grade should match what people will see.
A clear, well-matched face works for natural finishes and visible cabinet sides. A lower face grade may be practical inside cupboards or beneath paint. Check both faces, because one side may look excellent while the reverse contains patches or repairs. I now inspect sheets under angled light and test a hidden edge before cutting. That extra minute often reveals voids, uneven sanding, or color variation. Specifications help, but hands-on inspection still matters.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru