Why Choose Metal Snaps for Global Sourcing?
Global apparel sourcing often depends on details that buyers notice only after failure. Metal Snaps are one of those details. They must open smoothly, close firmly, and remain attractive after repeated washing. A weak cap can damage fabric. A poor finish can leave dark marks on a pale jacket.
David S. Birnbaum, a longtime apparel sourcing consultant, offers a useful principle: “The smallest component can determine the value of the finished garment.” This idea fits Metal Snaps closely. Their performance depends on alloy quality, spring tension, plating thickness, and installation pressure. A sourcing team should request production samples, not only showroom samples. Test pieces can reveal loose rings, uneven color, sharp edges, or inconsistent closure force. Small defects matter.
Global purchasing also brings practical challenges. Buyers must compare minimum order quantities, tooling charges, packaging standards, and delivery schedules. They should review factory records and confirm material specifications. Salt-spray testing may help assess corrosion resistance. Pull testing can show whether a snap will survive real use. Carton labels and batch numbers improve traceability across long supply chains.
Still, no checklist guarantees a perfect result. A polished sample can mislead. Even experienced teams sometimes overlook fabric thickness or washing conditions. That is worth admitting. The better approach combines supplier experience, documented testing, and honest review. When these steps work together, Metal Snaps become more than decorative hardware. They support durability, product consistency, and buyer confidence in international sourcing.
Why Choose Metal Snaps for Global Sourcing?
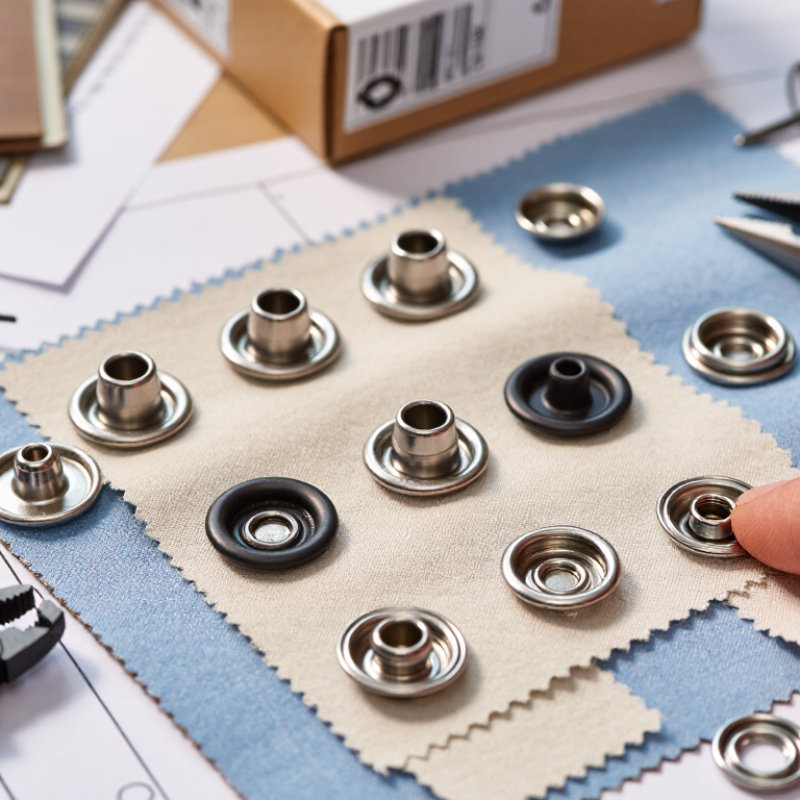
Metal snaps are four-part fasteners: a cap, socket, stud, and open ring. Together, they create a compact closure for jackets, workwear, bags, tents, and equipment covers. The socket receives the stud, while the ring locks the assembly through fabric or webbing. Four parts. One action.
A sourcing review should check more than appearance. Suppliers need consistent dimensions, clean forming, secure plating, and documented pull-off and corrosion tests. In production, a snap may fail because the ring cuts fabric, not because the metal breaks. Fit matters. Sampling should include repeated opening cycles, washing, humidity exposure, and installation with the intended fabric thickness. ASTM and ISO test methods can support comparable results, but test conditions must match real use.
Textile Exchange’s Materials Market Report 2024 recorded global fiber production at about 124 million tonnes in 2023, with projections approaching 160 million tonnes by 2030. That scale increases pressure to reduce replacement waste and improve component traceability. Metal snaps can support longer product use, but metal is not automatically sustainable. Buyers should request alloy details, coating information, recycled content evidence, and restricted-substance declarations. Global sourcing also needs clear tolerances and inspection records. A cheaper snap can become expensive after field returns. Sometimes, the overlooked ring causes the problem.

Metal snaps look simple, but their material affects durability, cost, and user experience. In global sourcing, the right choice depends on the product’s actual working conditions. During supplier reviews, I check the fabric weight, opening frequency, moisture exposure, and required finish. Small details matter. A heavy jacket needs stronger snap retention than a lightweight pouch.
Brass suits fashion garments, leather goods, and accessories needing a warm, classic appearance. It machines well and accepts decorative finishes. However, brass can develop color changes when exposed to sweat or humid storage. Stainless steel is a stronger option for outdoor clothing, workwear, bags, and products facing repeated washing. It offers good corrosion resistance and a clean surface. Yet, its higher hardness may increase tooling wear and unit cost. Zinc alloy supports complex shapes and attractive surface finishes. It works well for decorative snaps, medium-duty apparel, and cost-sensitive designs. Its performance depends heavily on the alloy grade and coating quality.
I once treated the lowest quotation as the best sourcing result. That decision ignored testing time and led to inconsistent snap engagement. Now, I request pull-force checks, salt-spray results, coating thickness records, and sample approval before bulk production. A supplier should also confirm dimensional tolerances and plating consistency. Laboratory data helps, but practical trials still matter. Install samples on the actual fabric. Wash them repeatedly. Inspect loosened caps, sharp edges, discoloration, and difficult opening force. No material wins every project.
| Material | Typical Density | Key Material Characteristics | Corrosion and Tarnish Behavior | Manufacturing Advantages | Best Use Cases for Snaps | Limitations to Consider | Global Sourcing Guidance |
|---|---|---|---|---|---|---|---|
| Brass | Approximately 8.4–8.7 g/cm³ | Copper-zinc alloy with good ductility, machinability, electrical conductivity, and a warm metallic appearance. | Generally good resistance to normal atmospheric exposure. It can tarnish or develop a patina over time, especially in humid or chemically active environments. | Suitable for stamping, forming, machining, and decorative plating. Its ductility supports smooth snap engagement and reliable forming. | Fashion apparel, leather goods, handbags, footwear, denim, decorative closures, and products where appearance and a premium metallic feel are important. | Heavier than zinc alloy and stainless steel in many comparable designs. Surface color may change if an uncoated finish is exposed to moisture, sweat, or chemicals. | Specify alloy grade, plating or lacquer system, surface-color tolerance, nickel-release requirements, and corrosion-test conditions before approval. |
| Stainless Steel | Approximately 7.7–8.0 g/cm³ | Iron-based alloy containing chromium; common austenitic grades provide high toughness, strong durability, and excellent resistance to wear. | Chromium forms a passive oxide layer that provides strong resistance to rust and staining. Performance depends on grade, surface condition, chloride exposure, and manufacturing quality. | Supports durable stamping, wire forming, machining, and polishing. It is well suited to long-service components exposed to frequent handling or washing. | Outdoor apparel, marine or coastal products, workwear, luggage, equipment covers, washable goods, and applications requiring high durability and low maintenance. | Usually more difficult to form and machine than brass or zinc alloy. Material and processing costs can be higher, and its appearance may be less decorative without additional finishing. | Confirm the exact grade, such as an austenitic grade suitable for the environment, along with salt-spray criteria, passivation requirements, burr control, and magnetic expectations. |
| Zinc Alloy | Approximately 6.6–6.7 g/cm³ | Die-cast alloy offering good dimensional repeatability, complex-shape capability, and a relatively low weight compared with brass and stainless steel. | Provides useful atmospheric corrosion resistance, but exposed surfaces can develop white corrosion products in prolonged humidity or salt exposure. Protective finishing is commonly used. | Highly suitable for die casting, enabling integrated decorative shapes, logos, recessed details, and large-volume production with consistent dimensions. | Decorative fashion snaps, accessories, bags, footwear, promotional products, and medium-duty closures where shape flexibility and cost efficiency are priorities. | Less suitable for severe impact, high-temperature service, or continuous saltwater exposure. Brittle failure and coating damage should be evaluated in heavy-duty designs. | Define casting porosity limits, plating thickness, adhesion testing, coating inspection, dimensional tolerances, and packaging protection against humidity during transport. |
| Brass | Approximately 8.4–8.7 g/cm³ | Strong visual compatibility with antique, vintage, gold-tone, and natural metal finishes. | Uncoated surfaces may darken or patinate; clear protective coatings can help maintain appearance but require adhesion and wear testing. | Well suited to embossed details, polished surfaces, and plated finishes when appearance consistency is carefully controlled. | Premium visual collections, heritage-style garments, luxury leather accessories, and products where the snap is a visible design element. | Finish variation can occur between production lots if base-metal preparation and plating controls are inconsistent. | Approve a physical color standard and define acceptable variation under the intended lighting conditions. |
| Stainless Steel | Approximately 7.7–8.0 g/cm³ | Strong, stable, and resistant to repeated opening and closing when the snap geometry and temper are properly designed. | Typically retains a clean appearance better than untreated brass or zinc alloy in humid and frequently handled applications. | Appropriate for high-cycle products where spring performance, wear resistance, and structural integrity are more important than decorative complexity. | High-use garments, technical textiles, outdoor equipment, reusable covers, and products exposed to repeated washing or abrasion. | Excessive work hardening, sharp edges, or unsuitable tooling can affect assembly quality and user comfort. | Validate opening force, closing force, cycle life, edge radius, and compatibility with the fabric or substrate thickness. |
| Zinc Alloy | Approximately 6.6–6.7 g/cm³ | Lower density and strong design freedom make it practical for larger decorative components that should not feel excessively heavy. | Long-term performance is strongly influenced by plating, paint, clear coating, storage humidity, and exposure to sweat or salt. | Efficient for complex three-dimensional shapes and repeat production when die-casting tooling is amortized over sufficient volume. | Large decorative snaps, statement accessories, fashion hardware, and cost-sensitive programs requiring detailed shapes. | Die-cast surfaces may contain porosity or require additional finishing. Thin plating or poor sealing can reduce service life. | Request first-article samples, coating cross-hatch tests, humidity testing, and dimensional inspection before mass production. |
Metal snaps offer reliable fastening, clean appearance, and efficient production across many garment categories. However, material selection must consider skin contact, not only strength or surface finish. Under REACH Annex XVII, certain articles intended for direct and prolonged skin contact must limit nickel release to 0.5 μg/cm² per week. This requirement applies to the released amount, not simply the nickel content inside the snap.
In practical sourcing reviews, a recurring mistake is trusting a general material certificate. A certificate is useful, but it is not a guarantee. Testing should reflect the finished snap, coating, plating, and assembly process. Surface wear matters. A polished snap can release more nickel after repeated opening, washing, or rubbing against skin. Ask suppliers for recent laboratory reports, test methods, sample identification, and production-batch traceability. Also confirm whether the product falls within the relevant REACH contact category.
Tips: Request samples before bulk approval. Test finished goods, not raw metal alone. Check edges, backs, and contact points. Keep documents with purchase records. If a supplier cannot explain the test conditions clearly, pause the order. That hesitation may prevent a costly correction later. Requirements can change, and interpretations may differ across markets, so a current legal review remains sensible.
For global sourcing, metal snaps need more than a polished appearance. A controlled sampling plan gives buyers measurable evidence. ISO 2859-1 connects lot size, inspection level, and sample size. Many buyers use General Inspection Level II, but the purchase agreement should state it clearly. AQL 1.5 can guide acceptance for agreed nonconformities. It does not guarantee that every shipment contains only 1.5% defects.
Define the lot before sampling. Keep one production run, finish, and size together. Keep lots separate. Select units randomly from different cartons, not only from top layers. Inspectors can check snap alignment, cap scratches, plating coverage, burrs, and opening force. Record everything. Major defects may include loose attachment or failed closure. Minor defects can include light color variation, when appearance requirements allow it.
The acceptance number depends on lot size and code letter. That detail is often missed. A written plan should specify normal inspection, single sampling, and AQL values for each defect class. Retain sample photos, measurements, and signed reports for supplier discussions. No inspection plan is perfect. A small sample can miss clustered defects, especially when cartons are packed unevenly. Review trends across shipments and investigate repeated failures instead of trusting one pass result. This approach makes sourcing decisions more consistent and easier to verify.
This example applies ISO 2859-1, General Inspection Level II, normal single sampling, at AQL 1.5. As lot size increases, the required sample size and the maximum number of nonconforming snaps allowed for acceptance also increase. The exact sampling plan depends on the selected inspection level, lot size, and standard tables.
Metal snaps suit global sourcing when buyers need repeatable fastening, clean appearance, and strong cycle performance. Yet the lowest unit price can mislead. A small order may carry a high MOQ, while custom molds add upfront tooling fees. For example, a 10,000-piece run can distribute a mold cost better than a 2,000-piece trial. Standard sizes usually reduce this burden. Finish still matters.
Lead time includes more than factory production. Sampling, tool approval, plating, inspection, and export preparation can each add days. In practical sourcing, I request dimensional samples and test the snap on the actual fabric. A thin jacket panel may need less force than heavy canvas. That detail affects rejection rates. Fast production is not useful if the first shipment fails assembly checks.
Landed cost should include unit price, tooling, packaging, freight, insurance, duties, inspection, and potential rework. A cheaper snap can become expensive after air freight or uneven plating causes returns. I also compare supplier quotes using the same specifications, including metal thickness, finish, tolerance, and carton quantity. My own estimates are not always accurate; freight changes and small defects can disrupt the model. Keep a contingency instead of trusting a perfect spreadsheet.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







