Why Is Carbon fiber production line cost So High?
Carbon fiber production line cost often surprises investors. A factory may look like a long series of ovens, rollers, tanks, and control cabinets. Yet each section demands strict temperature, tension, and chemical control. A small variation can weaken thousands of meters of fiber.
Industry analyst Jeff Sloan explains the central problem clearly: “Carbon fiber is expensive because it is energy-intensive, labor-intensive, and capital-intensive.” His observation reflects the entire manufacturing chain. Precursor fiber must remain uniform. Stabilization ovens may operate continuously at carefully controlled temperatures. Carbonization then requires extreme heat, protective atmospheres, and reliable exhaust systems. These units consume substantial energy and cannot tolerate frequent interruptions.
Equipment is only part of the investment. Engineers must design fire protection, ventilation, wastewater treatment, quality laboratories, and automated inspection systems. Skilled operators also need months of training. Production losses can be severe. A single unstable process may create brittle fiber, inconsistent strength, or an entire rejected batch.
Scale matters greatly. Small lines often carry higher costs per kilogram because utilities, maintenance, and technical labor remain expensive. Large facilities spread these costs more efficiently, but they require much greater capital and stronger market demand.
The uncomfortable truth is this: estimates are often too optimistic. They may exclude commissioning delays, spare parts, factory upgrades, and working capital. Carbon fiber production line cost is therefore not simply an equipment price. It is the financial result of precision, energy use, process risk, and long-term reliability. A cheaper design may exist, but not without trade-offs.
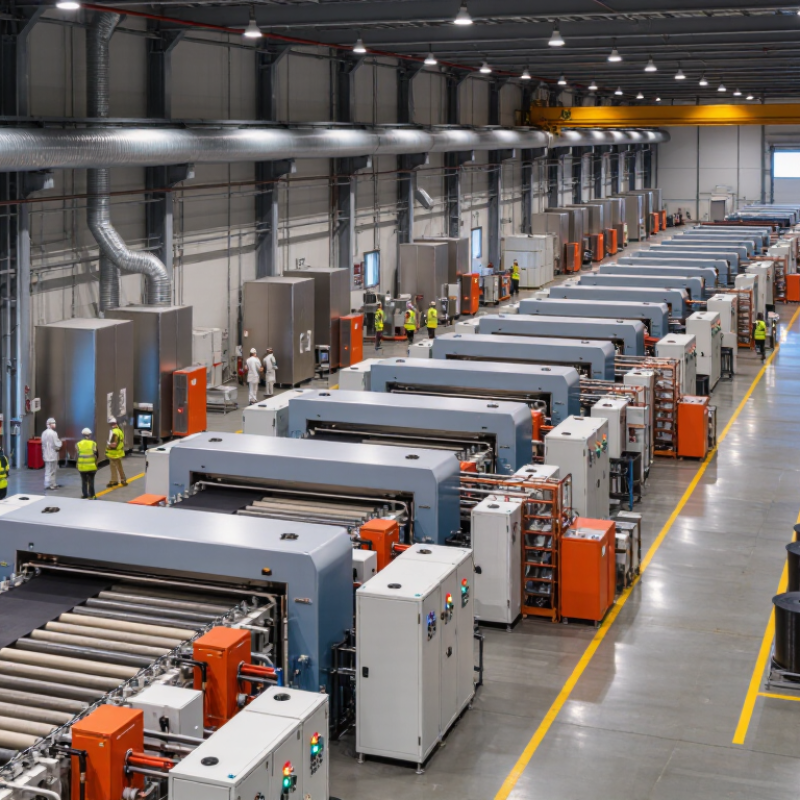
Carbon fiber production lines look expensive because they convert a fragile polymer into a high-performance structural material. The largest burden often begins before carbonization. PAN precursor commonly represents 50–60% of total carbon fiber cost. A U.S. Department of Energy cost model reported a similar share in its 2017 carbon fiber technology analysis. A 2022 review in Composites Part B also identified precursor production as a major cost driver. The percentage changes with product grade, plant scale, and energy prices.
PAN is not simply raw plastic. Its polymerization, filtration, spinning, washing, drying, and winding require tight process control. Each filament must maintain consistent diameter and molecular orientation. Small defects can reduce final tensile performance. That risk increases inspection, maintenance, and material losses. Stabilization also requires long heating cycles in controlled air. It is energy intensive. The carbonization furnace comes later, but its cost is easier to notice than precursor preparation.
The 50–60% figure deserves careful interpretation. It is a cost-model estimate, not a universal factory rule. A new line may pay more for qualified PAN, laboratory testing, and low production yields. A mature facility can reduce losses through process data and continuous quality checks. Still, precursor chemistry remains difficult to optimize. Lower purchase prices may create more broken filaments or unstable conversion. That trade-off is often missed in simple equipment quotations. My view is imperfect: precursor share should be calculated from actual plant data, not copied blindly from an industry average.

Why Is Carbon Fiber Production Line Cost So High?
Stabilization is the quiet cost center in carbon fiber manufacturing. PAN precursor passes through heated ovens at 200–300°C before carbonization. Oxygen reacts with the polymer and forms a stable ladder structure. Without this step, the fiber can melt or break during high-temperature treatment.
The process demands controlled airflow, tension, and residence time. A small temperature variation can create uneven color, strength, or shrinkage. Industrial lines may hold fiber for 30–120 minutes, depending on precursor chemistry and line speed. That long oven length requires major capital, insulation, ventilation, and continuous energy use. Lifecycle studies cited by the U.S. Department of Energy estimate carbon fiber production at roughly 183–286 MJ per kilogram. The exact number remains plant-specific. That uncertainty deserves attention.
Tips: Measure temperature across the fiber width, not only at the oven wall. Review oxygen levels at each zone. Keep detailed records of breaks, tension changes, and energy consumption. Oak Ridge National Laboratory reports that process optimization and alternative precursors can substantially reduce energy demand, but laboratory gains do not always transfer smoothly to full-scale lines. Real production is messier.
Carbon fiber production requires tightly controlled thermal stages. PAN-based precursor fibers are commonly stabilized in air at approximately 200–300°C before carbonization at about 1,000–1,500°C. Stabilization is especially important because slow, uniform heating allows cyclization and oxidation to occur without excessive fiber damage, increasing residence time, energy consumption, and equipment requirements.
Carbonization is where cost becomes visible. PAN-based fibers enter furnaces at roughly 1,000–1,500°C, under carefully controlled inert gas. The furnace must heat the fiber, insulation, rollers, gas, and internal fixtures. The fibers are light. The equipment is not.
An Oak Ridge National Laboratory life-cycle assessment estimated 183–286 MJ of primary energy per kilogram of carbon fiber. Results varied with precursor quality, furnace design, and process assumptions (Das, ORNL, 2011).
That range is substantial. A modern line also needs energy for gas circulation, exhaust treatment, cooling, and continuous temperature control. At 1,200°C, even small openings can release intense radiant heat. The furnace never sleeps.
The International Energy Agency’s Energy Technology Perspectives 2023 identifies industrial process heat as a major source of energy demand. Carbonization fits that difficult category. Long heating zones must remain stable while the line moves constantly. Heat recovery can reduce losses, but it adds exchangers, controls, and maintenance.
This is where estimates become imperfect. The 183–286 MJ figure is not a universal electricity bill. Local energy prices, production speed, furnace loading, and downtime can change the final cost sharply. A half-empty furnace may consume nearly the same heat as a full one. That detail is often underestimated.
Carbon fiber production becomes expensive when stabilized fiber enters graphitization. This stage exposes the material to temperatures between 2,000 and 3,000°C. The furnace must maintain even heat across a long, moving fiber path. Small temperature differences can change strength, modulus, or surface quality.
The equipment needs more than a heating chamber. Engineers must combine graphite components, thermal insulation, inert gas control, tension systems, and continuous cooling. At extreme temperatures, ordinary metals may deform or fail. Graphite parts can also wear faster when oxygen enters the chamber. Sensors, seals, power supplies, and exhaust systems add further costs. Electricity demand is substantial, especially during long production runs.
A practical cost review should examine output, not only purchase price. A larger furnace may increase capacity, but it also requires stronger power infrastructure and more complex maintenance. Energy losses through insulation can quietly affect operating expenses. Some early estimates look convincing, yet they underestimate commissioning time or replacement parts. That is a common weakness.
Reliable planning uses pilot data, thermal simulations, and measured gas consumption. Engineers should also check fiber tension at line speed. A stable process needs disciplined control. Cheap equipment is not always economical.
Carbon fiber production starts with polyacrylonitrile, or PAN, but PAN is not converted into fiber at full mass. Technical studies from the U.S. Department of Energy and Oak Ridge National Laboratory commonly report a PAN-to-carbon-fiber yield near 45–55%. Therefore, producing one kilogram of carbon fiber may require about 1.8–2.2 kilograms of PAN.
The missing mass leaves during stabilization and carbonization. Stabilization typically occurs around 200–300°C, while carbonization can exceed 1,000°C. These stages remove hydrogen, nitrogen, oxygen, water, and other volatile compounds. The fiber also loses mass through surface treatment, trimming, broken filaments, and rejected material. Yield is unforgiving.
Energy use adds another cost layer. Industry assessments, including data discussed in JEC technical reports, identify stabilization as a major production bottleneck because fibers must remain under controlled heat for extended periods. Carbonization requires high temperatures, inert atmospheres, and precise tension control. A small temperature variation can damage thousands of continuous filaments. Production lines therefore need furnaces, gas systems, tension controls, inspection equipment, and costly maintenance. The 1.8–2.2 kilogram ratio is not universal; precursor chemistry and line efficiency can shift it considerably. That uncertainty is often underestimated. In practice, every kilogram lost through poor alignment, overheating, or contamination raises the effective material cost.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







