A press operator reaches toward a jammed conveyor. The motor is off, but stored energy can still move a belt, release pressure, or restart equipment. Safety Lockout addresses that hidden danger by isolating hazardous energy before maintenance begins. It is not just a padlock on a switch. It is a controlled process: identify energy sources, shut equipment down, apply personal locks and tags, release or restrain stored energy, and verify isolation.
Former OSHA administrator Dr. David Michaels has emphasized the importance of preventing workplace injuries through effective safety systems. A practical paraphrase of that principle is: “A machine is not safe just because its controls are off.” This is not a direct quotation. The distinction matters, because workers need clear procedures—not slogans. A qualified safety professional should assess each machine, its energy sources, and the steps required for safe servicing.
Good Safety Lockout procedures make responsibility visible. Each authorized worker applies their own lock, checks the isolation, and removes that lock only when their work is complete. A supervisor’s checklist may help, but it cannot replace hands-on verification. Small details matter: a mislabeled valve, a shared power source, or pressure trapped in a line can undermine the whole process. Lockout takes time. That can feel inconvenient during a production rush. Still, teams should review procedures regularly and investigate near misses without blame. The process may be imperfect; noticing gaps is part of making it safer.
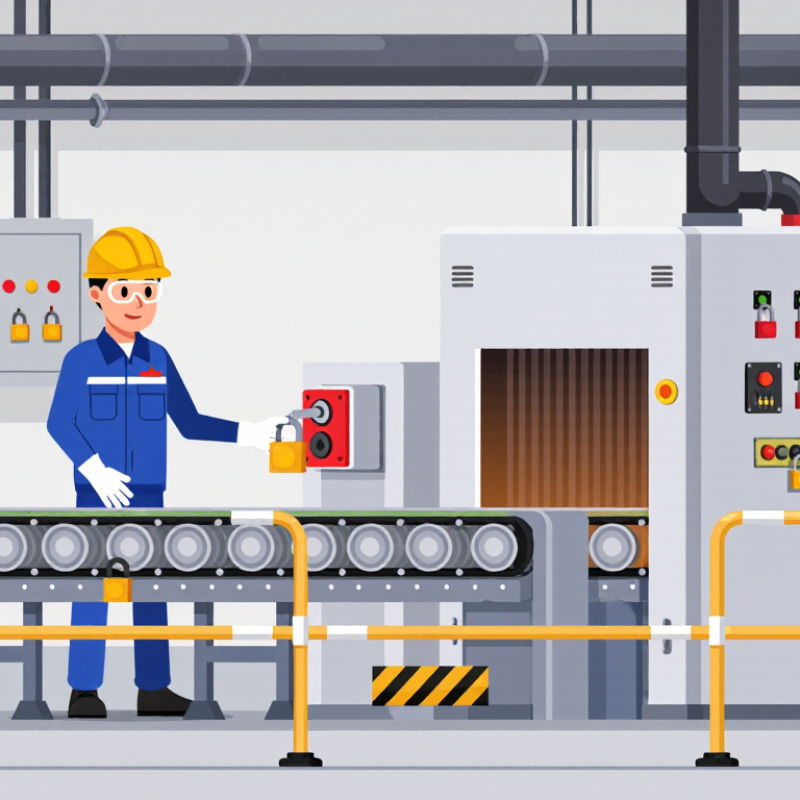
Safety lockout is a controlled way to keep hazardous energy from reaching equipment during servicing or repair. Energy may be electrical, hydraulic, pneumatic, thermal, or stored in a raised machine part. A worker isolates the relevant sources and applies a personal lock so the equipment cannot be restarted unexpectedly. A tag communicates the danger, but it does not physically stop energy. The distinction matters.
Lockout is not just a padlock on a switch. Workers need to follow the equipment-specific procedure, account for stored energy, and verify isolation before work begins. For example, a conveyor may have a disconnected supply but still contain tension or a moving part that can fall. Verification should use suitable methods and be performed by trained, authorized workers. Details can be easy to miss, especially when equipment has been modified. A procedure deserves review when the real setup no longer matches it.
Tips: Identify every energy source. Tell affected coworkers before shutdown. Apply your own lock. Release or secure stored energy, then verify the safe state. If anything seems unclear, pause and ask a qualified supervisor. It is tempting to hurry. Don’t.
A machine can look still while its hazards remain active. A conveyor may restart when a sensor detects movement, or a press may cycle after power returns. Lockout/tagout helps prevent these unexpected startups during cleaning, repairs, and other servicing. The danger is real. A stop button alone does not isolate energy.
Workers trained and authorized for the task follow the machine-specific procedure. They shut down the equipment, isolate every energy source, and apply personal locks and tags to the designated devices. This may include electrical power, compressed air, hydraulic pressure, or gravity-held parts. Stored energy must also be released, restrained, or otherwise made safe. A suspended component, for example, may need a mechanical block. Small details matter.
Before work begins, workers verify isolation using the procedure, such as testing the controls after checking that the area is clear. If the machine responds, they stop and reassess; a lock is not proof that every hazard has been controlled. Each worker should keep control of their own lock and remove it only under the site’s procedure. In a noisy shop, a tag can be hard to notice, and a rushed handover can create confusion. These steps can feel repetitive. That is worth reflecting on: routine is useful, but it should never replace careful verification.
How Lockout/Tagout Prevents Unexpected Equipment Startup
Lockout/Tagout isolates equipment from hazardous energy during servicing and maintenance, helping prevent unexpected startup and the release of stored energy. OSHA estimates that compliance with its hazardous-energy control standard prevents about 120 fatalities and 50,000 injuries annually. These are separate estimates, shown on the same scale.
Source: U.S. Occupational Safety and Health Administration (OSHA). Estimates are approximate.
Lockout procedures are needed whenever a worker could be exposed to hazardous energy while servicing equipment. The source may be obvious, like an electrical supply, or less visible, such as pressure trapped in a hydraulic line. Mechanical movement, compressed air, steam, hot surfaces, chemicals, and raised components can also cause harm. Gravity counts too. A suspended machine part can drop after power is disconnected.
Tasks that may require lockout include repairs, cleaning inside machinery, clearing jams, changing tools, and replacing parts. The key question is whether someone could reach a danger zone while energy remains available or stored. A control switch is not enough; another person might restart the machine, or stored pressure may remain. Verify isolation, release or secure stored energy, and test that equipment cannot operate before work begins.
Details matter. A conveyor might stop while its belt still holds tension, and a press may retain pressure after shutdown. Follow the equipment-specific procedure and workplace training, including steps for multiple energy sources. In practice, teams can rush familiar jobs. That is worth challenging. If the energy source or safe isolation point is unclear, pause and ask a qualified supervisor rather than guessing.
A jammed conveyor can look harmless until stored energy releases. A maintenance worker may reach past a guard to clear a blockage, while another person restarts the line. OSHA estimates that effective lockout/tagout (LOTO) prevents about 120 deaths and 50,000 injuries each year. These figures, cited in OSHA’s Control of Hazardous Energy guidance, show why isolation is more than paperwork. It can stop a motor, press, or pneumatic line from moving while someone is exposed.
The safeguards are practical: identify energy sources, shut equipment down, apply personal locks, and verify isolation before work begins. OSHA’s 29 CFR 1910.147 sets requirements for energy-control procedures, employee training, and periodic inspections.
A lock on a switch is not enough if pressure remains trapped in a line. Check the gauge. Test the controls. Try again if the result is uncertain. Small details matter. Workers and supervisors should review procedures when equipment or tasks change, because a familiar machine can still hold an unfamiliar hazard. Procedures can be clumsy, and real work does not always follow a neat script. That is a reason to improve them, not skip verification.
Employers apply lockout/tagout by identifying every energy source connected to a machine, not just its main switch. A maintenance plan should name the isolation points, required locks, and steps for releasing stored pressure or electrical charge. Workers receive role-specific training and use personal locks that remain under their control. A red tag alone does not stop moving parts. No shortcuts.
Before work begins, an authorized worker isolates the equipment, applies locks and tags, and tests the controls. A meter may confirm that electrical power is absent; a pressure gauge can reveal trapped air. The worker should also try the normal start control, then return it to off. Verification must match the hazard. If a reading seems uncertain, stop and investigate rather than assume the machine is safe.
Employers audit the program by observing real tasks, reviewing procedures, and speaking with workers who use them. Records can show who was trained and when procedures were checked, but paperwork cannot reveal every confusing step. A checklist may look complete while a valve location remains unclear. Auditors should compare written instructions with the equipment on the floor and record gaps, corrective actions, and follow-up dates. One overlooked energy source can change the whole job.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru