Wood Drying Equipment removes excess moisture from lumber, boards, and other wood products under controlled conditions. The goal is not simply to make wood feel dry. Moisture levels affect weight, strength, dimensions, and how a piece behaves during storage or further processing. Moisture matters.
A kiln or industrial dryer uses heat and airflow to move moisture from the wood’s interior toward its surface. Operators monitor temperature, humidity, airflow, and moisture content, adjusting the drying schedule for the species, thickness, and intended use. A thick oak plank usually needs a different approach from a thin pine board. Drying too quickly can cause checking, warping, or internal stress; drying too slowly can waste time and energy. Results depend on more than the machine.
This article explains what Wood Drying Equipment is used for, how common systems work, and where they fit in wood processing. It also looks at practical considerations such as capacity, energy use, control systems, and routine maintenance. Buyers should compare equipment against their actual production needs, not just its advertised output. That can be harder than it sounds. Even a well-designed dryer cannot compensate for poor stacking, inconsistent material, or careless monitoring. Reliable results come from suitable equipment and informed operation, though some facilities still need trial runs to refine their schedules.
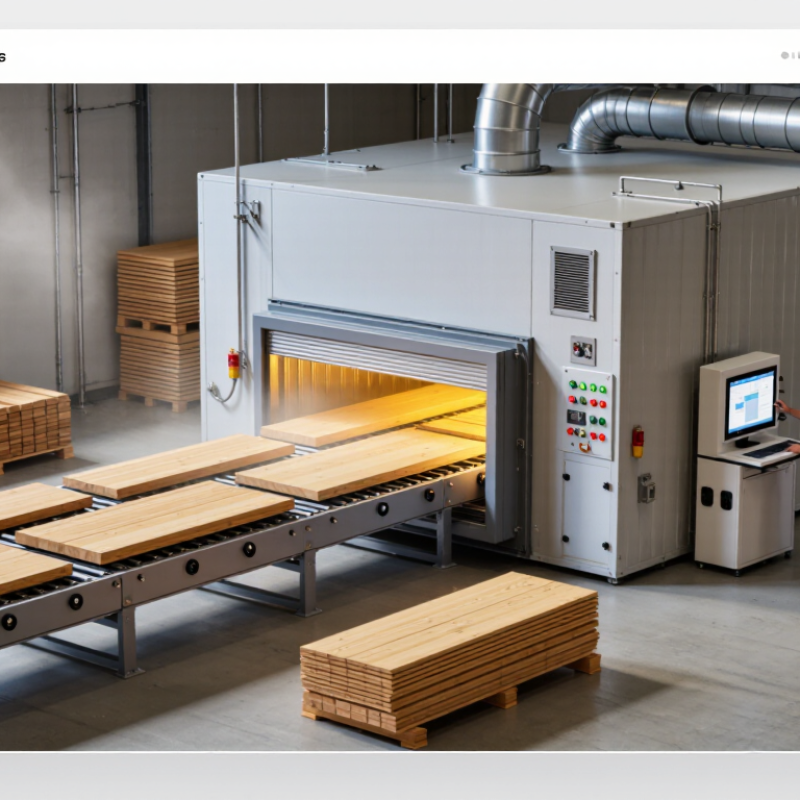
Wood drying equipment removes excess moisture from freshly cut lumber before it is used in furniture, flooring, cabinets, or construction. It includes kilns, fans, heaters, vents, and moisture sensors. Together, these components control heat, airflow, and humidity so boards dry more evenly. A kiln is not simply a hot room. Poor airflow can leave the board surface dry while its center stays wet, causing cracks or later movement.
Wood drying equipment removes moisture by controlling heat, airflow, and humidity around freshly cut lumber. In a kiln, warm air passes over stacked boards while fans keep conditions more even. Heat encourages water inside the wood to move toward the surface, where circulating air carries it away. The process is gradual. Drying too quickly can cause cracks, warped boards, or a dry outer layer around a wetter core.
Operators adjust temperature and humidity in stages to match the wood species, thickness, and starting moisture level. Sensors help track conditions, but readings need careful interpretation; one measurement may not represent every board in a stack. Small sample pieces can be weighed and checked with a moisture meter to follow changes over time. Airflow also matters. Spacers between boards create channels, while blocked gaps may leave damp spots.
Near the target moisture content, equipment can hold the lumber in an equalization stage so boards become more consistent. This can reduce problems during later machining or storage. Still, drying is not perfectly uniform. A board’s position and grain can change how it responds, so occasional checks remain useful. Dry air alone is not enough.
| Equipment or Method | How It Removes Moisture | Typical Use | Common Moisture-Content Goal | Key Operating Considerations |
|---|---|---|---|---|
| Conventional kiln | Circulates heated air through stacked lumber. Heat encourages moisture to move from the wood’s interior to its surface, while ventilation carries water vapor out of the kiln. | Commercially drying sawn lumber for furniture, flooring, construction, and woodworking. | Often about 6–12% for indoor uses; targets vary by product and local conditions. | Temperature, relative humidity, airflow, and drying time are adjusted to limit checking, warping, and other defects. |
| Dehumidification kiln | Uses a heat-pump system to cool humid air and condense water from it. The recovered heat warms the circulating air, which continues drying the lumber. | Small and medium-scale operations, specialty lumber, and lower-temperature drying schedules. | Commonly about 6–12% for many interior applications. | Moisture removal depends on air circulation, load arrangement, and the kiln’s ability to manage condensate and humidity. |
| Solar kiln | Uses solar energy to warm air inside an enclosure. Vents release moisture-laden air, and fans may help circulate air through the lumber stack. | Small-scale drying where lower equipment complexity and use of solar heat are priorities. | Can reach roughly 10–20%, depending on climate, design, season, and schedule. | Drying is weather-dependent; airflow and venting help prevent excessive humidity and uneven drying. |
| Vacuum kiln | Reduces pressure around the lumber, allowing moisture to evaporate at a lower temperature. Heat is supplied to the wood, often through plates or circulating media. | Thick, valuable, or difficult-to-dry lumber where shorter drying times or lower drying temperatures may be useful. | Set according to the intended end use; targets commonly fall within the range used for other kiln-dried lumber. | Requires a sealed chamber and controlled pressure, heat, and drying cycles; performance depends on wood species and dimensions. |
| Air-drying yard and fans | Natural or fan-assisted airflow carries water vapor away from board surfaces as moisture gradually migrates out of the wood. | Pre-drying lumber before kiln drying, or drying stock where longer drying times are acceptable. | Often approaches approximately 15–25%, depending on climate and exposure; it may not reach indoor-use targets. | Stack spacing, stickers, rain protection, ground clearance, and airflow influence uniformity and drying time. |
| Moisture monitoring equipment | Pin-type meters measure electrical resistance between pins; pinless meters estimate moisture using electromagnetic readings. These devices monitor drying progress rather than remove moisture directly. | Checking lumber during drying and verifying whether it is near its target moisture content. | Readings are compared with the project’s specified target, with adjustments for species and temperature where applicable. | Meter readings are estimates and can be affected by species, temperature, grain direction, and measurement depth. |
| Moisture-content targets and drying times vary with wood species, board thickness, starting moisture content, end use, and local conditions. Moisture content is commonly expressed as a percentage of the oven-dry weight of the wood. | ||||
Wood drying equipment removes excess moisture before lumber becomes furniture, flooring, or structural material. Moisture control limits warping, cracking, staining, and later shrinkage. The USDA Forest Products Laboratory’s Wood Handbook states that interior wood commonly reaches 6–8% moisture content, while structural lumber is often dried to about 19%. These targets depend on climate, species, thickness, and end use.
The main types begin with conventional hot-air kilns. They use heated air, fans, and vents, making them suitable for large, regular production. Dehumidification kilns recycle heat and condense moisture, often reducing exhaust losses. Solar kilns use collectors and natural energy, but cloudy weather can slow schedules sharply. Vacuum kilns lower air pressure, helping thick or valuable boards dry faster at lower temperatures. Radio-frequency vacuum systems heat moisture inside the wood, offering speed and improved control, although installation and maintenance costs remain high.
The Wood Handbook warns that drying rate changes with airflow, board thickness, initial moisture, and wood structure. Sensors help, but they do not remove judgment. A display showing 8% does not prove every board is ready. Operators should sample several locations and inspect the core, not only the surface. Conventional kilns remain dependable, yet they may consume substantial heat. Dehumidification systems can be more efficient, but their slower cycles may frustrate high-volume operations. Solar drying appears simple. Real weather is not.
Wood drying equipment supports nearly every stage of wood processing. Kilns remove excess moisture before sawing, machining, gluing, and finishing. This control reduces warping, checking, mold risk, and later dimensional movement. The USDA Forest Products Laboratory’s Wood Handbook states that many interior applications target roughly 6–8% moisture content. However, the correct level depends on species, thickness, climate, and end use.
Drying also improves production consistency. Uniform boards move more predictably through planers, moulders, and CNC machines. Below the fiber saturation point, commonly near 30% moisture content for many species, wood begins shrinking significantly. Poorly controlled drying can create casehardening, honeycombing, or surface cracks. These defects may remain hidden until machining. That is an expensive lesson.
Tips: Measure moisture in several board locations, not just one surface. Use calibrated meters and record kiln temperature, humidity, and airflow. Follow a species-specific schedule, then allow equalization and conditioning. The Wood Handbook recommends conditioning practices that relieve drying stresses, but real workshops still need trial adjustments. Equipment settings are guides, not magic.
Modern drying systems can also recover heat, regulate airflow, and reduce unnecessary energy use. The European Commission’s Best Available Techniques reference documents identify heat recovery and process control as important efficiency measures in wood-based manufacturing. Yet faster is not always better. A rushed schedule may save hours while creating weeks of rework. Experienced operators inspect sample boards, compare core and shell moisture, and revise the process when results disagree with the readings.
How drying equipment supports wood processing by reducing moisture content
Drying equipment removes moisture from lumber to help prepare it for machining, finishing, and end use. This illustrative example shows moisture content falling from about 60% in freshly cut wood to around 8% after kiln drying. Actual values vary with species, thickness, and drying conditions.
What Is Wood Drying Equipment Used For?
Wood drying equipment removes excess moisture before lumber is used in construction, flooring, furniture, or engineered products. Controlled drying reduces cracking, warping, fungal growth, and later dimensional movement. The USDA Forest Products Laboratory’s Wood Handbook, FPL-GTR-282, notes that some green wood species can contain moisture exceeding 100% of their oven-dry weight. That difference strongly affects kiln capacity, drying time, and energy demand.
Factors That Influence Equipment Selection
Species and board thickness usually come first. Dense hardwoods need gentler schedules, while thin softwood boards may tolerate faster heating. Initial moisture content matters too. A kiln designed for 20% moisture content lumber may perform poorly with freshly sawn material above 60%. Target moisture content also depends on the end use. The Wood Handbook indicates indoor wood often reaches approximately 6–8% equilibrium moisture content under moderate indoor humidity.
Energy availability shapes the equipment decision. The U.S. Department of Energy’s Industrial Decarbonization Roadmap identifies process heating as a major industrial energy load. Therefore, operators should compare heat recovery, insulation, fan efficiency, and fuel stability, not only purchase price. Direct-fired systems may respond quickly, while steam or hot-water systems can offer steadier control. Electric heating may simplify emissions management, but operating costs can vary sharply.
Airflow deserves attention. Uneven circulation leaves wet pockets inside a seemingly dry stack. Sensors help, but sensors can drift. Regular calibration is essential. This is where selection becomes less tidy. A technically efficient kiln can still underperform when loading patterns, maintenance skills, or local climate are ignored.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru